

Working Principle and Features of Tote Bag Unloading Pneumatic Conveying Equipment
Tote bag unloading pneumatic conveying equipment is a specialized system designed to efficiently transfer bulk materials from large tote bags into processing facilities or storage areas. This equipment plays a crucial role in industries such as chemicals, food processing, and pharmaceuticals, where handling bulk materials safely and efficiently is paramount. The system combines advanced engineering with pneumatic technology to ensure seamless material transfer while maintaining product integrity and operational safety.

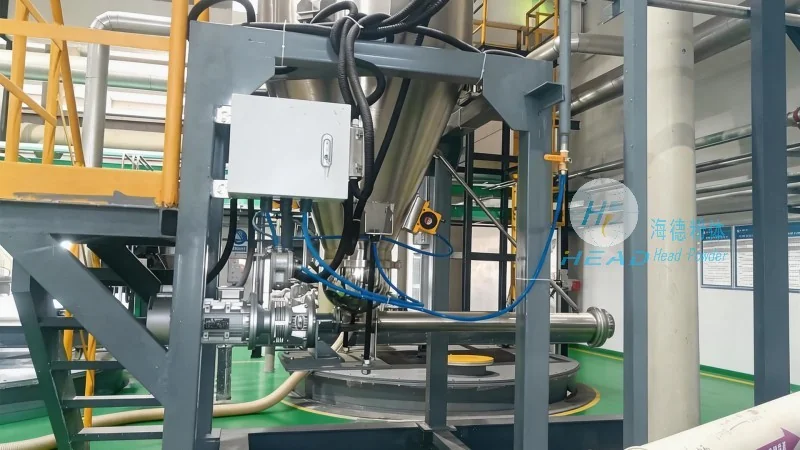
Working Principle of Tote Bag Unloading Pneumatic Conveying Equipment
The core working principle of this equipment revolves around the use of compressed air to create a pressure differential that propels bulk materials from the tote bag through a pipeline system. The process typically begins with the opening of the tote bag, which may involve mechanical or manual mechanisms to release the material. Once the bag is opened, a vacuum or pressure source is applied to the inlet of the conveying line, drawing the material into the system. The material is then carried through the pipeline by the airflow, which can be either positive pressure (air blowing the material) or negative pressure (air sucking the material). The system includes components such as a hopper, a rotary valve, and a filter to ensure smooth material flow and prevent blockages or contamination. The compressed air is supplied by an air compressor, which maintains the necessary pressure for effective conveying. The entire process is automated, allowing for continuous operation and minimizing human intervention, thereby enhancing productivity and reducing labor costs.

Key Features of Tote Bag Unloading Pneumatic Conveying Equipment
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, offers advanced tote bag unloading pneumatic conveying equipment with several distinctive features. One of the primary features is its high efficiency in material transfer, capable of handling large volumes of bulk materials quickly and reliably. The equipment is designed to handle a wide range of materials, including powders, granules, and fine particles, with minimal degradation or segregation. The system incorporates robust filtration and separation mechanisms to maintain product purity and prevent contamination, which is critical in industries like food and pharmaceuticals. Another key feature is its flexibility and adaptability, allowing for customization to suit different tote bag sizes and material characteristics. The equipment also features user-friendly controls and monitoring systems, enabling operators to track performance and troubleshoot issues in real-time. Additionally, the design emphasizes safety and compliance with industrial standards, incorporating features such as explosion-proof components and emergency shut-off systems to protect personnel and equipment. The equipment is built with durable materials, ensuring long-term reliability and low maintenance costs, which contributes to its overall cost-effectiveness.

Company Information and Location
HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in the design, development, and production of pneumatic conveying systems. The company is headquartered in Shandong, China, a region known for its robust industrial infrastructure and manufacturing capabilities. With a strong commitment to quality and innovation, HeadPowder has established itself as a trusted supplier of high-performance tote bag unloading equipment to clients worldwide. The company's products are widely used in various industries, including chemical processing, food and beverage, and pharmaceutical manufacturing, where reliable and efficient material handling is essential. HeadPowder's team of experienced engineers and technicians continuously researches and develops new technologies to improve the performance and functionality of its equipment, ensuring that clients receive cutting-edge solutions tailored to their specific needs. The company adheres to international quality standards and provides comprehensive after-sales support, including installation, maintenance, and technical assistance, to ensure customer satisfaction and long-term partnership.