

Working Principle and Features of Phosphorus Pentachloride Material Handling Equipment
Phosphorus pentachloride (PCl₅) is a highly reactive and corrosive chemical compound widely used in the production of various industrial chemicals, pharmaceuticals, and specialty materials. The safe and efficient handling of PCl₅ is critical due to its hazardous nature, making specialized material handling equipment essential for industrial applications. This article explores the working principle and key features of PCl₅ material handling equipment, highlighting how advanced engineering solutions from Shandong HeadPowder Engineering Co., Ltd. address the unique challenges associated with processing this compound.

Working Principle of Phosphorus Pentachloride Material Handling Equipment
The core working principle of PCl₅ material handling equipment revolves around maintaining strict control over temperature, pressure, and material flow to prevent decomposition or hazardous reactions. The system typically consists of several integrated components designed to handle the compound from storage to processing. First, the equipment uses sealed, corrosion-resistant containers to store PCl₅, minimizing exposure to moisture and air, which can trigger unwanted side reactions. When material is to be transferred, a pneumatic or hydraulic system activates, controlling the flow rate and pressure to ensure smooth movement through pipelines or transfer lines. Advanced control systems monitor real-time parameters such as temperature and pressure, adjusting operations automatically to maintain optimal conditions. The equipment also incorporates safety mechanisms, such as emergency shut-off valves and pressure relief systems, to prevent over-pressurization or leaks. Overall, the working principle emphasizes precision, safety, and reliability to handle PCl₅ effectively while protecting personnel and equipment.
Key Features of PCl₅ Material Handling Equipment
Shandong HeadPowder Engineering Co., Ltd. designs and manufactures PCl₅ material handling equipment with a focus on durability, safety, and operational efficiency. The key features of these systems include:
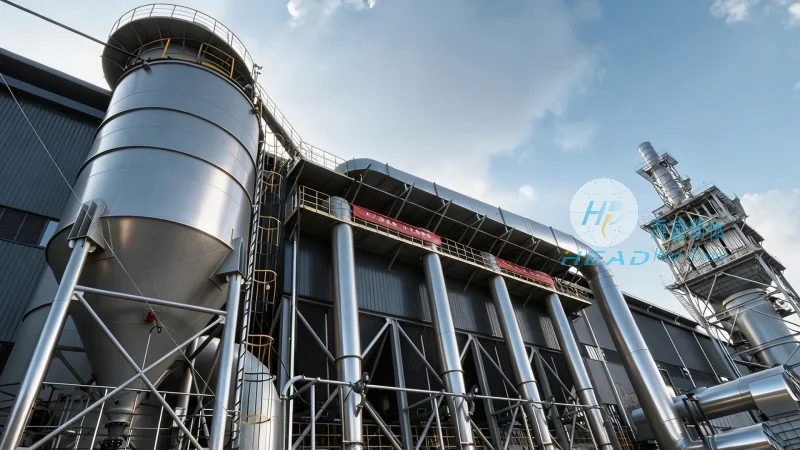
1. Corrosion-Resistant Materials: All components, including pipes, valves, and containers, are constructed from materials like Hastelloy, titanium, or specialized alloys that resist the corrosive effects of PCl₅ and its byproducts. This ensures long-term reliability and reduces maintenance costs.
2. Sealed and Airtight Design: The equipment features hermetic seals and double-walled construction to prevent leaks and exposure to the environment. This design minimizes the risk of accidental releases and complies with stringent safety regulations.
3. Advanced Control Systems: Integrated PLC (Programmable Logic Controller) and SCADA (Supervisory Control and Data Acquisition) systems allow for real-time monitoring and automated control of temperature, pressure, and flow rates. Operators can adjust parameters remotely, enhancing safety and process consistency.

4. Emergency Safety Protocols: The equipment is equipped with multiple safety features, including pressure relief valves, explosion-proof sensors, and automatic shut-off mechanisms. These systems activate in case of abnormal conditions, such as over-temperature or pressure spikes, to prevent accidents and protect personnel.
5. Modular and Scalable Design: The systems are modular, allowing for easy expansion or integration with existing industrial processes. This flexibility enables manufacturers to adapt the equipment to changing production needs without significant modifications.
6. Compliance with Industry Standards: All equipment is designed and manufactured in accordance with international safety and environmental regulations, such as those from the American Petroleum Institute (API) and the European Union (EU). This ensures that the equipment meets the highest standards for handling hazardous chemicals.

Benefits of Using PCl₅ Material Handling Equipment from Shandong HeadPowder Engineering Co., Ltd.
Investing in specialized PCl₅ material handling equipment from Shandong HeadPowder Engineering Co., Ltd. offers several significant benefits for industrial facilities. First, the equipment enhances safety by minimizing the risk of leaks, spills, or hazardous reactions, reducing the likelihood of accidents and associated costs. Second, the advanced control systems improve operational efficiency, allowing for precise control of the PCl₅ flow and reducing downtime due to maintenance or process adjustments. Third, the corrosion-resistant materials and sealed design extend the equipment's lifespan, lowering long-term maintenance and replacement costs. Additionally, the modular design enables manufacturers to scale their operations as production needs grow, providing flexibility and cost-effectiveness. Finally, compliance with international safety standards ensures that the equipment meets regulatory requirements, avoiding potential fines or operational disruptions.
Conclusion
Phosphorus pentachloride is a critical chemical in many industrial applications, but its handling requires specialized equipment to ensure safety and efficiency. The working principle and key features of PCl₅ material handling equipment, as designed by Shandong HeadPowder Engineering Co., Ltd., address the unique challenges of processing this hazardous compound. By leveraging advanced engineering, corrosion-resistant materials, and integrated control systems, these solutions provide reliable, safe, and efficient handling of PCl₅. For industrial facilities seeking to optimize their PCl₅ processing operations, investing in high-quality material handling equipment from Shandong HeadPowder Engineering Co., Ltd. is a strategic choice that enhances safety, productivity, and compliance.