

Working Principle and Features of Crystal Granule Material Conveying Lines
Crystal granule material conveying lines are essential equipment in industrial processing, designed to efficiently transport and handle crystalline materials. Understanding their working principle and key features is crucial for optimizing production processes and ensuring operational efficiency. This article provides an in-depth look at the mechanisms behind these systems and their distinct characteristics.

Company Introduction
HeadPowder, a leading manufacturer in the field, specializes in the design, development, and production of advanced material handling solutions. With a strong presence in Shandong, China, the company has built a reputation for delivering high-quality conveying systems tailored to the specific needs of various industries. The expertise and innovation of Shandong HeadPowder Engineering Co., Ltd. contribute significantly to the efficiency and reliability of crystal granule material conveying lines.
Working Principle of Crystal Granule Material Conveying Lines
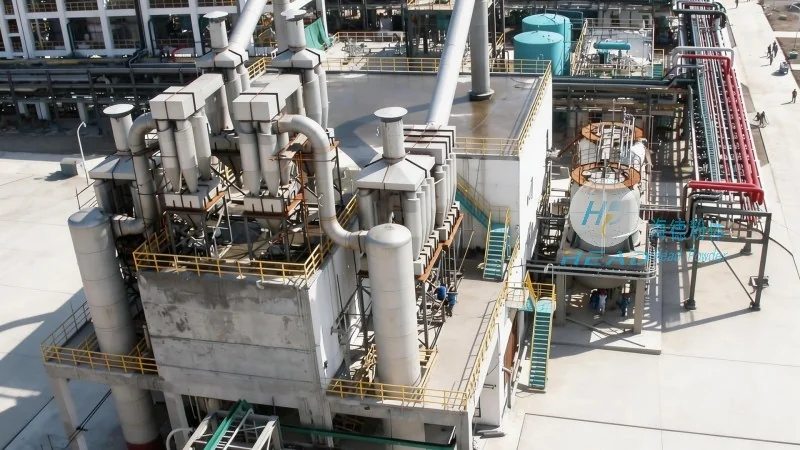
The core working principle of crystal granule material conveying lines revolves around the seamless integration of various components to facilitate the movement of granular materials. Typically, these systems consist of feeders, conveyors, and control mechanisms that work in tandem to ensure smooth material flow. The process begins with the material being fed into the system, where it is then transported through a series of stages, such as belt conveyors, screw conveyors, or pneumatic systems, depending on the material characteristics and operational requirements. Advanced control systems monitor and regulate the conveying speed, ensuring consistent and reliable transport. The entire mechanism is designed to minimize material degradation, maintain product integrity, and optimize energy consumption.
Key Features of Crystal Granule Material Conveying Lines
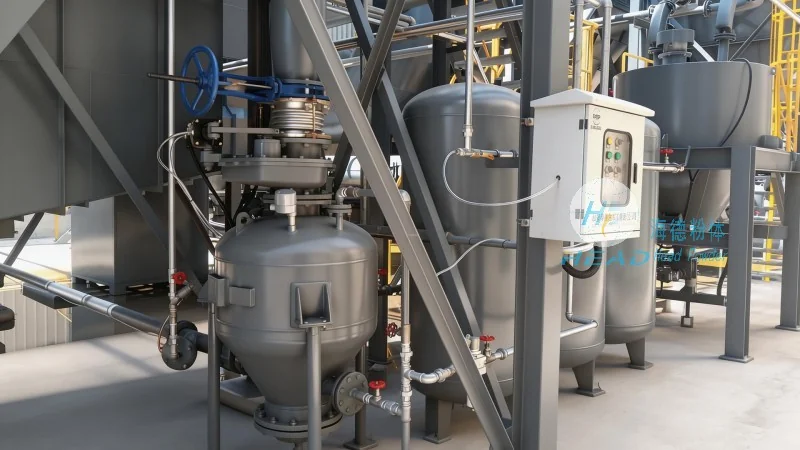
Crystal granule material conveying lines are characterized by several key features that enhance their performance and adaptability. One of the primary features is the ability to handle a wide range of material types, including fine powders, coarse granules, and crystalline substances, without causing clogging or degradation. The systems are equipped with specialized components, such as flexible hoses, adjustable speed drives, and anti-static measures, to address the unique challenges posed by different materials. Another notable feature is the modular design, which allows for easy customization and expansion to meet evolving production demands. This modularity ensures that the conveying line can be adapted to new processes or increased throughput without significant downtime. Additionally, the systems incorporate robust safety features, including overload protection and emergency stop mechanisms, to safeguard both the equipment and personnel. The integration of advanced sensors and monitoring technologies further enhances operational efficiency by providing real-time data on material flow and system performance.
Applications and Benefits
Crystal granule material conveying lines find extensive applications across multiple industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, these systems are crucial for transporting active ingredients and excipients with high precision, ensuring compliance with stringent quality standards. In food processing, they help maintain hygiene and product purity by handling granular food products efficiently. The benefits of these conveying lines extend beyond operational efficiency; they also contribute to cost reduction through minimized material waste and energy savings. The reliability and durability of the systems ensure long-term performance, reducing maintenance costs and downtime. Furthermore, the adaptability of the systems allows for seamless integration into existing production lines, enhancing overall productivity.

Conclusion
In summary, crystal granule material conveying lines are sophisticated systems that combine advanced engineering with practical design to meet the demands of modern industrial processing. The working principle, centered on efficient material transport and control, is complemented by key features such as adaptability, safety, and modularity. HeadPowder, with its expertise and commitment to quality, continues to lead in the development of these systems, providing industries with reliable and efficient solutions. The continued innovation in material handling technology ensures that these conveying lines will remain indispensable in various sectors, driving productivity and maintaining product quality.