

What is a Small Bag Pneumatic Conveying System? And Its Design Principles?
When it comes to material handling and transportation in industrial settings, pneumatic conveying systems offer efficient and flexible solutions. Among these, the small bag pneumatic conveying system stands out as a specialized equipment designed for handling and transporting bulk materials with precision and reliability. This article will explore the fundamental aspects of this system, including its definition, operational principles, and the key design considerations that make it an effective choice for various industrial applications.
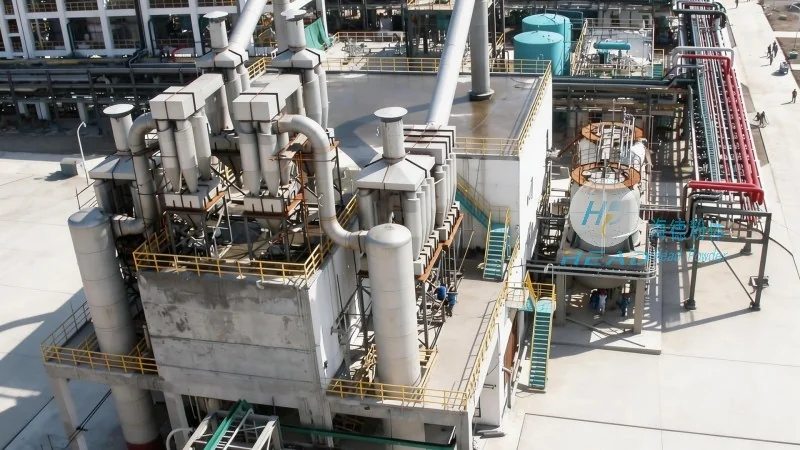
Understanding the Small Bag Pneumatic Conveying System
A small bag pneumatic conveying system is a type of pneumatic transport equipment that utilizes compressed air or other gases to move bulk materials from one location to another. Unlike traditional methods such as belt conveyors or bucket elevators, this system operates by creating a pressure differential within a sealed pipeline, allowing materials to be carried through the system as a suspension of particles in the air stream. The "small bag" aspect typically refers to the compact size and modular design of the system, making it suitable for applications where space is limited or where the material being handled is in smaller quantities.
The Core Design Principles of the System
The design of a small bag pneumatic conveying system is based on several critical principles that ensure its efficiency and reliability. The primary principle is the creation of a consistent airflow within the pipeline, which is achieved through the use of high-pressure blowers or compressors. These devices generate the necessary pressure to move the material through the system, and the design of the system must account for the specific properties of the material being conveyed, such as particle size, density, and moisture content. The system typically consists of several key components, including a hopper for material storage, a feeder to control the flow of material into the pipeline, a pipeline network that transports the material, and a receiver or discharge point where the material is collected.

Key Components and Their Functions
Each component of the small bag pneumatic conveying system plays a vital role in the overall operation. The hopper serves as the storage container for the bulk material, ensuring a steady supply to the feeder. The feeder, often a rotary valve or a screw feeder, regulates the flow of material into the pipeline, preventing blockages and maintaining a consistent material flow rate. The pipeline network is designed with appropriate diameters and bends to minimize pressure loss and ensure smooth material transport. The receiver, or discharge hopper, collects the material at the end of the system, allowing it to be discharged into a storage bin or processing equipment. Additionally, the system may include filters and cyclones to separate the material from the air stream, ensuring that the air is clean and can be recirculated or vented safely.

Applications and Benefits
Small bag pneumatic conveying systems are widely used in various industries, including pharmaceuticals, food processing, chemicals, and mining. Their benefits include high efficiency in material transport, minimal product contamination, and the ability to handle a wide range of materials, from fine powders to granules. The compact design of these systems makes them ideal for applications where space is at a premium, and their modular construction allows for easy installation and maintenance. Furthermore, the system's ability to operate in a closed environment helps to maintain product quality and safety, as it prevents exposure to external contaminants and dust.
About HeadPowder: Your Trusted Partner in Pneumatic Conveying Solutions
At Shandong HeadPowder Engineering Co., Ltd., we specialize in designing and manufacturing high-quality small bag pneumatic conveying systems tailored to meet the specific needs of our clients. With years of experience in the industry, our team of engineers and technicians has developed a deep understanding of the principles and applications of pneumatic conveying technology. We pride ourselves on our commitment to quality, innovation, and customer satisfaction, ensuring that every system we deliver meets the highest standards of performance and reliability. Our company is located in Shandong, China, and we serve clients both domestically and internationally, providing comprehensive solutions for their material handling challenges.