

What is a White Bean Chip Material Handling System? What Are Its Design Principles?
White bean chip material handling systems are specialized equipment designed to efficiently transport and manage white bean chips during processing and packaging. These systems are crucial in food processing industries, ensuring that white bean chips are handled with precision and care to maintain their quality and integrity. The design of such systems involves careful consideration of various factors, including material characteristics, processing requirements, and operational efficiency.

Overview of White Bean Chip Material Handling Systems
A white bean chip material handling system typically consists of several key components that work together to move, sort, and store white bean chips. These components may include conveyors, elevators, feeders, and storage bins. The system is engineered to handle the unique properties of white bean chips, such as their size, shape, and moisture content, to prevent damage or contamination during transport. By integrating these components, the system ensures a smooth and continuous flow of materials from raw bean processing to final packaging.

Design Principles for White Bean Chip Material Handling Systems
The design principles of a white bean chip material handling system are centered on optimizing performance, reliability, and safety. Engineers focus on creating a system that can handle the specific challenges associated with white bean chips, including their potential for sticking or clumping. Key design considerations include the use of appropriate conveyor materials, such as food-grade stainless steel, to prevent contamination and ensure easy cleaning. Additionally, the system may incorporate features like adjustable speed controls and gentle handling mechanisms to minimize product damage. The design also emphasizes energy efficiency and low maintenance requirements, making it a cost-effective solution for food processing facilities.

Components and Functionality of the System
The core components of a white bean chip material handling system include input feeders, conveyor belts, elevators, and output discharge mechanisms. Input feeders are responsible for uniformly feeding white bean chips into the system, ensuring a consistent flow rate. Conveyor belts, often equipped with special surfaces or rollers, transport the chips through the system with minimal friction. Elevators may be used to move chips vertically, connecting different levels of the processing facility. Output discharge mechanisms, such as gravity chutes or controlled discharge valves, ensure that the chips are released into storage or packaging areas in an organized manner. Each component is designed to work in harmony, minimizing downtime and maximizing throughput.
Operational Efficiency and Maintenance
Operational efficiency is a critical aspect of white bean chip material handling systems. The system is designed to operate continuously with minimal interruptions, which is essential for maintaining production schedules and meeting demand. Regular maintenance is essential to keep the system running smoothly. This includes cleaning conveyor surfaces, checking for wear and tear on components, and ensuring that all mechanisms are properly lubricated. The use of durable materials and robust construction helps to extend the lifespan of the system and reduce long-term maintenance costs. Additionally, the system may be equipped with monitoring systems that alert operators to potential issues, allowing for quick troubleshooting and repairs.
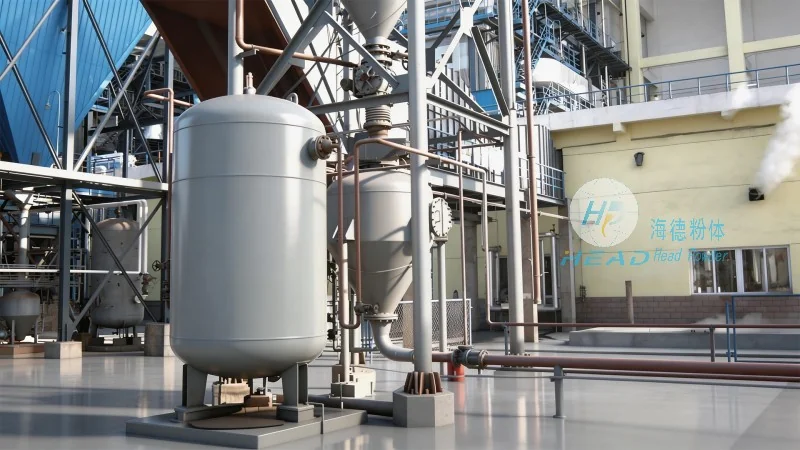
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of material handling systems for the food processing industry. With a focus on innovation and quality, HeadPowder specializes in designing and manufacturing equipment tailored to the unique needs of food processors. The company is headquartered in Shandong, China, and has a strong reputation for delivering reliable and efficient solutions to its clients. HeadPowder's expertise in material handling technology ensures that their systems are optimized for performance, safety, and cost-effectiveness, making them a trusted partner for food processing facilities worldwide.