

What is an Automatic Powder Feeding and Conveying System Equipment? What are its Design Principles?
In industrial manufacturing, the efficient handling of powders is a critical process that impacts productivity and product quality. An automatic powder feeding and conveying system equipment is a specialized solution designed to automate the intake, transport, and distribution of bulk powders. This equipment is essential for industries such as pharmaceuticals, food processing, chemicals, and materials science, where precise control over powder flow is paramount. The system integrates advanced technologies to ensure consistent performance, minimize human error, and enhance operational safety.

Key Components of the System
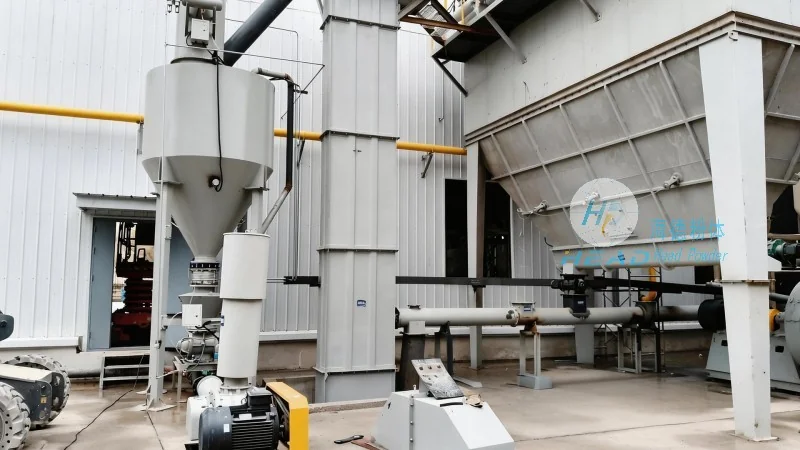
The automatic powder feeding and conveying system typically consists of several core components that work in harmony to achieve seamless operation. These components include a powder feeder, which is responsible for controlling the rate of powder discharge from a storage container. The feeder may use mechanisms like vibratory, screw, or rotary designs to regulate flow. A conveyor system, often a pneumatic or mechanical conveyor, transports the powder from the feeder to the processing or packaging area. Additionally, a control unit manages the entire process, using sensors and feedback mechanisms to adjust parameters in real-time. The system may also incorporate a hopper or silo for bulk storage, ensuring a continuous supply of material. Each component is engineered to meet specific operational requirements, such as material compatibility, flow rate, and environmental conditions.

Design Principles Behind the System
The design principles of an automatic powder feeding and conveying system are centered on precision, reliability, and adaptability. Precision is achieved through the use of advanced control algorithms and sensors that monitor variables like pressure, flow rate, and temperature. This allows for real-time adjustments to maintain consistent performance. Reliability is ensured by incorporating redundant systems and robust materials that can withstand harsh industrial environments. The system is also designed to be adaptable, with modular components that can be easily reconfigured to handle different powder types or process requirements. For example, the feeder may be adjusted to accommodate varying particle sizes or moisture content, while the conveyor can be scaled to handle different volumes. The design also emphasizes safety, with features like overload protection and emergency stop mechanisms to prevent accidents.

Applications and Benefits
The automatic powder feeding and conveying system finds wide applications across various industries. In the pharmaceutical industry, it ensures the accurate and sterile handling of active ingredients, reducing contamination risks. In food processing, it maintains hygiene standards while efficiently moving ingredients like flour or sugar. In chemical manufacturing, it enables precise dosing of reagents, improving reaction efficiency and product consistency. The benefits of this system extend beyond operational efficiency; it also enhances safety by minimizing manual handling of powders, which can be hazardous due to dust explosions or inhalation risks. Furthermore, the automation reduces labor costs and increases throughput, making it a cost-effective solution for high-volume production.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in powder handling equipment. With a strong presence in China, the company has established itself as a trusted provider of high-quality automatic powder feeding and conveying systems. HeadPowder's commitment to innovation and customer satisfaction has enabled it to serve a diverse range of industries, from pharmaceuticals to food processing. The company's products are designed to meet international standards and are backed by comprehensive technical support and after-sales service. HeadPowder's expertise in powder technology ensures that clients receive tailored solutions that address their specific operational challenges, contributing to improved productivity and safety in their production processes.
Conclusion
An automatic powder feeding and conveying system equipment is a sophisticated solution that revolutionizes the way powders are handled in industrial settings. By integrating advanced design principles and components, this system ensures precision, reliability, and efficiency in powder processing. The benefits of such equipment extend to improved safety, reduced labor costs, and enhanced product quality. As industries continue to demand higher standards of performance and safety, the role of these systems becomes increasingly critical. For businesses seeking to optimize their powder handling processes, investing in a well-designed automatic system is a strategic decision that can yield significant long-term advantages.