

Working Principle and Features of Sorghum Distillers Grains Pneumatic Conveying System Equipment
This article provides an overview of the working principle and key features of the sorghum distillers grains pneumatic conveying system equipment, manufactured by Shandong HeadPowder Engineering Co., Ltd., a company based in Shandong, China. The system is designed to efficiently handle sorghum distillers grains, a byproduct of the distillation process, ensuring optimal material transport in industrial settings.

Working Principle of the Pneumatic Conveying System
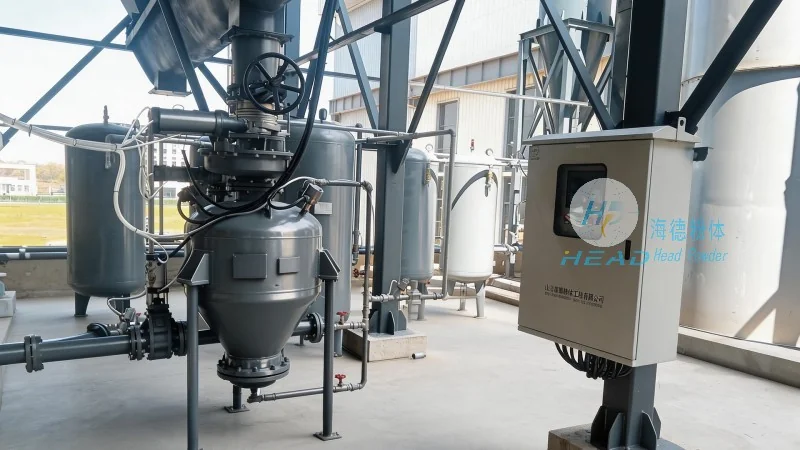
The sorghum distillers grains pneumatic conveying system operates on the principle of pneumatic transport, where material is moved through a pipeline using a combination of air or gas flow. The system typically consists of a hopper for material storage, a conveyor line, and a control unit. Material is fed into the hopper and then drawn into the conveyor line by the air flow generated by a blower or compressor. The air flow carries the distillers grains through the pipeline to the discharge point, where the material is deposited. The system can be either positive or negative pressure, depending on the specific application and material characteristics. The positive pressure system uses compressed air to push the material, while the negative pressure system uses suction to draw the material. The choice of system depends on factors such as the distance of transport, the volume of material, and the need for dust control. In some applications, a combination of both positive and negative pressure is used, known as a dual-pressure system, which offers flexibility in handling different material types and distances. The system may also include additional components such as a rotary valve at the inlet to control the flow of material, a filter or separator at the discharge to remove air and fine particles, and a pressure regulator to maintain consistent air pressure.

Key Features of the Sorghum Distillers Grains Pneumatic Conveying System
The sorghum distillers grains pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers several key features that enhance its performance and reliability. First, the system is designed for high efficiency in material transport, minimizing the time and labor required for handling sorghum distillers grains. The use of pneumatic transport reduces the need for manual handling and reduces the risk of material contamination. Second, the system is equipped with advanced control technology, allowing for precise control of the air flow and material feed rate. This ensures consistent and reliable operation, even with varying material conditions. Third, the system is constructed with high-quality materials, such as stainless steel, to withstand the corrosive nature of sorghum distillers grains and ensure long-term durability. Fourth, the system is designed for easy maintenance and cleaning, with features such as easy-to-remove components and self-cleaning mechanisms. This reduces downtime and maintenance costs. Fifth, the system incorporates safety features, such as explosion-proof design for the blower and control unit, to protect against potential hazards in industrial environments. Sixth, the system is designed with noise reduction measures, such as soundproof enclosures and low-noise blower motors, to minimize noise pollution and create a more comfortable working environment. Finally, the system is customizable to meet the specific needs of different industrial applications, allowing for flexibility in design and operation.
Application and Benefits
The sorghum distillers grains pneumatic conveying system is widely used in the food and beverage industry, particularly in the production of alcoholic beverages. The system is used to transport sorghum distillers grains from the distillation process to storage or further processing facilities. The benefits of using this system include improved efficiency, reduced labor costs, and enhanced product quality. The system also helps to maintain the quality of the distillers grains by minimizing exposure to air and moisture, which can affect the flavor and nutritional value of the product. Additionally, the system reduces the risk of dust and odor emissions, contributing to a safer and more environmentally friendly operation. By efficiently handling sorghum distillers grains, the system supports the overall production process, allowing manufacturers to optimize their operations and meet increasing demand for high-quality alcoholic beverages. The system's reliability and durability ensure consistent performance over long periods, reducing the need for frequent repairs and replacements, which further contributes to cost savings and operational efficiency.