

Principle and Operational Characteristics of Sorghum Distillers Grains Pneumatic Conveying System
HeadPowder Engineering specializes in the design and implementation of advanced pneumatic conveying systems tailored for the transportation of sorghum distillers grains. This technology is crucial in the distillery industry, where efficient handling of byproducts like distillers grains is essential for maintaining operational efficiency and product quality. The system combines precision engineering with robust materials to ensure reliable and consistent performance in high-demand environments.


Principle of Pneumatic Conveying
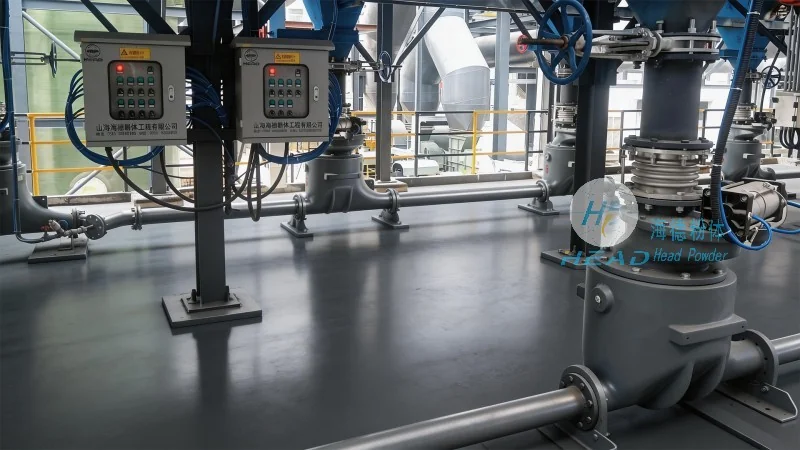
The core principle of the pneumatic conveying system involves the use of air or gas to transport bulk materials through a pipeline. In the case of sorghum distillers grains, the system employs a positive displacement or pressure-type design, which is ideal for handling fine to medium-sized particles with varying moisture content. The process begins with the material being fed into a hopper, where it is then drawn into the conveying line by a powerful blower or compressor. The air flow creates a low-pressure zone that pulls the material along the pipeline, ensuring a continuous and controlled flow. Key components include the feed hopper, rotary valve, airlock, and the conveying pipeline itself. The system's efficiency is enhanced by the use of appropriate air velocity and pressure, which are carefully calibrated to prevent material degradation and ensure minimal loss during transport.

Operational Characteristics in Work Scenarios
The pneumatic conveying system for sorghum distillers grains is designed to operate effectively in various industrial settings, particularly in distillery plants where space optimization and hygiene are critical. The system's flexibility allows it to integrate seamlessly with existing production lines, reducing the need for extensive modifications to the facility. In typical work scenarios, the system handles the transportation of distillers grains from the fermentation and distillation stages to storage silos or processing units. The continuous operation mode ensures that material is moved without interruption, maintaining a steady supply for downstream processes such as animal feed production or further processing. The system's ability to handle varying material loads and moisture levels makes it adaptable to different production volumes and seasonal demands. Additionally, the enclosed pipeline design minimizes dust emissions and improves workplace safety, aligning with modern industrial standards for environmental and occupational health.
Company Information and Expertise
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading provider of engineering solutions for the food and beverage industry. With a focus on innovation and customer-centric design, the company has developed specialized pneumatic conveying systems that meet the unique requirements of distillery operations. HeadPowder's team of engineers and technicians brings extensive experience in material handling and process optimization, ensuring that each system is tailored to the specific needs of the client. The company's headquarters is located in Shandong, China, where it maintains state-of-the-art facilities for research, development, and manufacturing. HeadPowder's commitment to quality and reliability has earned it a reputation as a trusted partner in the industry, delivering solutions that enhance operational efficiency and reduce costs for its clients.