

Principle and Working Scene Characteristics of Stone Aggregate Powder Conveying
Stone aggregate powder conveying is a critical process in modern material handling, particularly for transporting stone aggregate materials efficiently and safely. Understanding the underlying principles and the specific characteristics of different working scenes is essential for optimizing operations in construction, industrial, and related sectors. This article delves into the core principles of stone aggregate powder conveying systems and highlights the key working scene characteristics that define their application and performance.

About HeadPowder: A Leading Provider in Material Handling Solutions
HeadPowder, the professional brand under Shandong HeadPowder Engineering Co., Ltd., specializes in the design, manufacturing, and implementation of advanced material conveying systems. With a strong presence in China, particularly in Shandong, the company has established itself as a trusted partner for businesses seeking reliable solutions for handling stone aggregate powders. The company’s commitment to innovation and customer-centric service ensures that clients receive tailored systems that meet their unique operational needs. By leveraging years of industry experience, HeadPowder delivers high-performance conveying solutions that enhance productivity and operational efficiency.
The Fundamental Principle of Stone Aggregate Powder Conveying
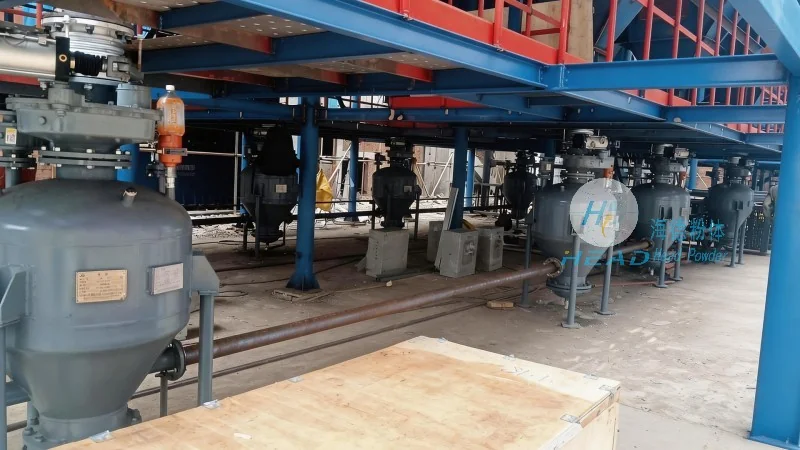
The core principle of stone aggregate powder conveying involves the use of specialized equipment to transport loose, granular materials like stone aggregates through a system of pipes or channels. This process typically relies on mechanical forces such as air pressure, vacuum, or mechanical drive mechanisms to move the material from the source to the destination. The system is designed to handle materials with varying particle sizes and densities, ensuring consistent and reliable transport. Key components of a typical stone aggregate powder conveying system include feed hoppers, conveying ducts, control valves, and discharge units. Each component plays a crucial role in maintaining the flow of material and preventing blockages or inefficiencies. The principle also emphasizes the importance of maintaining proper air or gas flow rates to ensure the material is conveyed smoothly without degradation or loss.

Key Working Scene Characteristics of Stone Aggregate Powder Conveying Systems
The effectiveness of stone aggregate powder conveying systems is significantly influenced by the specific working scene characteristics. These characteristics include the nature of the material being conveyed, the distance and layout of the conveying route, the environmental conditions, and the operational requirements of the application. In construction sites, for example, the system must handle large volumes of stone aggregates over varying distances, often in outdoor environments with potential weather impacts. The design must account for factors like dust control, material moisture, and the need for flexible routing to accommodate changing project needs. In industrial settings, such as mining or processing facilities, the system may need to convey materials with higher particle sizes or varying compositions, requiring robust equipment capable of handling abrasive or corrosive materials. The working scene also dictates the choice of conveying technology, whether pneumatic, mechanical, or a combination of both, to optimize performance and minimize operational costs. Additionally, the system must integrate seamlessly with existing infrastructure, ensuring compatibility with other equipment and processes within the facility. This integration is critical for maintaining overall operational efficiency and reducing downtime.
Application Scenarios and Operational Advantages
Stone aggregate powder conveying systems find widespread application across various industries, including construction, mining, and manufacturing. In construction, these systems are used to transport aggregates from storage areas to mixing sites or to different parts of a building project, improving material flow and reducing manual handling. The ability to convey large volumes of material over long distances efficiently reduces labor costs and enhances project timelines. In mining operations, the system facilitates the transport of raw stone aggregates from extraction sites to processing plants, enabling continuous production and minimizing material loss. The operational advantages of these systems extend beyond efficiency, as they also contribute to improved safety by reducing the need for manual handling of heavy or dusty materials. Furthermore, the systems are designed to minimize environmental impact by controlling dust emissions and ensuring proper material containment. This makes them a sustainable choice for modern industrial operations. The adaptability of stone aggregate powder conveying systems to different working scene characteristics allows them to be customized for specific applications, ensuring optimal performance and cost-effectiveness.

Conclusion and Future Directions
Stone aggregate powder conveying systems, as explained above, are essential for modern material handling, offering efficient, reliable, and safe solutions for transporting stone aggregates. The principles underlying these systems, combined with the specific characteristics of different working scenes, enable the design of tailored solutions that meet the unique needs of various industries. HeadPowder, as a leading provider in this field, continues to innovate and improve its conveying systems to enhance performance and customer satisfaction. By understanding the core principles and working scene characteristics, businesses can make informed decisions when selecting and implementing stone aggregate powder conveying systems, ultimately improving operational efficiency and achieving their project goals. As technology advances, the future of stone aggregate powder conveying is likely to see further integration of automation and smart technologies, leading to even more efficient and sustainable material handling solutions.