

Principle and Working Scene Characteristics of Fly Ash Silo Powder Pneumatic Conveying Line
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. This article delves into the core principles and operational characteristics of the fly ash silo powder pneumatic conveying line, a critical component in modern industrial applications.

Understanding the Core Principle of Fly Ash Silo Powder Pneumatic Conveying
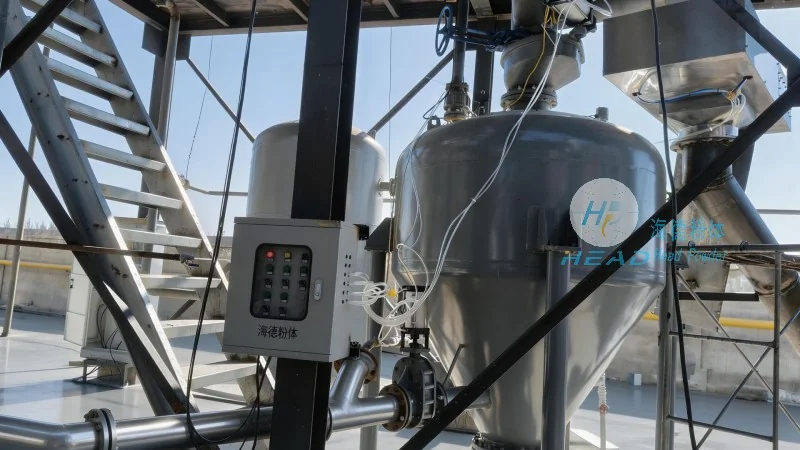
The fly ash silo powder pneumatic conveying line operates on the fundamental principle of using air as the conveying medium to transport dry powders, such as fly ash, from the storage silo to the processing or disposal units. This system typically consists of a silo, a conveying pipeline, a blower or compressor, and a control system. The process begins when the material is drawn from the silo by creating a negative pressure or positive pressure within the pipeline, depending on the system design. The air, carrying the fly ash particles, is then directed through the pipeline to the target location, where the material is discharged and the air is filtered or recycled.

Key Components and Their Functions in the System
Several key components work in tandem to ensure efficient and reliable operation of the fly ash silo powder pneumatic conveying line. The silo serves as the primary storage vessel, maintaining the fly ash in a contained environment. The conveying pipeline, often made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of fly ash particles. The blower or compressor provides the necessary air pressure to move the material through the pipeline. Additionally, the control system, which may include sensors, valves, and automation software, monitors and regulates the flow rate, pressure, and other critical parameters to optimize performance and prevent system failures.

Working Scene Characteristics: Industrial Applications and Benefits
The fly ash silo powder pneumatic conveying line is widely used in various industrial settings, particularly in power plants, cement factories, and waste management facilities. Its primary advantage lies in the ability to transport fly ash over long distances with minimal maintenance and low operational costs compared to traditional methods like belt conveyors or truck transport. The system is also highly flexible, allowing for multiple discharge points and integration with other processing equipment. Furthermore, the enclosed pipeline design helps in controlling dust emissions, enhancing workplace safety and environmental compliance. In power plants, for instance, this system efficiently transfers fly ash from the boiler to the storage silo or to the disposal site, ensuring smooth operation and compliance with environmental regulations.
Operational Efficiency and Advantages in Real-World Scenarios
Real-world applications of the fly ash silo powder pneumatic conveying line demonstrate significant operational efficiencies. By eliminating the need for manual handling and reducing the risk of material spillage, the system enhances workplace safety. The enclosed design also minimizes dust exposure, which is crucial for maintaining a healthy work environment and complying with occupational health standards. From a cost perspective, the system reduces labor costs associated with manual transport and lowers the risk of material loss or contamination. In addition, the ability to adjust the conveying rate and pressure allows for precise control over the material flow, adapting to varying production demands. This adaptability makes the system suitable for both large-scale industrial operations and smaller-scale facilities requiring reliable material transport solutions.
Conclusion: The Role of HeadPowder in Delivering Advanced Pneumatic Conveying Solutions
HeadPowder Engineering Co., Ltd., based in Shandong, China, is committed to providing innovative and efficient pneumatic conveying solutions tailored to the specific needs of industrial clients. The fly ash silo powder pneumatic conveying line exemplifies the company's expertise in designing systems that balance performance, reliability, and cost-effectiveness. By leveraging advanced engineering and quality materials, HeadPowder ensures that its clients receive systems that meet the highest standards of safety, efficiency, and environmental compliance. As the demand for sustainable and efficient material handling solutions grows, the fly ash silo powder pneumatic conveying line remains a vital component in modern industrial operations, supported by the expertise and dedication of companies like HeadPowder.