

Design of a Magnesium Sulfate Pneumatic Conveying System
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for industrial applications. This article focuses on the detailed design of a magnesium sulfate pneumatic conveying system, highlighting the technical considerations, material selection, and operational efficiency that define such systems.

System Overview and Core Components
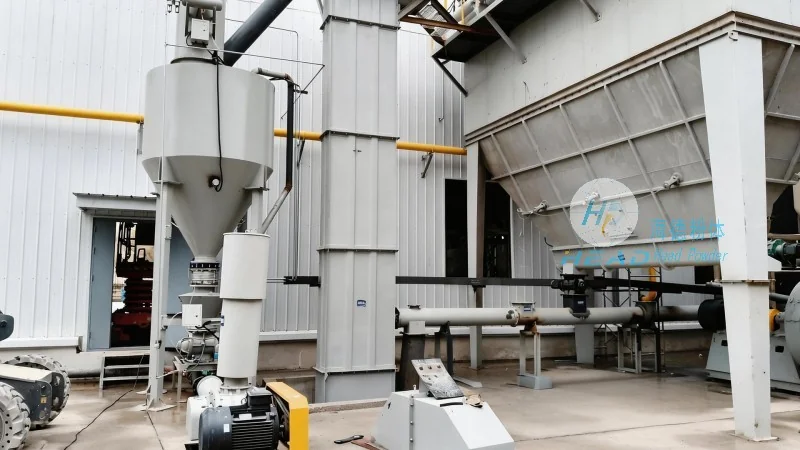
The magnesium sulfate pneumatic conveying system is engineered to transport bulk magnesium sulfate efficiently and safely from storage silos to processing units or packaging areas. The system comprises several critical components, including a hopper, a rotary valve, a pneumatic conveyor line, and a dust collection system. Each component is selected to withstand the corrosive and abrasive nature of magnesium sulfate, ensuring long-term reliability and minimal maintenance.
Material Selection and Equipment Design
For the magnesium sulfate pneumatic conveying system, high-quality stainless steel and corrosion-resistant materials are employed throughout the system. The hopper and silo are constructed from 316L stainless steel to prevent chemical degradation and ensure durability. The rotary valve, a key component for controlling material flow, is designed with a double-seal mechanism to minimize leakage and maintain product purity. The pneumatic conveyor line uses flexible, food-grade PVC or PTFE hoses, which are resistant to chemical exposure and provide smooth material transport. The dust collection system, integrated with high-efficiency filters, ensures compliance with environmental regulations and maintains a clean working environment.
Operational Efficiency and Flow Control
Efficient flow control is essential for the smooth operation of the magnesium sulfate pneumatic conveying system. The system incorporates a variable frequency drive (VFD) to regulate the air flow and pressure, allowing for precise control over the conveying speed. This feature enables the system to handle varying material loads and maintain consistent product flow rates. Additionally, the system includes a pressure sensor and a flow meter to monitor real-time performance, providing operators with immediate feedback on system health and potential issues.

Safety and Maintenance Considerations
HeadPowder prioritizes safety and reliability in the design of the magnesium sulfate pneumatic conveying system. The system is equipped with safety interlocks that automatically shut down the conveyor in case of blockages or overpressure, preventing equipment damage and ensuring operator safety. Regular maintenance is facilitated by easy access to components, such as the rotary valve and filter housings, which can be serviced without extensive disassembly. The use of corrosion-resistant materials and robust construction reduces the need for frequent repairs, extending the system's operational lifespan.
Customization and Application Flexibility
HeadPowder understands that industrial applications vary, and the magnesium sulfate pneumatic conveying system is designed with flexibility in mind. The system can be customized to accommodate different material quantities, conveyor lengths, and environmental conditions. For example, the conveyor line can be extended or modified to connect multiple processing units, and the hopper size can be adjusted based on storage capacity requirements. This adaptability ensures that the system meets the specific needs of each client, providing a tailored solution for their magnesium sulfate handling requirements.