

Design of a Dry Powder Air-Lift Conveyor for Flocculants
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and manufacturing of advanced material handling systems. Our primary focus is on providing efficient and reliable solutions for the transportation of dry powders, particularly in industrial applications involving flocculants. The dry powder air-lift conveyor is a critical piece of equipment that ensures the safe and effective movement of these materials, which are essential in processes such as water treatment, chemical processing, and environmental remediation.
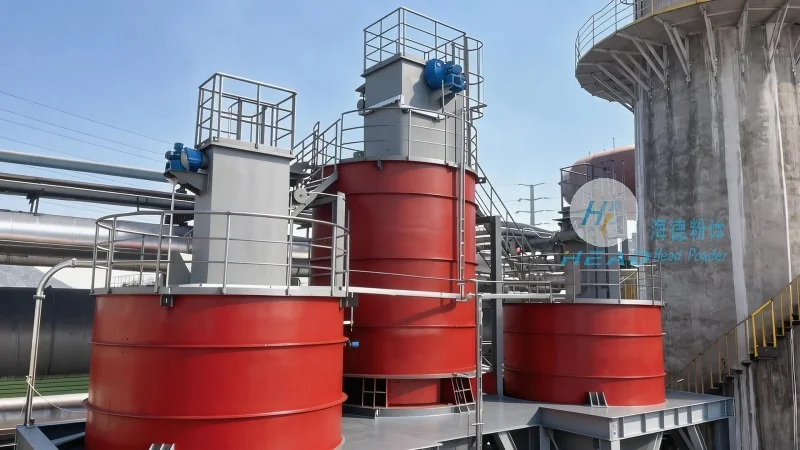
Key Features and Technical Specifications
The dry powder air-lift conveyor designed by HeadPowder is engineered to meet the stringent demands of modern industrial operations. It utilizes an air-lift mechanism, which combines the principles of pneumatic conveying with vertical or inclined transport capabilities. This design allows for the efficient transfer of flocculant powders from storage silos or hoppers to processing units, minimizing the risk of material degradation and contamination. The system incorporates high-quality components, including durable metal construction, precise air control valves, and advanced filtration systems to ensure optimal performance and longevity.

Advantages of Our Air-Lift Conveyor System
One of the key advantages of the HeadPowder dry powder air-lift conveyor is its ability to handle abrasive and fine powders without causing blockages or wear. The air-lift design reduces the need for mechanical components that are prone to failure in high-abrasion environments, thereby lowering maintenance costs and increasing operational uptime. Additionally, the system is equipped with adjustable air pressure controls, enabling operators to optimize the conveying rate based on the specific characteristics of the flocculant being transported. This flexibility ensures that the conveyor can be tailored to meet the unique requirements of each industrial application.

Application Scenarios and Industry Use Cases
The dry powder air-lift conveyor is widely used in various industries where flocculants are a critical component. In water treatment plants, for example, the system efficiently delivers flocculant powders to the mixing tanks, ensuring consistent coagulation and flocculation processes. In chemical manufacturing, it facilitates the transport of specialized flocculants used in polymer production and wastewater treatment. The conveyor's ability to handle large volumes of material at a controlled rate makes it an ideal solution for both batch and continuous production lines. Furthermore, its compact design allows for installation in confined spaces, making it suitable for retrofitting into existing facilities without major structural modifications.
Customization and Integration Capabilities
HeadPowder understands that each industrial operation has unique requirements. Therefore, our dry powder air-lift conveyor is designed to be highly customizable. We offer options for different material capacities, air pressure ranges, and control systems to suit specific operational needs. The system can be integrated with existing process control networks, allowing for seamless monitoring and automation. This integration enhances overall plant efficiency and provides real-time data on material flow, enabling better decision-making and process optimization.

Quality Assurance and Maintenance Support
At HeadPowder, we prioritize quality and reliability. Our dry powder air-lift conveyor undergoes rigorous testing and quality checks before delivery to ensure it meets the highest industry standards. We provide comprehensive maintenance and support services to our clients, including regular inspections, component replacement, and technical assistance. Our team of experienced engineers is available to provide guidance on optimal operation and troubleshooting, ensuring that the conveyor continues to perform at its best throughout its service life.