

Components of Organic Fertilizer Granule Pneumatic Conveying
Organic fertilizer granule pneumatic conveying systems are essential in modern agricultural and industrial applications, facilitating the efficient transport of organic fertilizer granules from production sites to storage or application areas. The technology behind these systems involves a combination of mechanical and pneumatic components that work in tandem to ensure reliable and efficient material handling. This article explores the key components that make up organic fertilizer granule pneumatic conveying systems, providing insights into the technology used by industry leaders like Shandong HeadPowder Engineering Co., Ltd.
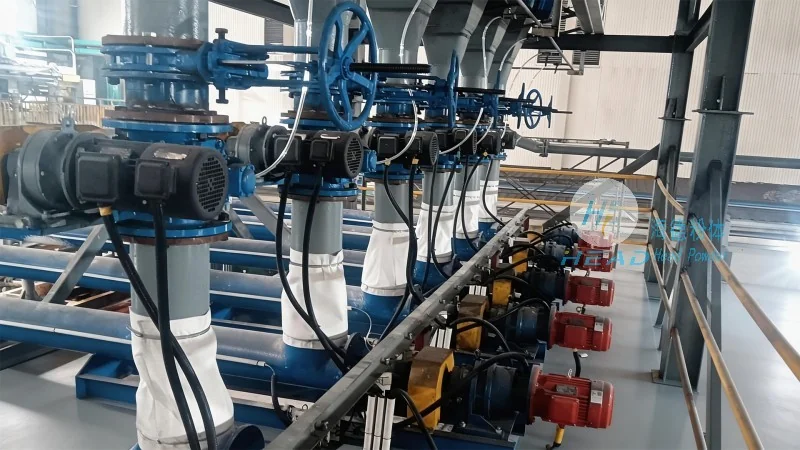
Introduction to Organic Fertilizer Granule Pneumatic Conveying
Organic fertilizer granule pneumatic conveying is a method of transporting granular organic fertilizers through a pipeline using a combination of air and mechanical forces. Unlike traditional bulk material handling methods, pneumatic conveying offers advantages such as reduced dust generation, lower labor costs, and improved safety. The system typically consists of several interconnected components, each playing a critical role in the overall operation. Understanding these components is crucial for optimizing performance and ensuring the longevity of the conveying system.
Key Components of Organic Fertilizer Granule Pneumatic Conveying Systems
The core components of an organic fertilizer granule pneumatic conveying system include the feed hopper, air compressor or blower, conveying pipeline, separation and collection equipment, and control systems. Each component is designed to work together to achieve efficient material transport. The feed hopper is responsible for storing and feeding the organic fertilizer granules into the system, ensuring a consistent flow of material. It is typically equipped with a gate valve or feeder to regulate the discharge rate.
The air compressor or blower provides the necessary air pressure to move the granules through the pipeline. This component is critical as it determines the conveying velocity and the overall system efficiency. Different types of compressors, such as rotary lobe or centrifugal, may be used depending on the specific application requirements and the characteristics of the organic fertilizer granules.
The conveying pipeline is the main channel through which the organic fertilizer granules are transported. It is usually made of materials like stainless steel or plastic, chosen for their resistance to corrosion and wear from the organic fertilizer. The pipeline design, including the diameter and length, affects the conveying capacity and pressure drop. Proper pipeline layout, with appropriate bends and fittings, is essential to minimize energy consumption and prevent material blockages.
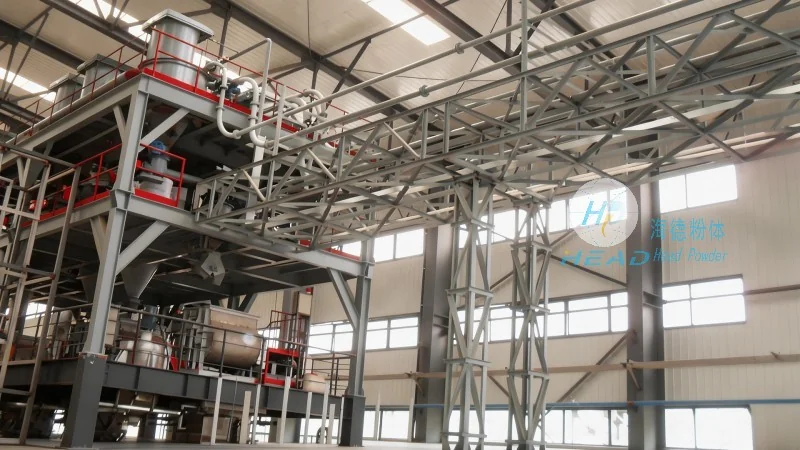
Separation and collection equipment is used to separate the conveyed organic fertilizer granules from the air stream and collect them in a designated storage or application container. This component typically includes a cyclone separator or a bag filter, which uses centrifugal force or filtration to separate the solid granules from the air. The collected granules are then discharged into a hopper or storage tank, while the cleaned air is discharged to the atmosphere or recirculated if necessary.
Control systems are integral to the operation of the pneumatic conveying system, allowing for monitoring and adjustment of key parameters such as air pressure, flow rate, and material level. Modern control systems often include sensors and automation equipment to ensure optimal performance and prevent system failures. These systems help operators to maintain consistent conveying rates and detect any issues in real-time, improving overall system reliability.
Role of Shandong HeadPowder Engineering Co., Ltd. in Organic Fertilizer Granule Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing high-quality organic fertilizer granule pneumatic conveying systems. With years of experience and a commitment to innovation, the company has developed advanced solutions tailored to the specific needs of the agricultural and industrial sectors. The company's products are known for their durability, efficiency, and reliability, making them a preferred choice for customers worldwide.
HeadPowder's engineers work closely with clients to understand their unique requirements, from the type of organic fertilizer granules to the distance and volume of material to be conveyed. By leveraging their expertise in material handling technology, the company provides customized solutions that meet the highest standards of performance and safety. The company's focus on quality and customer satisfaction has earned it a reputation as a trusted partner in the industry.

Benefits of Organic Fertilizer Granule Pneumatic Conveying
Organic fertilizer granule pneumatic conveying offers several benefits over traditional handling methods. One of the primary advantages is the reduction in dust and airborne particles, which improves workplace safety and reduces the risk of respiratory issues for workers. Additionally, the system minimizes material spillage and loss, ensuring that more of the organic fertilizer reaches its intended destination.
The technology also offers flexibility in terms of layout and installation. Pneumatic conveying systems can be designed to follow existing infrastructure or be installed in new facilities, allowing for easy integration into existing production lines. This flexibility makes it suitable for a wide range of applications, from small-scale farms to large industrial operations.
Another benefit is the energy efficiency of pneumatic conveying systems. By using air as the conveying medium, the system can achieve high material throughput with relatively low energy consumption compared to other methods like truck or rail transport. This not only reduces operational costs but also contributes to a more sustainable and environmentally friendly approach to material handling.
Conclusion
Organic fertilizer granule pneumatic conveying systems are a critical component of modern material handling, offering efficient, safe, and cost-effective solutions for transporting organic fertilizers. The key components, including the feed hopper, air compressor, conveying pipeline, separation equipment, and control systems, work together to ensure reliable operation. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these systems, leveraging their expertise to meet the evolving needs of the agricultural and industrial sectors. As the demand for organic fertilizers continues to grow, the importance of efficient and reliable conveying systems will only increase, making this technology a cornerstone of sustainable material handling practices.