

[Brief Introduction to Bentonite Pneumatic Conveying and the Working Principle of Pneumatic Conveyin
Bentonite, a versatile clay mineral, plays a crucial role in various industrial processes due to its unique properties such as high swelling capacity and excellent thixotropy. Its applications range from drilling mud additives to environmental remediation and construction materials. The efficient handling and transportation of bentonite are essential for optimizing production workflows and ensuring product quality. Pneumatic conveying systems have emerged as a reliable solution for transporting bulk materials like bentonite, offering advantages over traditional methods like belt conveyors or trucks.

Understanding Bentonite and Pneumatic Conveying Systems
Bentonite is a natural clay composed primarily of montmorillonite, which gives it the ability to absorb water and expand significantly. This property makes it ideal for applications requiring thickening, filtration, and stabilization. Pneumatic conveying, on the other hand, is a method of transporting bulk materials through a pipeline using air or other gases as the conveying medium. It involves the creation of a low-pressure or high-pressure air stream that propels the material forward. This technology is particularly suitable for handling fine powders and granular materials, including bentonite, due to its ability to minimize dust generation and maintain product integrity.
The Role of Bentonite in Industrial Applications
In industrial settings, bentonite is widely used in the oil and gas industry as a drilling fluid additive to maintain wellbore stability and prevent fluid loss. It is also employed in the paper manufacturing industry as a filler and coating agent, enhancing paper strength and smoothness. Additionally, bentonite is utilized in the environmental sector for soil remediation, as it can effectively absorb and immobilize contaminants. The consistent quality and purity of bentonite are critical for these applications, making reliable material handling systems indispensable.

Introduction to Pneumatic Conveying Technology
Pneumatic conveying systems are designed to transport bulk materials from one location to another without the need for mechanical components like belts or buckets. The system typically consists of a hopper, a conveyor line, and a receiver. The material is fed into the hopper, where it is then drawn into the conveyor line by a vacuum or pressure source. The air flow carries the material through the pipeline, ensuring it reaches the destination without clogging or degradation. This method is particularly effective for transporting fine powders like bentonite, as it prevents particle agglomeration and maintains the material's properties.
How Pneumatic Conveying Systems Work
The operation of a pneumatic conveying system involves several key steps. First, the material is loaded into the hopper, which is equipped with a feeder to control the flow rate. The feeder then introduces the material into the conveying line. Simultaneously, a fan or blower generates the necessary air flow, either by creating a vacuum (in suction systems) or applying pressure (in pressure systems). The air stream propels the material through the pipeline, with the velocity and pressure maintained to ensure efficient transport. At the receiving end, the material is separated from the air using a cyclone or filter, and the air is either recirculated or vented. This process allows for continuous and automated material handling, reducing labor costs and improving operational efficiency.

Key Components of a Pneumatic Conveying System
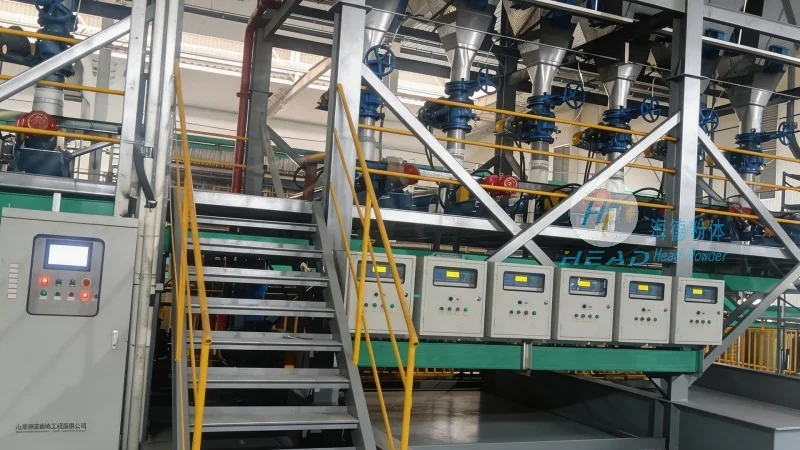
Several components are essential for the proper functioning of a pneumatic conveying system. The hopper serves as the storage and feeding unit, ensuring a consistent supply of material. The feeder, such as a rotary valve or screw feeder, controls the flow rate and prevents material from clogging. The conveyor line, made of materials like stainless steel or plastic, is designed to withstand the pressure and temperature of the conveying process. The fan or blower provides the necessary air flow, with options including centrifugal fans for suction systems and positive displacement blowers for pressure systems. The receiver, equipped with a dust collector or cyclone, separates the material from the air and collects it in a storage bin. These components work together to ensure the efficient and reliable transport of bentonite and other bulk materials.
Applications of Bentonite Pneumatic Conveying
Bentonite pneumatic conveying systems are widely used in various industries due to their versatility and efficiency. In the oil and gas sector, these systems are employed to transport bentonite from storage facilities to drilling sites, ensuring a continuous supply of drilling fluid additives. In the paper industry, pneumatic conveyors are used to move bentonite from processing plants to paper mills, where it is used as a filler or coating agent. Additionally, in the environmental industry, bentonite pneumatic systems are utilized for transporting bentonite to remediation sites, where it is applied to contaminated soil to immobilize pollutants. The ability to handle fine powders and maintain product quality makes pneumatic conveying an ideal choice for these applications.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of bulk material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of various industries. HeadPowder's expertise lies in understanding the unique properties of materials like bentonite and developing systems that ensure efficient, reliable, and cost-effective transportation. The company's facilities are located in Shandong, China, where it leverages advanced technology and skilled personnel to deliver high-performance solutions to global clients. By combining industry knowledge with customer-centric approaches, HeadPowder aims to enhance operational efficiency and product quality for its clients in the bulk material handling sector.