

What is a Rare Earth Mineral Powder Material Handling System Equipment? What is its Design Principle
For industries dealing with rare earth mineral powders, efficient and reliable material handling systems are crucial for maintaining production efficiency and product quality. This article explores the Rare Earth Mineral Powder Material Handling System Equipment, detailing its components, operational principles, and design considerations to help professionals in the field understand its functionality and importance.

Introduction to Rare Earth Mineral Powder Material Handling Systems
Rare earth minerals are critical components in modern technology, including electronics, renewable energy, and advanced manufacturing. The processing of these minerals often involves handling fine powders, which require specialized equipment to ensure safe and efficient transport. A Rare Earth Mineral Powder Material Handling System is designed to address the unique challenges of transporting these powders, such as their fine particle size, potential for dust generation, and the need for contamination control.
Key Components of the Material Handling System
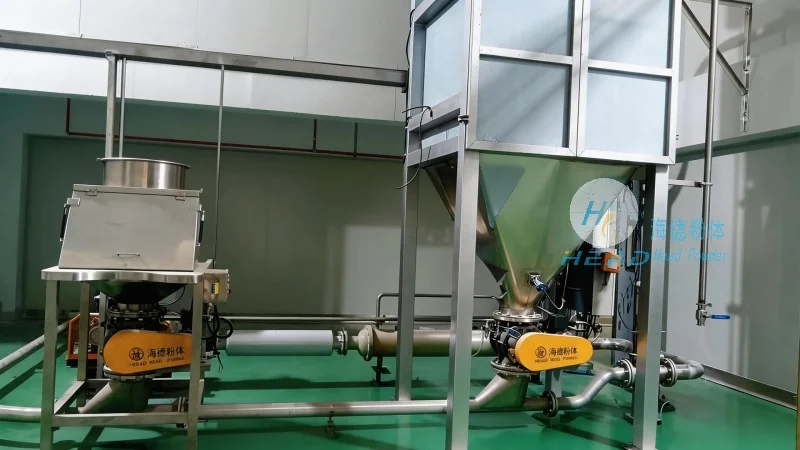
The system typically consists of several interconnected components that work together to move and process the rare earth mineral powders. These components may include feeders, conveyors, storage silos, and control systems. Each component is engineered to handle the specific characteristics of the powders, ensuring minimal loss, low dust emission, and consistent flow rates.
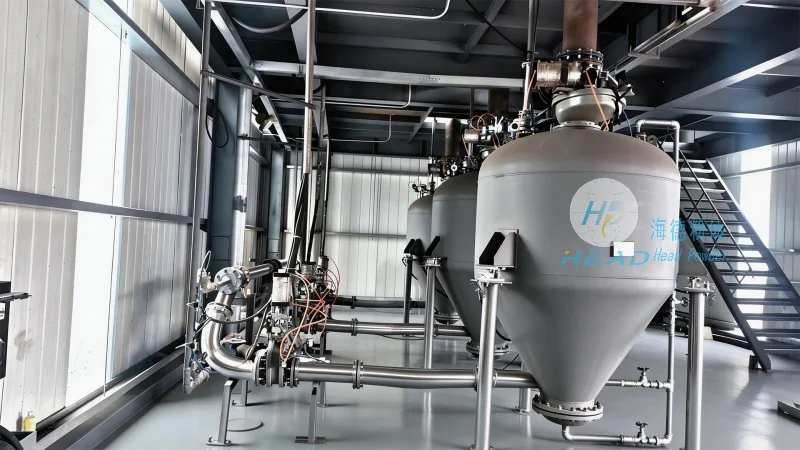
Feeding equipment, such as rotary valves or vibratory feeders, is used to regulate the flow of the powder from the storage silo to the conveyor system. The conveyor system, often a belt or screw conveyor, transports the powder to the processing or packaging area. Storage silos are designed with aeration systems to prevent caking and maintain the powder's flowability. Control systems, including sensors and automation software, monitor the system's performance and adjust parameters as needed to optimize operation.
Design Principles for Efficient Material Handling
The design of a Rare Earth Mineral Powder Material Handling System follows several key principles to ensure effectiveness and safety. First, the system must be designed to minimize dust generation and control airborne particles, as rare earth powders can be hazardous if inhaled. This is achieved through enclosed systems, proper sealing, and dust collection mechanisms. Second, the equipment must be constructed from materials that are resistant to corrosion and wear, as the powders may be abrasive or chemically reactive.
Third, the system is designed for scalability and adaptability, allowing it to accommodate changes in production volume or powder characteristics. This flexibility is crucial for industries where demand fluctuates or where new processing techniques are introduced. Additionally, the design emphasizes energy efficiency and low maintenance requirements to reduce operational costs over the system's lifespan.
Operational Considerations and Safety Measures
When operating a Rare Earth Mineral Powder Material Handling System, several considerations are essential to ensure safe and efficient performance. Regular maintenance is critical to prevent equipment failure and maintain optimal performance. This includes cleaning the system to remove accumulated powder, inspecting conveyor belts and bearings, and checking the integrity of seals and ductwork.
Proper training for operators is also vital, as they need to understand the system's controls and emergency procedures. Safety measures, such as dust suppression systems and personal protective equipment (PPE), are implemented to protect both the equipment and personnel from the hazards associated with handling fine powders. The system is designed to comply with relevant safety standards and regulations, ensuring that it operates within legal and industry guidelines.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing high-quality material handling systems for various industries, including rare earth processing. With a focus on innovation and customer satisfaction, the company provides tailored solutions that meet the specific needs of its clients. HeadPowder's expertise in material handling technology ensures that their systems are reliable, efficient, and compliant with industry standards. The company's headquarters is located in Shandong, China, where it continues to develop advanced solutions for the global market.