

[Coffee Material Conveying: Working Principles and Features]
Coffee material conveying systems are integral to the efficiency and reliability of coffee processing operations. These systems ensure that raw coffee beans, as well as intermediate and finished products, are transported smoothly and safely from one stage of production to another. Understanding the working principles and key characteristics of such systems is crucial for optimizing workflow and maintaining product quality in coffee manufacturing facilities.

Working Principles of Coffee Material Conveying Systems
The core working principle of coffee material conveying systems revolves around the efficient movement of coffee materials through various stages of processing. These systems typically utilize a combination of mechanical components, such as belts, chains, or screw conveyors, to transport coffee beans and related products. The process begins with the loading of raw coffee beans into the system, where they are then moved through a series of stages including cleaning, sorting, roasting, and packaging. Each stage is designed to handle specific tasks, and the conveying system ensures that materials are transferred seamlessly between these stages without interruption. For instance, in the cleaning stage, the conveyor may incorporate a series of screens or brushes to remove impurities like stones, dust, or debris from the raw beans. This ensures that only high-quality beans proceed to the next stage. Similarly, during the sorting phase, the conveyor may use air jets or optical sensors to separate beans of different sizes, colors, or grades, allowing for precise classification based on quality standards.

Key components of coffee material conveying systems include feeders, conveyors, and control mechanisms. Feeders are responsible for evenly distributing the coffee material into the conveyor, ensuring consistent flow. Conveyors, which may be belt, chain, or screw types, provide the primary means of transporting the material. Control mechanisms, often automated, regulate the speed and direction of the conveyor, adapting to the needs of different processing stages. For example, during the roasting phase, the conveyor may adjust its speed to accommodate the increased temperature and material characteristics, ensuring uniform roasting and preventing overheating or under-roasting. Additionally, sensors are integrated into the system to monitor the material flow and detect any blockages or irregularities, triggering alarms or automatic adjustments to maintain optimal operation.
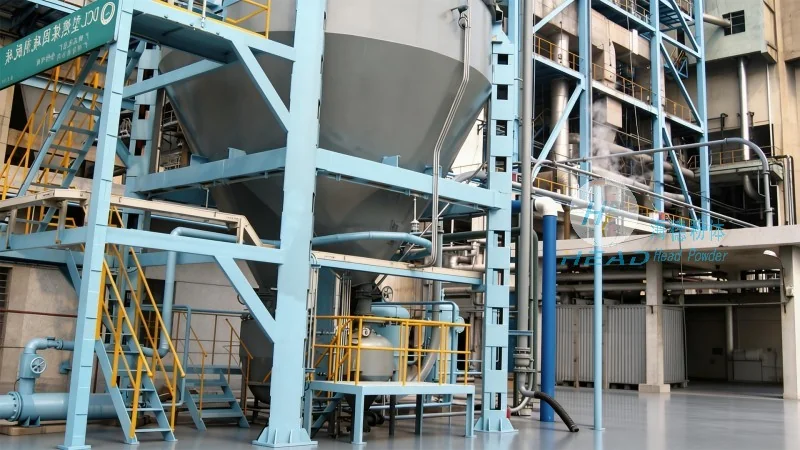
Key Characteristics of Coffee Material Conveying Systems
Coffee material conveying systems are characterized by several important features that enhance their performance and suitability for coffee processing applications. One of the primary characteristics is their ability to handle a wide range of coffee materials, from raw green beans to roasted and ground coffee. This versatility allows the system to support multiple stages of coffee production, from initial raw material handling to final product packaging. Another key characteristic is their durability and resistance to the harsh conditions of coffee processing, such as high temperatures, moisture, and the presence of oils and acids. Materials used in the construction of these systems, such as stainless steel and corrosion-resistant alloys, ensure long-term reliability and minimal maintenance. Furthermore, the systems are designed with hygienic standards in mind, featuring smooth surfaces and easy-to-clean components to prevent contamination and ensure compliance with food safety regulations.