

Working Principle and Features of Fine Chemical Powder Pneumatic Conveying Equipment
For industries dealing with fine chemicals, the efficient and reliable transportation of powders is a critical operational requirement. The fine chemical powder pneumatic conveying equipment, developed by Shandong HeadPowder Engineering Co., Ltd., offers a sophisticated solution to this challenge. This equipment is designed to handle the unique characteristics of fine chemical powders, ensuring safe, clean, and efficient material transfer. This article explores the working principle and key features of this advanced pneumatic conveying system.

Understanding the Working Principle of Fine Chemical Powder Pneumatic Conveying Equipment
The core of the fine chemical powder pneumatic conveying system lies in its ability to use air as the conveying medium. The system typically operates through two primary modes: suction (or vacuum) and pressure. In the suction mode, a vacuum is created at the material inlet, drawing the powder into the conveying line. The air and powder mixture then travels through the pipeline to a separation unit where the powder is discharged and the air is filtered or recycled. The pressure mode, conversely, uses compressed air to push the powder through the system. Both modes rely on precise control of air flow, pressure, and velocity to maintain the optimal transport conditions for fine powders.
Key components of the system include the material hopper, which holds the fine chemical powder; the air compressor or vacuum pump, which provides the necessary air pressure or vacuum; the conveying line, which transports the powder; and the separation and collection equipment, such as cyclones or filters, which separate the powder from the air. The system is designed to handle powders with varying particle sizes, densities, and flow properties, ensuring consistent performance across different applications.

Key Features of Fine Chemical Powder Pneumatic Conveying Equipment
One of the most significant advantages of this equipment is its ability to provide a clean and dust-free transfer process. Unlike mechanical conveyors, which can generate dust and cause contamination, pneumatic systems enclose the powder in an air stream, minimizing environmental impact and product contamination. This is particularly important for fine chemicals, where purity is paramount.
Efficiency is another key feature. The system can transport powders over long distances with minimal energy consumption, making it a cost-effective solution for large-scale operations. Additionally, the flexibility of the system allows for easy integration into existing production lines, with the ability to change conveying routes or adjust flow rates as needed. The equipment also offers high reliability, with advanced controls that monitor and adjust system parameters in real-time to maintain optimal performance.
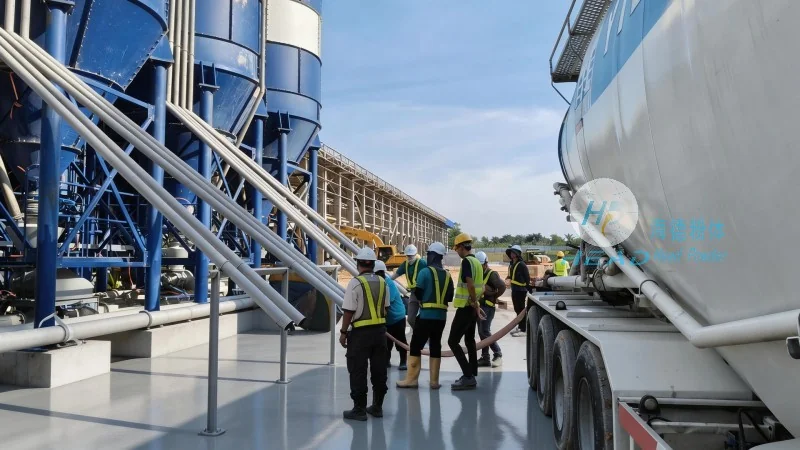
Another notable feature is the system's ability to handle a wide range of powder characteristics. Whether dealing with abrasive, hygroscopic, or temperature-sensitive powders, the fine chemical powder pneumatic conveying equipment is designed to accommodate these challenges. The use of specialized materials for the conveying line and components ensures durability and resistance to corrosion or wear, extending the equipment's service life.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of advanced powder handling equipment. With a strong presence in China, particularly in Shandong, the company specializes in developing customized solutions for the fine chemical industry. The company's commitment to innovation and quality has made it a trusted partner for businesses seeking reliable and efficient powder conveying systems. By leveraging years of experience and expertise, headpowder provides equipment that meets the stringent requirements of modern fine chemical production, ensuring safety, efficiency, and product integrity.