

Working Principle and Features of a Sulfur Powder Material Pneumatic Conveying System
For industrial applications involving the handling of sulfur powder, efficient and reliable material transport is crucial. A pneumatic conveying system offers a sophisticated solution to move sulfur powder from one location to another within a processing facility. This article explores the working principle and key features of such a system, providing insights into its operational mechanics and advantages.
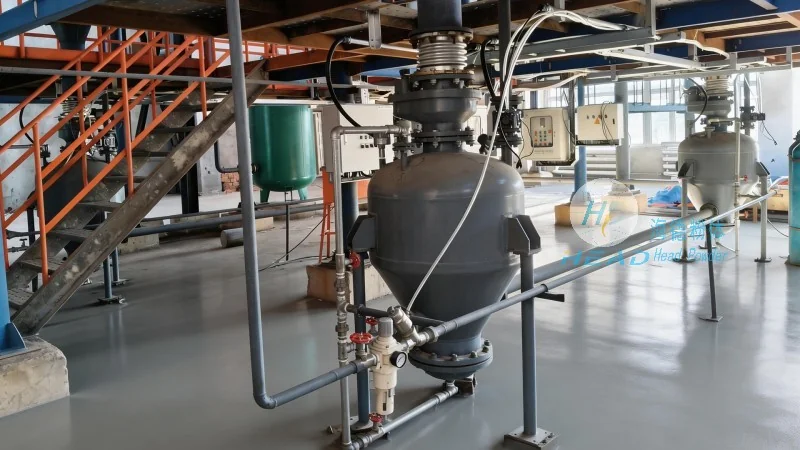
Overview of Sulfur Powder Pneumatic Conveying Systems
A pneumatic conveying system for sulfur powder is designed to transport dry powder materials through a pipeline using air or other gases as the conveying medium. The system typically consists of several components, including a material feed hopper, a conveying line, a control valve, and a discharge device. The primary goal is to move sulfur powder from a storage or processing point to a destination such as a silo, reactor, or packaging unit without the need for mechanical components like belts or buckets.

Working Principle of the Sulfur Powder Pneumatic Conveying System
The operation of a sulfur powder pneumatic conveying system relies on the principle of fluidization and suspension. The system uses a blower or compressor to generate airflow within the pipeline. As air flows through the conveying line, it creates a low-pressure zone that draws sulfur powder from the feed hopper into the pipeline. The powder particles are then suspended in the air stream and transported to the discharge point. The velocity of the air is carefully controlled to ensure that the powder remains suspended without settling or clogging the pipeline. The system may use either positive pressure (where air is forced into the pipeline) or negative pressure (where air is drawn out), depending on the specific application and layout of the facility.

Key Features and Advantages of the System
Several key features distinguish a sulfur powder pneumatic conveying system from other material handling methods. Firstly, it offers a completely enclosed and dust-free operation, which is essential for handling sulfur powder to prevent environmental contamination and ensure worker safety. Secondly, the system provides high efficiency in terms of material transport, with minimal material loss and reduced maintenance compared to traditional methods like bucket elevators or screw conveyors. Additionally, the system can handle varying particle sizes and moisture content of sulfur powder, making it versatile for different industrial processes. The modular design of the system allows for easy integration into existing facilities and scalability to accommodate increased production demands. Another notable feature is the ability to control the flow rate and pressure precisely, enabling accurate dosing and process control. This level of control is critical in applications where the sulfur powder is used as a raw material in chemical reactions or manufacturing processes.
Application Scenarios and Operational Considerations
Sulfur powder pneumatic conveying systems are widely used in various industries, including chemical manufacturing, fertilizer production, and pharmaceutical processing. In chemical plants, the system is often employed to transport sulfur powder to reactors for the production of sulfuric acid or other sulfur-based compounds. In fertilizer plants, it helps move sulfur powder to mixing and blending units, ensuring uniform distribution of the nutrient. The operational considerations for such a system include proper maintenance of the air compressor and pipeline to prevent blockages, regular cleaning of the system to avoid powder accumulation, and monitoring of air pressure and flow rates to maintain optimal performance. The system's design also needs to account for the potential for sulfur powder to be abrasive or corrosive, requiring materials like stainless steel or special coatings for the pipeline and components to ensure durability and longevity.

Conclusion and Company Information
In conclusion, a sulfur powder pneumatic conveying system is an efficient and reliable solution for transporting dry powder materials in industrial settings. Its working principle, based on fluidization and suspension, allows for safe and effective movement of sulfur powder while offering several advantages such as enclosed operation, high efficiency, and versatility. For companies seeking to implement such a system, Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions tailored to specific industrial needs. With a focus on quality and performance, the company's expertise in pneumatic conveying systems ensures that clients receive robust and reliable equipment for their sulfur powder handling requirements. Based in Shandong, China, HeadPowder Engineering Co., Ltd. is committed to delivering innovative and efficient material handling solutions that meet the demands of modern industrial operations.