

Principle and Working Scene Characteristics of Feather Powder Conveying Systems
Feather powder conveying systems are specialized equipment designed to handle and transport fine powders, such as those derived from feather processing. These systems are engineered to ensure efficient, reliable, and safe material handling in various industrial applications. Understanding the underlying principles and typical working scenarios of these systems is crucial for optimizing operational efficiency and maintaining product quality.

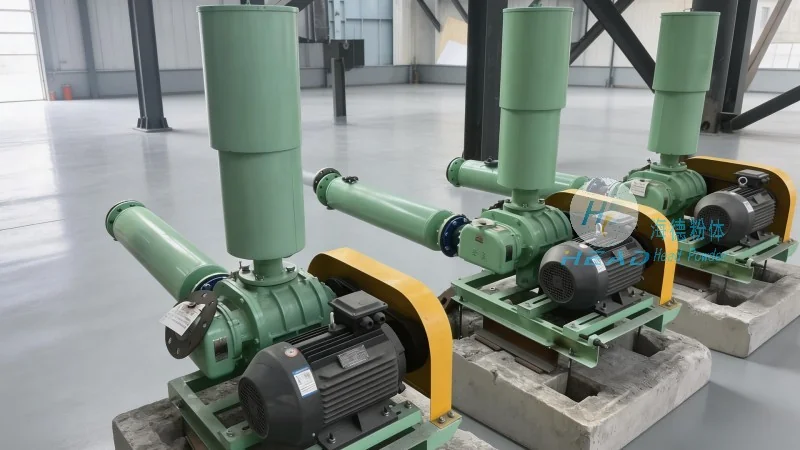
Principle of Feather Powder Conveying Systems
The core principle of feather powder conveying systems revolves around the use of air or mechanical forces to move fine powders through a pipeline or conveyor. The system typically comprises a hopper for material storage, a conveying mechanism (either pneumatic or mechanical), and a control unit to regulate the flow. Pneumatic conveying systems, for instance, utilize compressed air to create a pressure differential that propels the powder particles through the system. This method is particularly effective for handling delicate or abrasive powders, as it minimizes mechanical wear and prevents contamination. Mechanical conveying systems, on the other hand, rely on rotating components like screws or belts to transport the material. Both approaches aim to achieve consistent flow rates and maintain the integrity of the powder, ensuring that it reaches its destination without degradation or loss.

Working Scene Characteristics of Feather Powder Conveying Systems
Feather powder conveying systems are deployed in diverse industrial settings, each with unique characteristics that influence system design and operation. One common application is in the poultry processing industry, where these systems are used to transport feather meal or other feather-derived powders from processing facilities to storage or packaging areas. In such scenarios, the system must handle high volumes of fine material while maintaining low dust emissions, as feather powders can be lightweight and prone to dispersion. Another working scene is in the feed manufacturing sector, where feather powder is blended with other ingredients to produce animal feed. Here, the conveying system needs to integrate seamlessly with existing production lines, ensuring precise dosing and consistent mixing. Additionally, in research and development laboratories, these systems are used for small-scale testing and quality control, requiring high precision and minimal material waste. Each working scene demands specific considerations, such as the need for dust suppression, material handling speed, and compatibility with other equipment, making the design of feather powder conveying systems highly tailored to the application.

About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer specializing in the design, development, and supply of advanced powder handling solutions. With a strong focus on innovation and customer-centric approaches, the company has established itself as a trusted partner in the industrial sector. HeadPowder's expertise lies in creating customized conveying systems that address the unique challenges of handling fine powders, including feather-based materials. The company's facilities are located in Shandong, China, where it leverages local resources and industry knowledge to deliver high-quality products and services. By combining technical expertise with practical experience, HeadPowder ensures that its systems meet the stringent requirements of modern industrial operations, contributing to enhanced productivity and operational reliability for clients worldwide.