

Principle and Working Scene Characteristics of Positive and Negative Pressure Mixed Powder Conveying
Positive and negative pressure mixed powder conveying machines represent a sophisticated solution in the field of powder handling technology, designed to efficiently transport bulk powders over long distances with minimal energy consumption and operational complexity. This article delves into the fundamental principles behind these machines and explores the specific working scenarios where their application is most advantageous.

Company Introduction
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the powder processing industry, specializes in the design, development, and production of advanced powder conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable solutions for their powder handling needs. HeadPowder's facilities are located in Shandong, China, where state-of-the-art technology and rigorous quality control ensure the delivery of high-performance equipment tailored to diverse industrial requirements.
Principle of Positive and Negative Pressure Mixed Powder Conveying
The core principle of a positive and negative pressure mixed powder conveying system involves the integration of both positive and negative pressure zones within a single conveying line. This hybrid approach allows for the simultaneous operation of suction and pressure components, enabling the efficient movement of powders from a source to a destination. The system typically consists of a suction section that draws powders from the source, a mixing zone where the powders are combined with air or other carrier gases, and a pressure section that propels the mixture to the discharge point. By leveraging the combined effects of suction and pressure, these machines achieve higher conveying capacities and lower energy costs compared to traditional systems that rely solely on positive or negative pressure.
Working Scene Characteristics
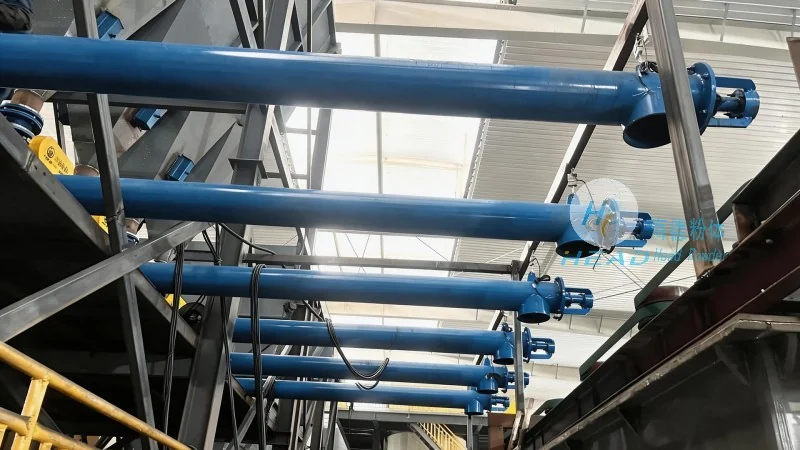
The application of positive and negative pressure mixed powder conveying machines is particularly suited to industrial environments where the transportation of bulk powders over extended distances is required. These machines are commonly employed in sectors such as pharmaceuticals, food processing, chemical manufacturing, and mining, where the need for precise control over powder flow, minimal product contamination, and energy efficiency is paramount. The working scene characteristics include:
Long-Distance Conveying
One of the key advantages of these machines is their ability to transport powders over long distances, often exceeding 100 meters, without the need for intermediate transfer points. This capability is crucial in large-scale production facilities where raw materials or finished products need to be moved between different processing stages or storage areas. The hybrid pressure system ensures consistent flow rates and pressure stability, minimizing the risk of material degradation or blockages during long-distance transport.

Multi-Point Discharge
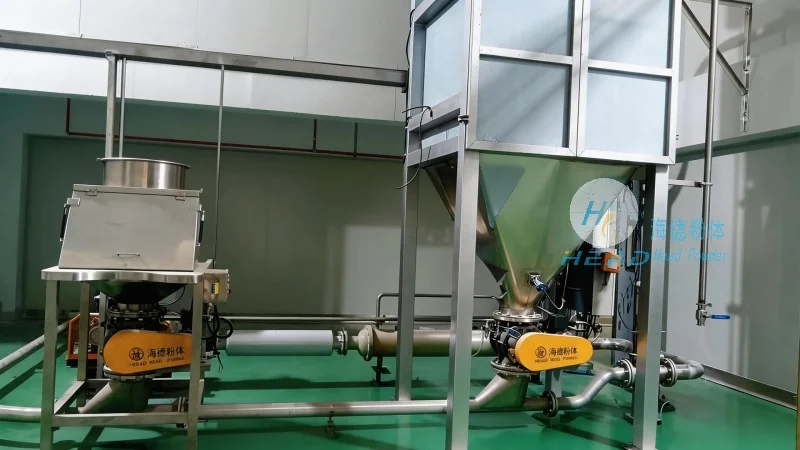
Another significant characteristic is the capability to discharge powders to multiple destinations simultaneously. By integrating multiple discharge points into the conveying line, these machines can serve several processing units or storage silos from a single source. This flexibility enhances operational efficiency and reduces the need for additional equipment, making them ideal for complex production lines where multiple outputs are required.
Low Energy Consumption
Compared to traditional positive pressure or vacuum systems, the mixed pressure approach significantly reduces energy consumption. The suction section operates at lower pressure levels, while the pressure section utilizes the remaining energy to propel the mixture. This optimization results in lower operational costs and a smaller environmental footprint, aligning with modern sustainability goals in industrial operations.
Reduced Product Contamination
The design of positive and negative pressure mixed conveying systems minimizes the risk of product contamination. The sealed conveying line prevents the ingress of external contaminants, while the controlled air flow ensures that the powders remain within the system without exposure to external elements. This is particularly important in industries such as pharmaceuticals and food processing, where product purity is non-negotiable.
Conclusion
Positive and negative pressure mixed powder conveying machines offer a versatile and efficient solution for the transportation of bulk powders in various industrial applications. By combining the benefits of both positive and negative pressure systems, these machines provide superior performance in terms of conveying capacity, energy efficiency, and operational flexibility. As a leading manufacturer, Shandong HeadPowder Engineering Co., Ltd. continues to innovate in this field, delivering high-quality equipment that meets the evolving needs of modern industries. The working scene characteristics, including long-distance conveying, multi-point discharge, low energy consumption, and reduced product contamination, make these machines an indispensable asset for businesses seeking reliable and cost-effective powder handling solutions.