

Principle and Working Scene Characteristics of Air-Driven Material Conveyor for Edible Salt
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling systems. Among their portfolio is the air-driven material conveyor line, a critical solution for efficiently transporting edible salt and other bulk materials in industrial settings. This article explores the fundamental principles behind such systems and highlights the key characteristics of their working environments.
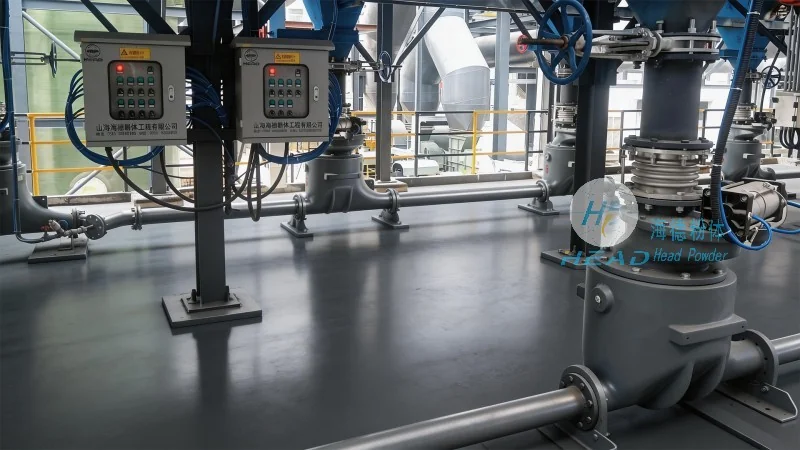
Understanding the Core Principle of Air-Driven Material Conveyors
The air-driven material conveyor, also known as pneumatic conveying, operates by using compressed air or a vacuum to move bulk materials through a pipeline. For edible salt, this method offers several advantages over traditional mechanical systems. The process typically involves a hopper where the salt is stored, a feeder that controls the flow rate, and a pipeline that transports the material to its destination. The air pressure or vacuum creates a flow that carries the salt particles, ensuring a smooth and continuous transfer. This principle is based on the principle of fluid dynamics, where the air acts as a medium to transport the solid material. The system can be configured in either positive pressure or negative pressure modes, depending on the application requirements. Positive pressure systems use compressed air to push the material forward, while negative pressure systems use a vacuum to pull the material through the line. Both methods are effective for edible salt, but the choice depends on factors like material characteristics, distance, and system complexity.

Key Working Scene Characteristics of Edible Salt Air-Driven Conveyors
The working environment of an edible salt air-driven conveyor is tailored to meet the specific needs of food processing industries. These systems are designed to maintain strict hygiene standards, as edible salt is a food product that requires contamination-free handling. The conveyor components are typically made from stainless steel or other food-grade materials, ensuring durability and compliance with food safety regulations. The system is also equipped with filters and cleaning mechanisms to prevent dust and particles from escaping into the environment, which is crucial for maintaining a clean and safe workspace. Another important characteristic is the scalability of the system. HeadPowder’s solutions can be customized to handle different production volumes, from small-scale operations to large industrial plants. This flexibility allows manufacturers to adapt the conveyor line to their changing production needs without significant modifications. The working scene also includes integration with other processing equipment, such as mixing tanks, packaging machines, and storage silos. The conveyor line acts as a central link, connecting these components and ensuring a seamless flow of materials throughout the production process. Additionally, the system is designed for energy efficiency, with adjustable air pressure settings that minimize energy consumption while maintaining optimal performance. This not only reduces operational costs but also aligns with modern sustainability goals in the food industry.

Application Scenarios and Operational Efficiency
Edible salt air-driven conveyor lines are widely used in various industrial applications within the food processing sector. One common scenario is in salt production facilities, where the conveyor line transports raw salt from storage silos to processing units, such as grinding or packaging stations. The system’s ability to handle large volumes of salt efficiently reduces labor costs and improves production throughput. Another application is in food processing plants, where the conveyor line is used to transport salt to mixing lines for seasoning or preservation processes. The precise control over the flow rate ensures consistent product quality, which is essential for meeting regulatory standards. Furthermore, the system is suitable for use in environments where space is limited, as the pneumatic conveyor can be installed in a compact configuration without the need for extensive infrastructure. This makes it an ideal solution for modern food processing facilities that prioritize space optimization. The operational efficiency of the air-driven conveyor is enhanced by its low maintenance requirements. Unlike mechanical systems that require regular lubrication and part replacement, the pneumatic system has fewer moving parts, reducing the risk of breakdowns and minimizing downtime. HeadPowder’s engineering team ensures that the conveyor line is designed with reliability in mind, incorporating features like automatic shut-off valves and pressure sensors to prevent overloading and ensure safe operation. These features contribute to a longer service life and lower long-term operational costs for the end-user.

Conclusion and Company Expertise
In conclusion, the air-driven material conveyor line for edible salt is a sophisticated and efficient solution that addresses the unique challenges of bulk material handling in the food industry. By leveraging the principles of pneumatic conveying, these systems offer advantages such as hygiene compliance, scalability, and energy efficiency. HeadPowder, with its headquarters in Shandong, China, has established itself as a trusted provider of such engineering solutions, delivering customized systems that meet the specific needs of their clients. The company’s expertise in material handling technology ensures that the conveyor lines are designed to operate reliably and effectively, contributing to improved productivity and cost savings for food processing businesses. As the demand for efficient and safe material handling continues to grow, HeadPowder remains at the forefront of innovation, providing advanced solutions that meet the evolving needs of the industry.