

Operation Process and Working Principle of Intelligent Tonne Bag Feeding Station Material Conveying
Intelligent tonne bag feeding stations equipped with material conveying lines represent a sophisticated solution in modern industrial material handling. These systems are designed to efficiently manage the transfer of bulk materials from tonne bags into processing equipment, ensuring seamless and automated operations. The integration of advanced technology in these lines enhances productivity, reduces labor costs, and minimizes material loss during the transfer process. For industries dealing with large volumes of bulk materials, such as chemicals, food, and construction materials, the intelligent tonne bag feeding station material conveying line is a critical component of their material handling infrastructure.

Key Components and Structure of the Material Conveying Line
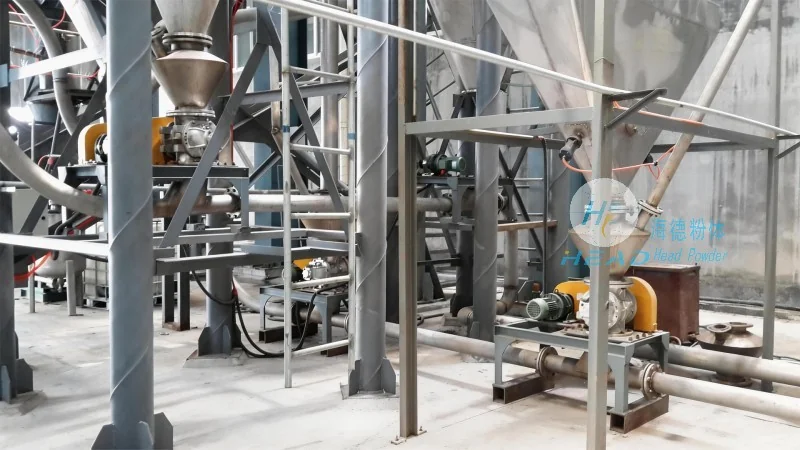
The intelligent tonne bag feeding station material conveying line typically consists of several key components that work in concert to achieve efficient material transfer. The primary components include a tonne bag opening mechanism, a hopper or receiving container, a conveyor system (such as a screw conveyor or belt conveyor), and a control system. The tonne bag opening mechanism is responsible for safely and efficiently opening the bag to release the material inside. This is often achieved through mechanical or pneumatic systems that cut or tear the bag open without damaging the material. The hopper or receiving container then collects the material from the opened bag and funnels it into the conveyor system. The conveyor system transports the material from the hopper to the processing equipment, such as a mixer, grinder, or storage silo. The control system monitors and regulates the entire process, ensuring that the material flow is consistent and that the system operates within safe parameters. Each component is carefully designed and integrated to ensure smooth operation and minimal downtime.
Operation Process of the Material Conveying Line
The operation of the intelligent tonne bag feeding station material conveying line follows a systematic sequence of steps. The process begins with the placement of a tonne bag onto the feeding station. The system then automatically identifies the bag and initiates the opening mechanism. Once the bag is opened, the material inside is released into the hopper. The control system then activates the conveyor system, which starts moving the material from the hopper to the processing equipment. The speed of the conveyor can be adjusted based on the material characteristics and processing requirements. For example, if the material is fine and powdery, a slower conveyor speed may be used to prevent material spillage or blockages. The system continuously monitors the material level in the hopper and adjusts the conveyor speed accordingly to maintain a steady flow. When the tonne bag is empty, the system automatically stops the conveyor and signals the operator to replace the bag. This automated process significantly reduces the need for manual intervention, improving safety and efficiency. The entire operation is designed to be user-friendly and reliable, ensuring that the material handling process is consistent and repeatable.

Working Principle of the Material Conveying Line
The working principle of the intelligent tonne bag feeding station material conveying line is based on the principles of mechanical and pneumatic systems. The core of the system is the material transfer mechanism, which converts the vertical or horizontal movement of the material into a controlled flow. The tonne bag opening mechanism uses mechanical force or pneumatic pressure to cut or tear the bag open, allowing the material to flow into the hopper. The hopper acts as a buffer, collecting the material and preventing it from spilling or causing blockages. The conveyor system then uses a rotating screw or belt to move the material forward. The screw conveyor, for instance, has a helical screw that rotates and pushes the material along the conveyor path. The speed of the screw rotation determines the material flow rate. The belt conveyor uses a moving belt that carries the material from the hopper to the processing equipment. The control system uses sensors and feedback mechanisms to monitor the material level, conveyor speed, and system status. This feedback loop ensures that the system operates optimally and that any issues are detected and addressed promptly. The integration of sensors and automation technology allows for real-time monitoring and adjustment, enhancing the overall performance and reliability of the material conveying line.

Advantages of the Intelligent Tonne Bag Feeding Station Material Conveying Line
The intelligent tonne bag feeding station material conveying line offers several advantages over traditional manual material handling methods. Firstly, it significantly improves operational efficiency by automating the entire process. The system can handle multiple tonne bags simultaneously, reducing the time required for material transfer. This leads to increased production throughput and reduced downtime. Secondly, the system enhances safety by minimizing the need for manual handling of heavy and bulky tonne bags. The automated opening and conveying mechanisms reduce the risk of injury to operators. Thirdly, the system improves material quality by preventing contamination and loss. The enclosed design of the conveying line prevents dust and other contaminants from entering the material, ensuring that the processed material meets quality standards. Fourthly, the system provides cost savings by reducing labor costs and minimizing material waste. The automated process reduces the need for manual labor, and the efficient transfer reduces material spillage and loss. Finally, the system offers flexibility and adaptability. The conveyor speed and other parameters can be adjusted to accommodate different material types and processing requirements. This makes the system suitable for a wide range of industrial applications.
Application Scenarios and Industries
The intelligent tonne bag feeding station material conveying line is widely used in various industries that handle bulk materials. Some of the key application scenarios include chemical manufacturing, where the system is used to transfer raw materials such as powders and granules into reactors and mixers. In the food industry, the system is used to handle food-grade materials, ensuring that the material is transferred hygienically and without contamination. In the construction industry, the system is used to transfer cement, sand, and other building materials into mixers and storage silos. The system is also used in the pharmaceutical industry to transfer raw materials into processing equipment, ensuring that the material is handled under sterile conditions. The versatility of the intelligent tonne bag feeding station material conveying line makes it suitable for a wide range of industrial applications, from small-scale operations to large-scale manufacturing plants.
Conclusion and Company Overview
In conclusion, the intelligent tonne bag feeding station material conveying line is a highly efficient and reliable solution for bulk material handling. The system combines advanced technology with automation to ensure smooth and consistent material transfer, improving productivity and reducing costs. The key components and operation process of the system are designed to meet the demands of modern industrial applications, providing a robust and durable solution for material handling. For companies looking to enhance their material handling capabilities, the intelligent tonne bag feeding station material conveying line is an excellent choice. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality material handling systems that meet the specific needs of their clients. With years of experience and a commitment to quality, HeadPowder provides reliable and efficient solutions for bulk material handling, helping companies to improve their operations and achieve their business goals. Based in Shandong, China, HeadPowder serves clients worldwide, delivering innovative and cost-effective solutions for material handling challenges.