

Principles and Application Scenarios of Fully Automatic Bulk Powder Unpacking and Conveying Systems
In the modern industrial landscape, the efficient handling of bulk powders is a critical requirement across various sectors, including pharmaceuticals, food processing, and chemical manufacturing. The fully automatic bulk powder unpacking and conveying system represents a sophisticated solution designed to streamline the entire process from raw material reception to internal storage or direct processing. This system integrates advanced technologies to automate the unpacking, weighing, and transport of powders, ensuring precision, safety, and operational efficiency. As a key component in material handling, such systems are essential for maintaining consistent product quality and optimizing production workflows. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, this system exemplifies the company's commitment to innovation and customer-centric design.

Core Principles of the Fully Automatic Bulk Powder Unpacking and Conveying System
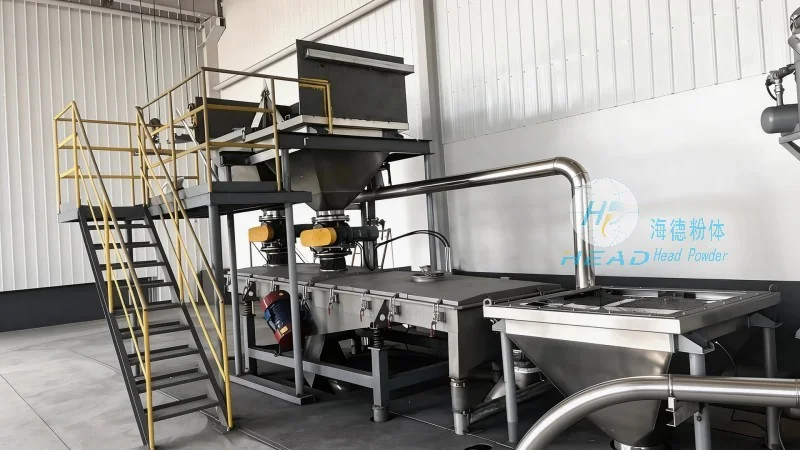
The fundamental principle of this system revolves around the seamless integration of multiple automated processes. At its heart, the system employs a combination of mechanical, pneumatic, and electronic components to handle the entire workflow. The process typically begins with the reception of bulk powder bags or containers. The system then uses automated mechanisms to open the packaging, such as bag openers or container lifting devices, ensuring that the powder is released without manual intervention. Subsequently, the system incorporates precise weighing scales to measure the exact quantity of material, which is crucial for inventory management and compliance with regulatory standards. The weighing data is then processed and recorded, providing real-time insights into material usage and stock levels.
Following the weighing step, the system transitions to the conveying phase. Advanced conveying technologies, including screw conveyors, pneumatic transport systems, or belt conveyors, are employed to transport the powder from the weighing station to the desired destination. The choice of conveying method depends on the properties of the powder, such as its flowability, moisture content, and potential for dust generation. For example, screw conveyors are ideal for free-flowing powders, while pneumatic systems are suitable for dusty or fine powders that require containment. The system also includes sensors and control mechanisms to monitor the conveying process, ensuring that the material is transported at the correct speed and volume. This automation minimizes human error and enhances the overall reliability of the operation.
Key Features and Technical Advantages
The fully automatic bulk powder unpacking and conveying system offers several key features that set it apart from traditional manual or semi-automated methods. One of the primary advantages is the significant reduction in labor requirements. By automating the entire unpacking and conveying process, the system eliminates the need for manual handling, which not only reduces operational costs but also minimizes the risk of workplace injuries associated with lifting heavy bags or containers. Additionally, the system enhances safety by reducing exposure to dust and other airborne particles, as the entire process is contained within a sealed environment.
Another critical feature is the high level of precision and accuracy. The integrated weighing scales provide precise measurements, ensuring that the correct amount of powder is used in each batch. This precision is essential in industries like pharmaceuticals, where even minor variations in dosage can have significant implications for product quality and safety. The system also includes data logging and reporting capabilities, allowing for real-time monitoring of material flow and inventory levels. This data can be used to optimize production schedules, identify bottlenecks, and improve overall operational efficiency.
Furthermore, the system is designed for flexibility and adaptability. It can accommodate various types of packaging, including bags, drums, and containers, making it suitable for a wide range of applications. The modular design allows for easy integration with existing production lines and can be scaled to meet the changing needs of the facility. The system also incorporates advanced control systems, such as PLC (Programmable Logic Controllers), which enable remote monitoring and control, further enhancing operational flexibility.

Application Scenarios and Industry Use Cases
The fully automatic bulk powder unpacking and conveying system finds extensive application across multiple industries, each with specific requirements for material handling. In the pharmaceutical industry, for instance, the system is used to handle active pharmaceutical ingredients (APIs) and excipients with high precision and strict contamination control. The automated process ensures that the powders are handled in a sterile environment, minimizing the risk of cross-contamination and maintaining product integrity. The system's ability to measure and record exact quantities is particularly valuable in pharmaceutical manufacturing, where batch consistency is paramount.
In the food processing industry, the system is employed to handle ingredients such as flour, sugar, and spices. The automated unpacking and conveying process ensures that the ingredients are handled hygienically and efficiently, reducing the risk of contamination and improving production throughput. The system's flexibility allows it to handle different types of packaging, including bulk bags and containers, which are commonly used in food processing facilities. The precise weighing and conveying capabilities also help in maintaining consistent product quality, which is crucial for meeting regulatory standards and consumer expectations.
In the chemical manufacturing sector, the system is used to handle a wide range of powders, including raw materials and intermediates. The system's ability to handle dusty and potentially hazardous powders is particularly important in this industry. The sealed and automated process minimizes the risk of exposure to harmful substances, enhancing workplace safety. The system's precision in weighing and conveying also helps in maintaining the quality of the final product, as even small variations in the raw material can affect the chemical properties of the end product.

Additionally, the system is used in the agricultural sector for handling fertilizers and other agricultural inputs. The automated process ensures that the fertilizers are handled efficiently and safely, reducing the risk of spills and contamination. The system's ability to handle large quantities of material makes it suitable for agricultural applications, where bulk handling is common. The precise weighing and conveying capabilities also help in optimizing the application of fertilizers, ensuring that the correct amount is used for each crop.
Conclusion and Future Trends
The fully automatic bulk powder unpacking and conveying system represents a significant advancement in material handling technology, offering numerous benefits to industries that rely on bulk powders. By automating the entire process, the system enhances efficiency, reduces labor costs, and improves product quality and safety. As technology continues to evolve, we can expect further innovations in this field, such as the integration of artificial intelligence and machine learning to optimize the system's performance and adapt to changing production needs. The system's adaptability and flexibility make it a valuable asset for modern industrial operations, and its continued development will likely play a crucial role in the future of material handling. Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of this technological advancement, dedicated to providing cutting-edge solutions that meet the evolving needs of industries worldwide.