

What is a Negative Pressure Suction Material Handling Equipment? What are its Design Principles?
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced material handling solutions. This article delves into the concept of negative pressure suction equipment and its underlying design principles, offering a comprehensive overview for industry professionals and potential clients.

Understanding Negative Pressure Suction Material Handling Equipment
Negative pressure suction material handling equipment is a sophisticated system designed to transport bulk materials through a pipeline using a vacuum or negative pressure environment. Unlike traditional positive pressure systems that force material through a pipeline, this technology draws material into the system by creating a lower pressure zone. This method is particularly effective for handling fine powders, granules, and other dry bulk materials, ensuring efficient and safe material transfer in various industrial applications.
The Core Design Principles of Negative Pressure Suction Systems
The design of a negative pressure suction system is built upon several key principles that ensure optimal performance and reliability. The primary principle is the creation of a consistent vacuum or negative pressure within the suction line. This is achieved through the use of a vacuum pump or other vacuum generation devices, which maintain a pressure differential between the material source and the suction point. The pressure differential is crucial as it provides the necessary force to draw material from the source into the pipeline.
Another critical design principle involves the proper selection and configuration of components such as the suction nozzle, pipeline diameter, and filter systems. The suction nozzle is typically designed to minimize air resistance and maximize material intake, while the pipeline diameter is optimized to balance material flow rate and pressure drop. Filter systems are integrated to prevent dust and debris from entering the vacuum pump, ensuring long-term operational efficiency and equipment longevity.

Key Components and Their Functions in Negative Pressure Suction Equipment
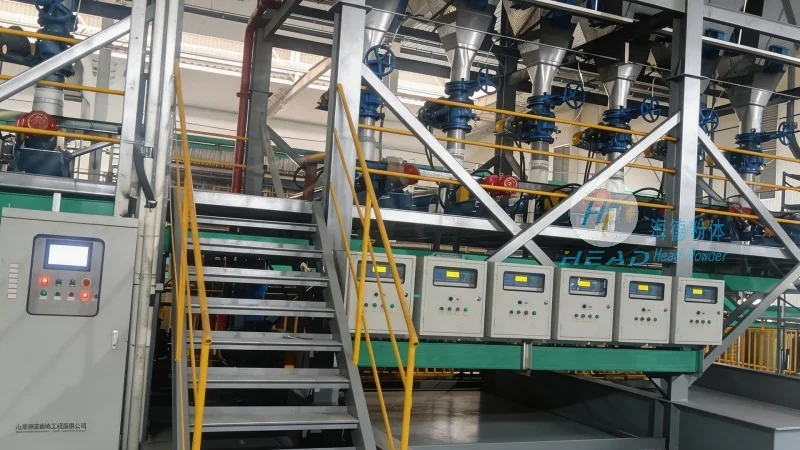
HeadPowder's negative pressure suction systems consist of several essential components, each playing a vital role in the overall operation. The vacuum pump is the heart of the system, responsible for generating the required vacuum level. It can be either a rotary vane pump, a roots blower, or a combination of both, depending on the application's specific needs. The vacuum pump is connected to the suction line via a manifold or a series of pipes, which distribute the vacuum to the various suction points.
The suction nozzle is a critical component that directly interacts with the material source. It is typically made of durable materials like stainless steel or polyethylene to withstand abrasion and corrosion from the bulk material. The nozzle design may include features such as a diffuser or a venturi to enhance the suction effect and improve material flow. The nozzle is usually mounted on a flexible hose or a rigid pipe, allowing for easy positioning and adjustment at the material source.
The pipeline system is another essential part of the negative pressure suction equipment. It consists of a network of pipes that connect the suction nozzle to the vacuum pump and other processing equipment. The pipeline diameter is carefully selected to minimize pressure losses while maintaining an adequate flow rate. The material of the pipeline is chosen based on the properties of the bulk material, such as its abrasiveness or corrosiveness. For example, stainless steel or PVC pipes are commonly used for handling powders and granules.
Advantages of Negative Pressure Suction Material Handling
There are several advantages to using negative pressure suction systems for material handling. One of the main benefits is the ability to transport materials over long distances without the need for multiple transfer points. This reduces the risk of material spillage and contamination, as the material remains contained within the pipeline. Additionally, negative pressure systems are more energy-efficient compared to positive pressure systems, as they require less power to operate.
Another advantage is the reduced risk of dust and fume emissions. Since the system operates under a vacuum, the material is drawn into the pipeline rather than being expelled into the environment. This helps to maintain a clean and safe working environment, especially in industries where dust is a health hazard. Furthermore, negative pressure systems are more flexible in terms of material handling, as they can accommodate a wide range of bulk materials, including fine powders and granules.

Applications and Industries Using Negative Pressure Suction Equipment
Negative pressure suction material handling equipment is widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and other fine powders, ensuring a clean and sterile environment. In food processing, it is used to handle dry ingredients like flour, sugar, and spices, maintaining food safety standards. In chemical manufacturing, it is used to transport powders and granules, reducing the risk of chemical exposure and contamination.
In the mining industry, negative pressure suction systems are used to transport ore and other bulk materials from the mine to processing facilities. This method is particularly useful in underground mining operations, where it is difficult to use traditional positive pressure systems due to the confined space and the need to maintain a safe atmosphere. The negative pressure system helps to keep the mine environment clean and free from dust and fumes.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of negative pressure suction material handling equipment. Our company specializes in designing and manufacturing high-quality systems that meet the specific needs of various industries. By adhering to the core design principles of negative pressure suction technology, we ensure that our equipment is efficient, reliable, and safe for use. Whether you are in the pharmaceutical, food, chemical, or mining industry, our negative pressure suction systems can help you achieve efficient and safe material handling. Contact us today to learn more about our products and services.