

Working Principle and Features of Stabilizer Powder Material Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in providing advanced pneumatic conveying systems tailored for transporting stabilizer powders. This article delves into the working principle and key features of such equipment, offering insights into its operational efficiency and technical advantages.

Introduction to Pneumatic Conveying Systems for Stabilizer Powders
Stabilizer powders, widely used in various industrial applications such as construction, chemical processing, and food production, require reliable and efficient transport methods to maintain product integrity and operational safety. Pneumatic conveying equipment offers a solution that minimizes material degradation, ensures hygienic handling, and enhances overall process efficiency. HeadPowder Engineering Co., Ltd., based in Shandong, China, has been at the forefront of developing customized pneumatic conveying solutions for diverse powder materials, including stabilizers.
Working Principle of Stabilizer Powder Pneumatic Conveying Equipment
The core mechanism of pneumatic conveying for stabilizer powders involves the use of air or gas to transport dry powders through a pipeline system. The process typically operates on one of two fundamental principles: pressure or vacuum. In pressure systems, a positive pressure is generated at the inlet, forcing the powder and air mixture through the pipeline to the discharge point. Conversely, vacuum systems create a negative pressure at the discharge end, drawing the powder from the source to the collection point. Both methods rely on the interaction between the air flow and the powder particles to achieve efficient transport.

Key components of the system include the material feed hopper, which holds the stabilizer powder and regulates the feed rate; the air compressor or vacuum pump, which provides the necessary pressure or vacuum; the conveying pipeline, which transports the powder; and the discharge unit, which collects the material at the destination. The design of these components is critical to ensure consistent performance and minimal product loss. For instance, the feed hopper often incorporates a rotary valve or screw feeder to control the flow of powder, preventing blockages and maintaining a steady feed rate. The air compressor or vacuum pump is selected based on the specific characteristics of the stabilizer powder, such as particle size, density, and moisture content, to optimize the conveying efficiency.
Key Features of Stabilizer Powder Pneumatic Conveying Equipment
HeadPowder's pneumatic conveying systems for stabilizer powders are characterized by several notable features that enhance their performance and usability. Firstly, the equipment is designed for minimal product degradation, which is crucial for stabilizer powders that may be sensitive to moisture or temperature changes. The use of smooth, corrosion-resistant pipelines and appropriate air flow rates helps prevent agglomeration and caking of the powder, ensuring that the material remains in its original form throughout the conveying process. Secondly, the systems are equipped with advanced control mechanisms that allow for precise regulation of the conveying rate, pressure, and vacuum levels. This enables operators to adjust the system parameters in real-time based on the specific requirements of the application, improving process flexibility and reducing downtime.

Another significant feature is the hygienic design of the equipment, which is essential for industries where product purity is paramount, such as food and pharmaceuticals. The components are constructed from materials like stainless steel, which are easy to clean and maintain, and the system is equipped with features like CIP (Clean-In-Place) capabilities to ensure thorough sanitation. This not only meets regulatory standards but also extends the lifespan of the equipment and reduces maintenance costs. Additionally, the systems are designed for energy efficiency, with optimized air flow and pressure control that minimize energy consumption while maintaining high conveying rates. This feature is particularly important for large-scale industrial operations where operational costs are a key consideration.
Advantages of Using Pneumatic Conveying for Stabilizer Powders
Implementing pneumatic conveying equipment for stabilizer powders offers numerous advantages over traditional methods like belt conveyors or manual handling. One of the primary benefits is the ability to transport powders over long distances without the need for multiple transfer points, which reduces the risk of material contamination and improves overall process continuity. The system also eliminates the need for manual handling, which enhances workplace safety and reduces labor costs. Furthermore, pneumatic conveying is highly flexible, allowing for changes in the conveying route or destination without significant modifications to the system. This adaptability is particularly valuable in dynamic industrial environments where production requirements may change frequently.
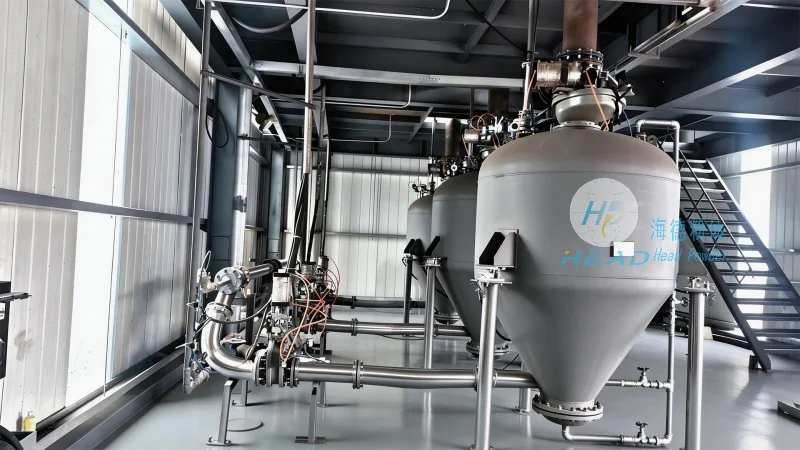
Another advantage is the improved product quality and consistency achieved through pneumatic conveying. The gentle handling of the powder particles minimizes breakage and degradation, resulting in a more uniform product that meets the exact specifications required by downstream processes. This is especially important for stabilizer powders, which are often used as additives in final products where even minor variations can affect performance. The system also reduces the risk of cross-contamination between different powder types, as each conveying line can be dedicated to a specific material. This feature is critical in industries where product purity is non-negotiable, such as in the production of food additives or pharmaceutical excipients.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, is a trusted provider of high-quality pneumatic conveying equipment for stabilizer powders. The company's expertise lies in designing and manufacturing customized systems that meet the unique requirements of each application, ensuring optimal performance, efficiency, and reliability. By leveraging advanced technology and rigorous quality control, HeadPowder delivers solutions that enhance operational productivity while maintaining the highest standards of product integrity and safety. For industries seeking reliable and efficient transport solutions for stabilizer powders, HeadPowder's pneumatic conveying equipment represents a superior choice.