

Principle and Working Scene Characteristics of Soda Ash Powder Conveyors
Understanding the operational principles and application scenarios of soda ash powder conveyors is crucial for industries that rely on efficient handling of this essential chemical. As a specialized equipment for transporting soda ash, these systems combine mechanical engineering with material handling expertise to ensure reliable and safe transport. This article delves into the core principles behind soda ash powder conveyors, exploring their design, functionality, and the specific environments where they excel.
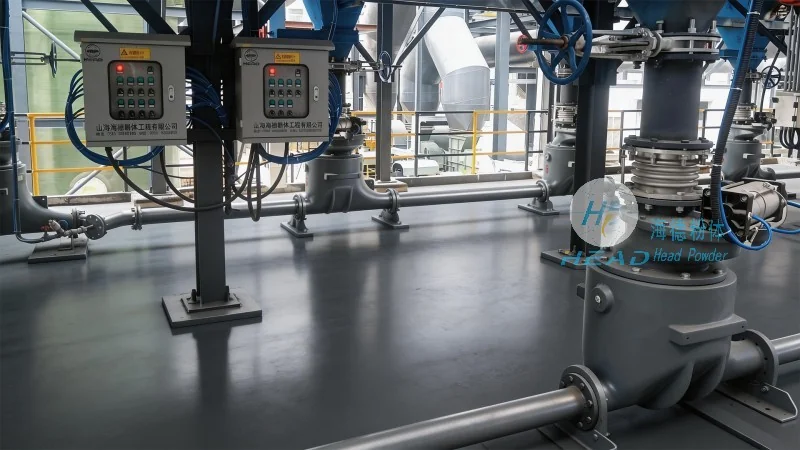
Working Principle of Soda Ash Powder Conveyors
Soda ash powder conveyors operate on fundamental principles of material transport, tailored to the unique properties of soda ash. The primary mechanism involves the use of rotating components, such as screw conveyors or pneumatic systems, to move the powder from one location to another. For example, a screw conveyor consists of a helical screw rotating inside a cylindrical tube. As the screw turns, it pushes the soda ash forward, leveraging the friction between the powder and the screw surface. This method is particularly effective for dry, free-flowing powders like soda ash, as it minimizes material degradation and maintains consistent flow rates. In contrast, pneumatic conveyors utilize air pressure to transport the powder through a pipeline, where the material is suspended in a stream of air. This approach is advantageous for longer distances or when dealing with more delicate powders, as it reduces mechanical stress and prevents particle agglomeration.

Key Features and Technical Advantages
Headpowder, a leading manufacturer based in Shandong, China, has developed soda ash powder conveyors with several key features that enhance performance and reliability. One of the most significant advantages is the system's ability to handle high volumes of material with minimal energy consumption. The design optimizes the balance between power input and output, ensuring efficient operation even under heavy load conditions. Additionally, the conveyors are constructed with corrosion-resistant materials, such as stainless steel, to withstand the chemical properties of soda ash and prevent contamination. This feature is critical in industries where product purity is paramount, such as food processing or pharmaceutical manufacturing. Another notable aspect is the system's adaptability to different operational conditions. The conveyors can be customized to accommodate varying particle sizes, moisture levels, and flow rates, making them suitable for diverse applications. This flexibility allows users to integrate the equipment seamlessly into existing production lines without extensive modifications.
Common Working Scenarios and Applications
Soda ash powder conveyors are widely used in various industrial settings, where their ability to handle bulk materials efficiently is essential. In the chemical industry, these systems are commonly employed in soda ash production facilities to transport raw materials and finished products. The conveyors ensure a smooth flow of material between reactors, storage tanks, and packaging areas, reducing downtime and improving overall production throughput. In the food and beverage sector, soda ash is used as a leavening agent and pH adjuster, and the conveyors help maintain product quality by preventing contamination and ensuring consistent dosing. Similarly, in the construction industry, soda ash is used in the production of glass and ceramics, where the conveyors facilitate the transport of raw materials to processing equipment. The systems are also utilized in environmental applications, such as water treatment, where soda ash is used to adjust pH levels and remove impurities. In each of these scenarios, the conveyors contribute to operational efficiency and product quality by providing reliable and consistent material transport.

Company Profile and Service Commitment
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name Headpowder, is a professional manufacturer specializing in powder handling equipment. With a strong presence in Shandong, China, the company has built a reputation for delivering high-quality, customized solutions tailored to the needs of various industries. Headpowder's team of engineers and technicians leverages years of experience in material handling to design and manufacture conveyors that meet international standards. The company emphasizes customer satisfaction by providing comprehensive support, including installation, maintenance, and technical assistance. By focusing on innovation and quality, Headpowder ensures that its soda ash powder conveyors not only meet but exceed industry expectations, providing reliable performance and long-term value to clients worldwide.