

Dry Coffee Pneumatic Conveying Solutions
For coffee processing facilities, the efficient and safe transfer of dry coffee beans and related products is a critical operational requirement. Traditional methods such as manual handling or mechanical conveyors often present challenges related to contamination, product degradation, and labor costs. This article introduces a specialized pneumatic conveying system designed specifically for dry coffee applications, highlighting its benefits, technical features, and the expertise of Shandong HeadPowder Engineering Co., Ltd. as a leading provider in the field.

Understanding Pneumatic Conveying for Dry Coffee
Pneumatic conveying systems utilize air or gas to transport dry materials like coffee beans through a pipeline network. This technology offers several advantages over conventional methods, including reduced risk of product contamination, improved product quality preservation, and enhanced operational flexibility. The system works by creating a pressure differential that moves the material through the pipeline, ensuring a clean and controlled transfer process. For coffee producers, this means maintaining the aromatic integrity and quality of the beans while minimizing the risk of moisture or foreign particle introduction.
Key Features of the HeadPowder Dry Coffee Conveying System
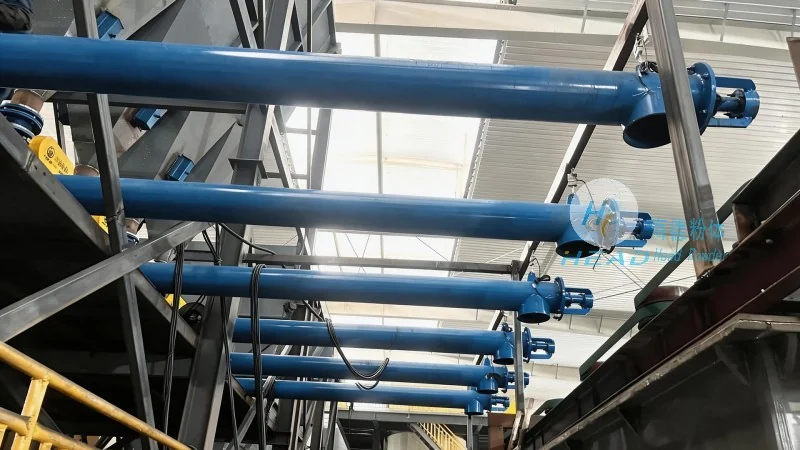
Shandong HeadPowder Engineering Co., Ltd. offers a comprehensive range of pneumatic conveying solutions tailored to the unique needs of coffee processing. The system is designed with several key features that enhance performance and reliability. First, the use of positive pressure or negative pressure conveying options allows for flexibility in system layout and material handling requirements. The equipment is constructed from food-grade materials, ensuring compliance with industry standards for product safety. Additionally, the system incorporates advanced control mechanisms that optimize air flow and material transport, reducing energy consumption and operational costs. The conveying lines are equipped with high-quality valves and filters, which help maintain product purity and prevent system blockages. The design also includes easy-to-clean components, facilitating regular maintenance and hygiene compliance in coffee processing environments.
Benefits for Coffee Processing Facilities
Implementing a dry coffee pneumatic conveying system from HeadPowder brings numerous benefits to coffee processing operations. One of the primary advantages is the significant reduction in labor costs associated with manual handling of coffee beans. The automated system minimizes the need for manual labor, improving operational efficiency and reducing the risk of workplace injuries. Additionally, the system enhances product quality by preventing contamination from external sources and preserving the natural aroma and flavor of the coffee beans. This is particularly important for specialty coffee producers who rely on the quality of their beans to maintain market competitiveness. The system also contributes to improved workplace safety by eliminating the need for workers to handle heavy or bulky coffee bags, reducing the risk of musculoskeletal injuries. Furthermore, the energy-efficient design of the HeadPowder system helps reduce operational costs over time, making it a cost-effective investment for coffee processing facilities.

Customization and Integration Capabilities
HeadPowder understands that each coffee processing facility has unique operational requirements. Therefore, the company offers customized pneumatic conveying solutions that can be integrated seamlessly into existing production lines. The engineering team at HeadPowder works closely with clients to assess their specific needs, including material characteristics, production volume, and facility layout. This collaborative approach ensures that the final system is optimized for maximum efficiency and minimal downtime. The company provides comprehensive support throughout the entire project lifecycle, from initial design and installation to ongoing maintenance and technical support. This commitment to customer service and technical expertise makes HeadPowder a trusted partner for coffee processing facilities seeking reliable and efficient material handling solutions.
Conclusion
For coffee processing facilities looking to enhance their material handling capabilities while maintaining product quality and operational efficiency, the dry coffee pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers a superior solution. The system’s advanced features, customized design options, and commitment to quality make it an ideal choice for both small and large-scale coffee producers. By leveraging the expertise of HeadPowder, coffee facilities can achieve improved operational performance, reduced costs, and enhanced product quality, ultimately contributing to their long-term success in the competitive coffee market.