

Malt Pneumatic Conveying System Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in designing and implementing efficient malt pneumatic conveying systems. Based in Shandong, China, the company leverages advanced engineering principles to deliver tailored solutions that meet the specific needs of the malt processing industry. This article explores the key components, benefits, and practical applications of their malt pneumatic conveying systems, highlighting how they enhance operational efficiency and product quality.

Understanding Malt Pneumatic Conveying Technology
Malt pneumatic conveying systems utilize air or gas to transport malt grains and other bulk materials from one location to another within a processing facility. Unlike traditional mechanical conveying methods, such as screw conveyors or belt conveyors, pneumatic systems offer several advantages, including reduced risk of contamination, lower maintenance requirements, and the ability to handle materials with high moisture content or delicate characteristics. The core technology involves a series of components, including a hopper, feeder, air compressor, and conveying line, which work in tandem to ensure smooth and reliable material transport.
Key Components of the Malt Pneumatic Conveying System
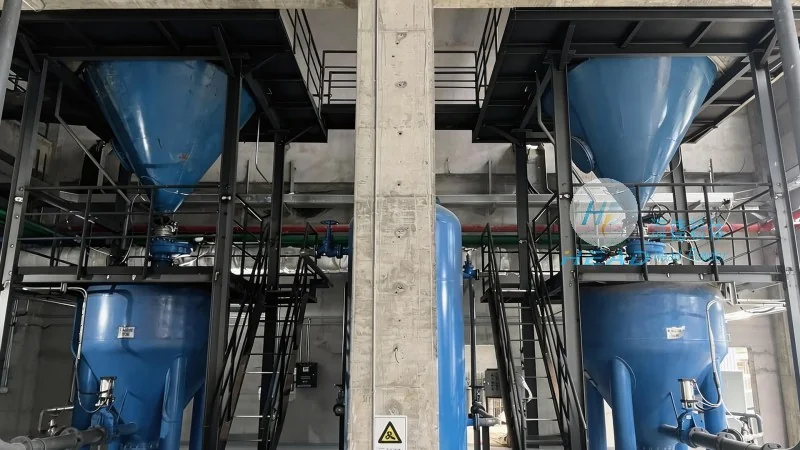
The malt pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. incorporates several critical components that ensure optimal performance. The system begins with a hopper, which stores the malt and feeds it into the system via a rotary valve or screw feeder. This component is designed to maintain consistent material flow and prevent blockages. Next, the air compressor generates the necessary pressure to move the malt through the conveying line. The line itself is typically made of stainless steel or other corrosion-resistant materials to accommodate the acidic and moisture-rich environment of malt processing. Additionally, the system includes a filter and cyclone separator to remove dust and debris from the air, ensuring compliance with environmental regulations and maintaining air quality within the facility.
Benefits of Implementing a Malt Pneumatic Conveying System
Adopting a malt pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers numerous benefits for malt processing facilities. One of the primary advantages is improved hygiene and sanitation, as the enclosed system minimizes direct contact between the malt and the environment, reducing the risk of microbial contamination. This is particularly important in the food and beverage industry, where product safety is paramount. Additionally, the system enhances operational efficiency by reducing downtime and maintenance costs. The smooth, continuous flow of materials minimizes bottlenecks and ensures that production processes run seamlessly. Furthermore, the system’s ability to handle varying material characteristics, such as different malt types or moisture levels, makes it a versatile solution for diverse processing needs.

Customization and Scalability for Diverse Applications
Shandong HeadPowder Engineering Co., Ltd. understands that each malt processing facility has unique requirements. Therefore, their pneumatic conveying systems are designed to be customizable and scalable. The company works closely with clients to assess their specific operational needs, including the volume of malt to be conveyed, the distance between processing stages, and the desired level of automation. By tailoring the system to these parameters, they ensure that the solution is both effective and cost-efficient. The systems can be scaled from small-scale operations to large industrial facilities, making them suitable for a wide range of applications, from small breweries to large-scale malt production plants.

Case Studies and Real-World Applications
Several malt processing facilities have benefited from the implementation of Shandong HeadPowder Engineering Co., Ltd.’s pneumatic conveying systems. For example, a medium-sized brewery in Shandong, China, reported a 20% reduction in labor costs and a 15% increase in production efficiency after upgrading to their system. The facility noted that the enclosed design reduced the risk of contamination, leading to higher product quality and compliance with food safety standards. Another client, a large malt production plant, implemented the system to handle high volumes of malt over long distances, achieving a 30% reduction in energy consumption compared to traditional conveying methods. These case studies demonstrate the effectiveness and reliability of the systems in real-world scenarios.
Conclusion and Contact Information
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive malt pneumatic conveying system solutions that enhance operational efficiency, improve product quality, and ensure compliance with industry standards. With their expertise in engineering and customization, they offer tailored systems that meet the unique needs of malt processing facilities. For more information or to discuss how a malt pneumatic conveying system can benefit your operation, please contact Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China.