

Airborne Conveying System Solutions for Lithium-Ion Battery Positive Electrode Materials
For manufacturers in the lithium-ion battery industry, the efficient and safe handling of positive electrode materials is a critical operational challenge. The traditional methods of material transport, such as manual handling or mechanical conveyors, often present significant risks related to dust exposure, material degradation, and operational inefficiencies. To address these challenges, advanced airborne conveying systems have emerged as a preferred solution. These systems leverage pneumatic technology to transport positive electrode powders and related materials with precision, ensuring minimal contamination and optimal process control.
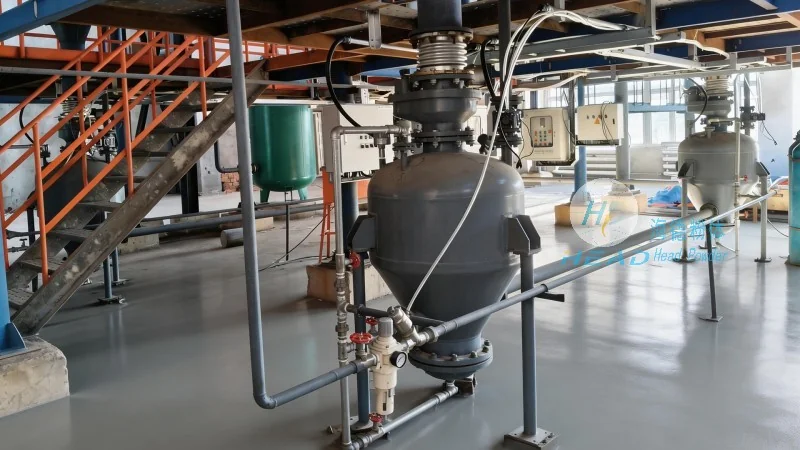
HeadPowder Engineering: A Leader in Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a specialized engineering firm dedicated to providing innovative material handling solutions for the battery and powder processing sectors. With a strong focus on research and development, HeadPowder has established itself as a trusted partner for companies seeking reliable and efficient conveying systems. The company’s expertise lies in designing and implementing customized airborne conveying solutions tailored to the unique requirements of lithium-ion battery production lines. By integrating state-of-the-art technology with practical engineering insights, HeadPowder ensures that its systems meet the stringent quality and safety standards essential for modern battery manufacturing.
Key Features of the Airborne Conveying System
The airborne conveying system designed by HeadPowder for lithium-ion battery positive electrode materials incorporates several key features that enhance performance and reliability. First, the system utilizes high-efficiency pneumatic transport technology, which allows for the seamless movement of powders over long distances with minimal pressure loss. This technology ensures consistent material flow rates, reducing the risk of clogging or material degradation during transport. Second, the system is equipped with advanced filtration and dust control mechanisms. These components are crucial for maintaining a clean working environment and preventing dust contamination, which is vital for both product quality and worker safety. The filtration systems are designed to capture fine particles, ensuring compliance with environmental regulations and industry standards. Third, the system incorporates intelligent control and monitoring capabilities. Through integrated sensors and control panels, operators can monitor the system’s performance in real-time, allowing for quick adjustments and maintenance. This feature enhances operational efficiency and reduces downtime, contributing to overall productivity improvements.

Customization and Integration Capabilities
HeadPowder understands that each battery manufacturing facility has unique operational needs and space constraints. Therefore, the airborne conveying system is designed with high levels of customization. The company works closely with clients to assess their specific requirements, including material types, production volumes, and facility layout. Based on this assessment, HeadPowder engineers develop tailored solutions that integrate seamlessly with existing production lines. The system can be adapted to handle various positive electrode materials, such as lithium cobalt oxide (LCO), lithium iron phosphate (LFP), and nickel manganese cobalt oxide (NMC), among others. Additionally, the system can be integrated with other processing equipment, such as mixing, drying, and coating machines, creating a cohesive material handling workflow. This integration minimizes material handling steps, reduces the risk of cross-contamination, and optimizes the overall production process.

Benefits of Implementing an Airborne Conveying System
Adopting an airborne conveying system for lithium-ion battery positive electrode materials offers numerous benefits for manufacturers. One of the primary advantages is improved safety. By eliminating manual handling of powders, the system reduces the risk of dust explosions and respiratory health issues for workers. This not only enhances workplace safety but also helps companies comply with occupational health and safety regulations. Another significant benefit is enhanced product quality. The system’s enclosed and controlled environment minimizes material exposure to moisture, air, and contaminants, ensuring that the positive electrode powders maintain their desired properties. This leads to more consistent battery performance and higher product reliability. Furthermore, the system improves operational efficiency. With automated material transport, production lines can operate at higher speeds without the need for manual intervention. The real-time monitoring and control features allow for quick identification and resolution of issues, reducing downtime and increasing overall productivity. Finally, the system contributes to cost savings. By reducing material waste and improving process efficiency, manufacturers can lower their operational costs and enhance their competitive position in the market.
Conclusion and Contact Information
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive airborne conveying system solutions for lithium-ion battery positive electrode materials. By leveraging advanced pneumatic technology and customized engineering, HeadPowder delivers systems that enhance safety, improve product quality, and boost operational efficiency. For companies seeking reliable and efficient material handling solutions, HeadPowder is a trusted partner. The company’s commitment to innovation and customer satisfaction ensures that its systems meet the evolving needs of the battery industry. If you are interested in learning more about how an airborne conveying system can benefit your lithium-ion battery production, please contact HeadPowder for a consultation.