

Limestone Powder Pneumatic Conveying Solutions
Limestone powder, a widely used material in various industrial applications such as flue gas desulfurization, water treatment, and construction, requires efficient and reliable handling methods to ensure safe and effective processing. Pneumatic conveying systems have emerged as a preferred solution for transporting limestone powder due to their ability to handle fine powders, minimize dust emissions, and maintain process integrity. This article provides an overview of the key considerations and solutions for limestone powder pneumatic conveying, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in designing and implementing advanced air-driven conveying systems.
Key Challenges in Limestone Powder Handling
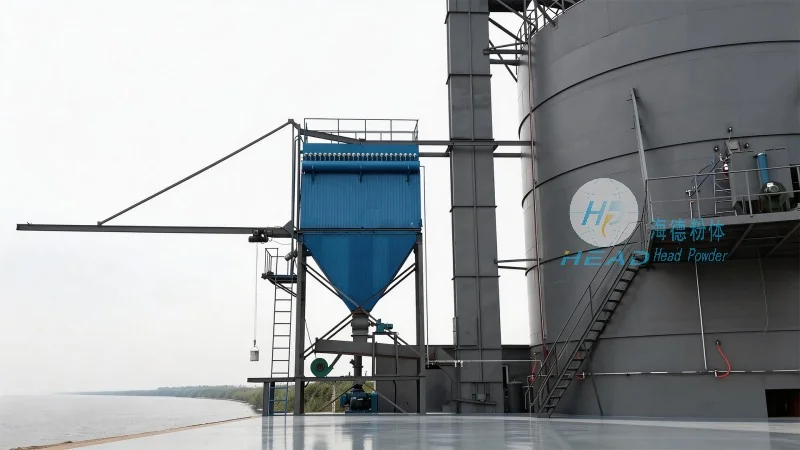
Handling limestone powder presents several challenges that traditional methods may struggle to address. Fine particles are prone to agglomeration, leading to blockages in pipelines and reduced system efficiency. Additionally, dust control is critical to maintain a safe working environment and comply with environmental regulations. Traditional methods like belt conveyors or bucket elevators often result in high dust emissions and material loss, making them unsuitable for many applications. Pneumatic conveying offers a solution by using air to transport the powder, reducing the risk of dust exposure and ensuring a more controlled process.
HeadPowder's Expertise in Pneumatic Conveying Technology
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in the design, manufacturing, and installation of customized pneumatic conveying systems tailored to the unique needs of limestone powder handling. With years of experience in the industry, HeadPowder has developed a deep understanding of the material properties and operational requirements of limestone powder, enabling them to provide optimized solutions that enhance productivity and reduce operational costs. The company's team of engineers and technicians work closely with clients to assess their specific requirements, from material characteristics and flow rates to space constraints and environmental regulations, to design a system that meets all operational and safety standards.

Customized Pneumatic Conveying Solutions for Limestone Powder
HeadPowder offers a range of pneumatic conveying solutions tailored to different limestone powder applications and operational conditions. The primary types of systems include dilute-phase and dense-phase conveying, each with distinct advantages depending on the material's properties and the required transport distance. Dilute-phase systems use low air velocities to transport the powder in a dispersed state, suitable for short to medium distances and low to medium flow rates. Dense-phase systems, on the other hand, use higher air velocities and lower flow rates to create a dense mixture of powder and air, ideal for longer distances and higher material loads. HeadPowder's engineers select the appropriate system type based on factors such as the limestone powder's particle size, moisture content, and the distance between the source and destination points, ensuring optimal performance and minimal energy consumption.
Key Components of Limestone Powder Pneumatic Conveying Systems
A pneumatic conveying system for limestone powder typically consists of several key components, each playing a crucial role in the overall operation. The primary components include a material feeder, which accurately controls the flow rate of the limestone powder into the system; a conveying line, which transports the powder using air; a receiver, which collects the material at the destination; and a dust collector, which captures any airborne particles to ensure environmental compliance. HeadPowder's systems are equipped with high-quality components from reputable manufacturers, ensuring durability, reliability, and efficient performance. The material feeder is designed to handle fine powders without clogging, while the conveying line is constructed from materials resistant to corrosion and abrasion, such as stainless steel or special alloys, to withstand the abrasive nature of limestone powder. The receiver is equipped with a venting system to prevent pressure buildup and maintain a safe operating environment. The dust collector, often a baghouse or cartridge filter, effectively captures dust particles, reducing emissions and maintaining a clean working environment.

Advantages of Using Pneumatic Conveying for Limestone Powder
Implementing a pneumatic conveying system for limestone powder offers numerous advantages over traditional handling methods. One of the most significant benefits is the reduction in dust emissions, which not only improves workplace safety but also helps companies comply with environmental regulations. Pneumatic systems also minimize material loss, as the powder is transported in a closed system, preventing spillage and contamination. Additionally, these systems offer greater flexibility in terms of layout and space utilization, as they can be installed in various configurations to fit the specific needs of the facility. The use of air as the conveying medium allows for a more controlled and consistent flow rate, ensuring that the limestone powder reaches the destination without variations in quality or quantity. Furthermore, pneumatic conveying systems are generally more energy-efficient compared to other methods, as they require less power to transport the material over short to medium distances. HeadPowder's systems are designed to maximize these advantages, providing clients with a reliable and cost-effective solution for their limestone powder handling needs.
Case Studies and Real-World Applications
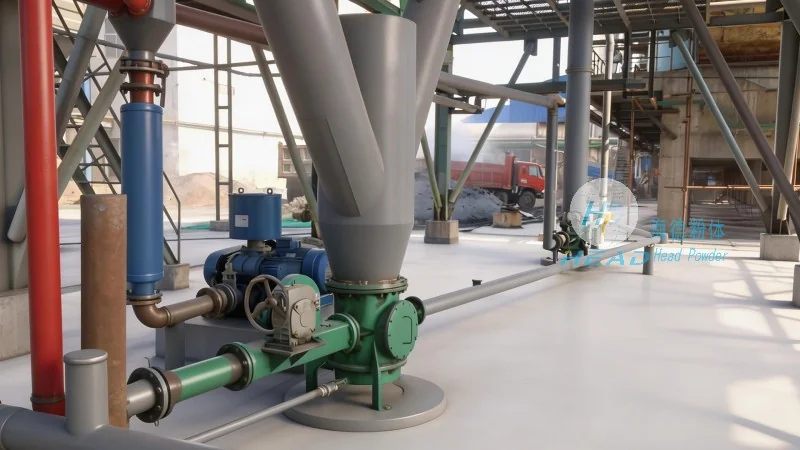
HeadPowder has successfully implemented numerous pneumatic conveying systems for limestone powder in various industries, demonstrating the effectiveness of their solutions. For example, in a flue gas desulfurization plant, HeadPowder designed a dense-phase system to transport limestone powder from storage silos to the reaction tower. The system was able to handle the fine powder without agglomeration, ensuring a consistent flow rate and minimizing downtime. In another application, a water treatment facility used a dilute-phase system to convey limestone powder from a mixing tank to a storage tank. The system was installed in a compact space, meeting the facility's layout requirements while maintaining high efficiency. These case studies highlight the versatility and reliability of HeadPowder's pneumatic conveying solutions, which can be adapted to meet the specific needs of different limestone powder applications.
Conclusion and Contact Information
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive and customized pneumatic conveying solutions for limestone powder, addressing the unique challenges of handling fine powders while ensuring operational efficiency and safety. With their expertise in pneumatic conveying technology and commitment to quality, HeadPowder is a trusted partner for industries relying on limestone powder in their processes. For more information on their limestone powder pneumatic conveying systems, please contact HeadPowder at their address in Shandong, China.