

What is Crystal Granular Material Conveying? And What Are the Design Principles?
Crystal granular material conveying is a specialized field within material handling that focuses on the efficient transportation of crystalline and granular substances. This process is crucial in various industrial applications, including pharmaceuticals, chemicals, food processing, and mining, where precise control over material flow is essential for maintaining product quality and operational efficiency.

Understanding Crystal Granular Material Conveying
At its core, crystal granular material conveying involves the movement of solid particles with a crystalline structure or granular form from one location to another. These materials often exhibit unique properties such as varying densities, moisture content, and flow characteristics, which require specialized equipment and design considerations to ensure smooth and reliable transport. The primary goal of this process is to achieve consistent material flow rates, minimize product degradation, and reduce operational downtime.
Key Design Principles for Crystal Granular Material Conveying Systems
The design of effective crystal granular material conveying systems is governed by several critical principles that address the specific challenges posed by these materials. First, the system must accommodate the unique flow characteristics of the material, such as its angle of repose, cohesion, and compressibility. This often necessitates the use of specialized components like flexible hoses, rotary valves, and conveyor belts designed to handle non-free-flowing materials without causing blockages or degradation.
Second, the system must ensure minimal product contamination and degradation. This is achieved through the use of sanitary or food-grade materials for components that come into direct contact with the material, as well as the implementation of gentle handling techniques to prevent crushing or overheating of the crystals. Additionally, the design must consider the need for easy cleaning and maintenance to comply with regulatory standards in industries like pharmaceuticals and food processing.
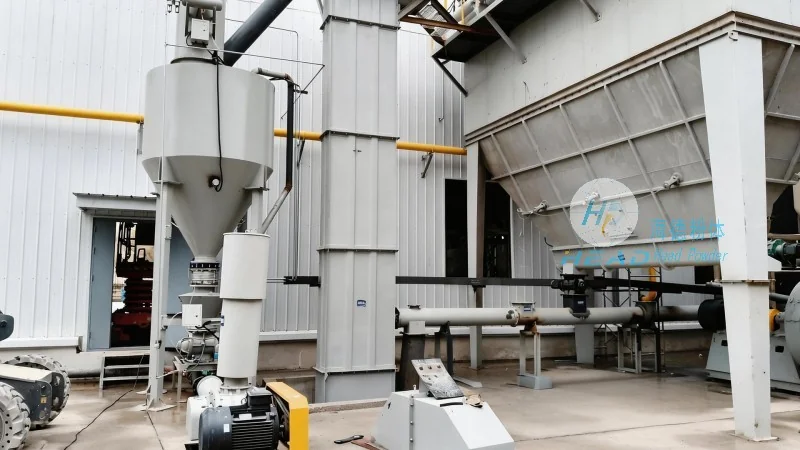
Components and Technologies Used in Crystal Granular Material Conveying
Modern crystal granular material conveying systems rely on a combination of advanced components and technologies to achieve optimal performance. Key components include: rotary airlock valves, which control the flow of material from hoppers to conveyors; flexible hoses or tubing, which allow for flexible routing and reduce the risk of material buildup; and conveyor belts or screw conveyors, which provide the primary means of transporting the material. In some cases, pneumatic conveying systems are used, where compressed air is employed to move the material through a pipeline, offering advantages in terms of cleanliness and reduced mechanical wear.
Each component is carefully selected and integrated to address the specific needs of the material being conveyed. For example, the choice of a screw conveyor versus a belt conveyor depends on the material's flowability and the required conveying distance. Similarly, the selection of a flexible hose material, such as food-grade PVC or stainless steel, is based on the material's chemical compatibility and the need for hygiene.
Applications and Industries Benefiting from Crystal Granular Material Conveying
Crystal granular material conveying is widely used across various industries where the handling of crystalline and granular materials is critical. In the pharmaceutical industry, it is essential for the transport of active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials are handled in a sterile and controlled environment. In the chemical industry, it is used for the conveyance of raw materials and finished products, such as fertilizers and specialty chemicals, where precise control over flow and temperature is necessary to prevent reactions or degradation.

In the food processing industry, crystal granular material conveying is used for the handling of ingredients like sugar, salt, and spices, where maintaining product quality and preventing contamination is paramount. Similarly, in the mining and mineral processing sector, it is used for the transport of raw minerals and processed products, such as ores and concentrates, where the ability to handle abrasive and heavy materials is crucial.
Advantages of Professional Crystal Granular Material Conveying Solutions
Implementing a well-designed crystal granular material conveying system offers numerous advantages for industrial operations. These include improved material flow consistency, reduced downtime due to equipment failure or blockages, and enhanced product quality through gentle handling. Additionally, specialized systems can help minimize material waste by reducing spillage and ensuring efficient use of the material being transported.
Another key advantage is the ability to integrate the conveying system with other processing equipment, such as mixers, dryers, and packaging machines, creating a seamless production line. This integration improves overall operational efficiency and reduces the need for manual handling, which can be labor-intensive and prone to errors.

Shandong HeadPowder Engineering Co., Ltd.: Your Partner in Crystal Granular Material Conveying
For businesses seeking reliable and efficient crystal granular material conveying solutions, Shandong HeadPowder Engineering Co., Ltd. is a trusted partner with extensive expertise in the field. Based in Shandong, China, HeadPowder specializes in the design, manufacturing, and installation of customized material handling systems tailored to the unique needs of each client.
Our team of experienced engineers and technicians works closely with clients to understand their specific material characteristics, operational requirements, and regulatory standards. We then develop and implement solutions that incorporate the latest technologies and best practices in crystal granular material conveying, ensuring that the final system meets all performance and safety requirements.
HeadPowder's commitment to quality and customer satisfaction is reflected in our comprehensive service offerings, which include system design, equipment supply, installation, and ongoing maintenance. We pride ourselves on delivering solutions that not only meet but exceed industry standards, helping our clients achieve their production goals while maintaining the highest levels of product quality and operational efficiency.