

[MOST POPULAR] Mobile Powder Conveying Systems: Exploring Their Function and Design Principles
For industries dealing with bulk powders, the efficiency and reliability of material handling equipment are critical. A mobile powder conveying system represents a sophisticated solution designed to transport dry powders and bulk materials with precision and adaptability. This article delves into what these systems entail and the fundamental design principles that underpin their operation, providing insights into their role in modern industrial processes.
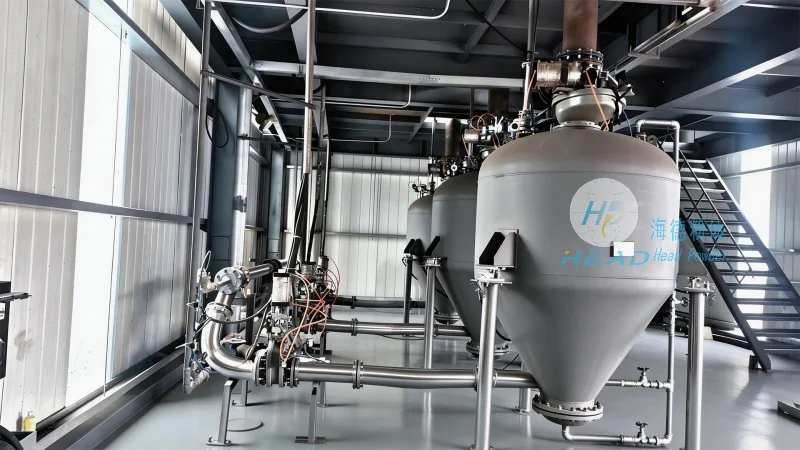
Key Components and Functional Aspects of Mobile Powder Conveying Lines
At the core of a mobile powder conveying system are several key components that work in tandem to ensure smooth material transport. These typically include a hopper for material storage, a conveyor mechanism (such as screw, belt, or pneumatic systems), and a control unit that regulates the flow and speed of the material. The mobility aspect is achieved through a robust chassis with wheels or tracks, allowing the system to be repositioned as needed without the need for extensive infrastructure changes. This flexibility is particularly valuable in environments where production layouts may change or where multiple processing points are required.

Design Principles Guiding the Development of Mobile Powder Conveying Systems
The design of a mobile powder conveying system is governed by several key principles aimed at optimizing performance, safety, and operational efficiency. One of the primary principles is the minimization of material degradation, which is achieved through gentle handling mechanisms and enclosed systems that prevent contamination or spillage. Another critical principle is the integration of advanced control technologies, such as variable frequency drives (VFDs) and sensors, to monitor and adjust the conveying process in real-time. This ensures consistent material flow rates and prevents issues like blockages or overloading. Additionally, the design emphasizes durability and ease of maintenance, with modular components that can be easily replaced or serviced, reducing downtime and operational costs.

Advantages of Mobile Powder Conveying Systems in Industrial Applications
The adoption of mobile powder conveying systems offers numerous advantages for businesses in various sectors, including pharmaceuticals, food processing, and chemical manufacturing. These systems enhance operational flexibility by allowing for quick reconfiguration of production lines, adapting to changing production demands or product types. They also improve safety by containing dust and preventing material exposure to the environment, which is crucial for compliance with regulatory standards. Furthermore, the energy efficiency of modern mobile conveying systems, often achieved through optimized conveyor speeds and reduced friction, contributes to lower operational costs over time.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
As a leading provider of industrial material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of mobile powder conveying systems tailored to the specific needs of clients. With a focus on innovation and quality, the company leverages advanced engineering principles to develop systems that meet the highest standards of performance and reliability. HeadPowder's expertise in powder technology and material handling ensures that their products are not only efficient but also safe and environmentally friendly, aligning with the evolving demands of modern industries. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales support and customization services, enabling clients to optimize their material handling processes effectively.

Conclusion: The Role of Mobile Powder Conveying Systems in Modern Manufacturing
In conclusion, mobile powder conveying systems represent a vital advancement in the field of bulk material handling, combining mobility, efficiency, and adaptability to meet the complex needs of contemporary industrial operations. By adhering to robust design principles and leveraging advanced technologies, these systems enable businesses to enhance productivity, reduce costs, and maintain compliance with industry regulations. As industries continue to evolve, the importance of reliable and flexible material handling solutions like mobile powder conveying systems will only grow, making them an indispensable component of modern manufacturing processes.