

What is a Positive Pressure Dilute Phase Powder Conveying System Equipment? What are its Design Prin
Positive pressure dilute phase powder conveying systems represent a sophisticated technology used in the handling and transportation of bulk powders. These systems are designed to efficiently move dry powders through pipelines under positive pressure, ensuring reliable and consistent material transfer. The core of such systems lies in their ability to maintain a consistent flow of material while minimizing the risk of blockages or material degradation.
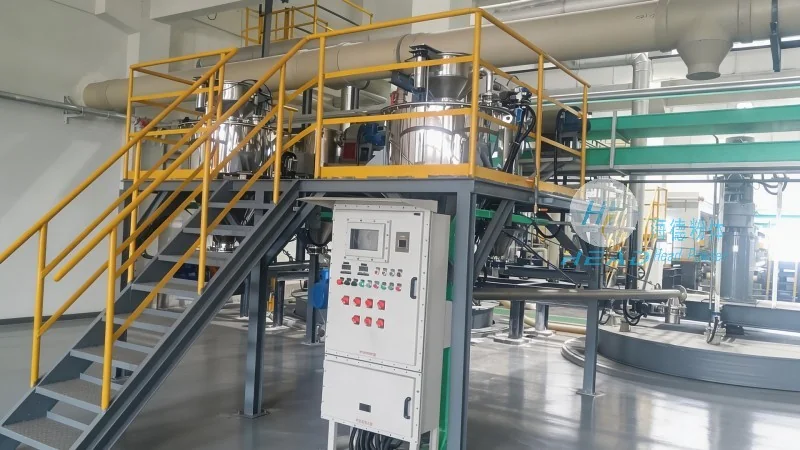
Understanding the Core Components of a Positive Pressure Dilute Phase Powder Conveying System
A typical positive pressure dilute phase powder conveying system comprises several key components that work in tandem to achieve effective material transport. The primary elements include a positive displacement blower or compressor, which generates the necessary pressure to move the powder through the pipeline. This is often supplemented by a hopper or feeder that controls the flow rate of the powder into the system. The pipeline itself is designed to handle the material under pressure, with appropriate fittings and valves to direct and regulate the flow. Additionally, a dust collection or filtration system may be integrated to ensure compliance with air quality standards and to protect the equipment from dust accumulation.

The Design Principles Underpinning Positive Pressure Dilute Phase Powder Conveying
The design principles of positive pressure dilute phase powder conveying systems are centered on maintaining a dilute phase flow, where the powder is suspended in a gas stream rather than being compacted or settled. This approach is critical for preventing blockages and ensuring smooth material movement. The system's design must consider several factors, including the particle size and density of the powder, the required conveying distance and velocity, and the overall system pressure. Engineers must calculate the appropriate air velocity and pressure to achieve the desired flow rate while minimizing energy consumption. The selection of materials for the pipeline and components is also crucial, as they must withstand the abrasive nature of the powder and the high-pressure environment.

Applications and Benefits of Positive Pressure Dilute Phase Powder Conveying Systems
Positive pressure dilute phase powder conveying systems find applications across various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. These systems are particularly advantageous in applications where material purity and contamination control are paramount. The benefits of such systems include improved material handling efficiency, reduced downtime due to blockages, and enhanced safety by minimizing dust exposure. Additionally, the positive pressure design allows for flexible system layouts, enabling the integration of multiple conveying lines and processing units within a facility.
Key Considerations for Implementing a Positive Pressure Dilute Phase Powder Conveying System
When implementing a positive pressure dilute phase powder conveying system, several considerations must be addressed to ensure optimal performance and longevity. The first is the selection of the appropriate equipment based on the specific characteristics of the powder being conveyed. This includes evaluating the particle size distribution, moisture content, and flow properties of the material. The system's design must also account for the required conveying distance and the available space within the facility. Proper maintenance and regular inspections are essential to prevent equipment failure and ensure consistent operation. Additionally, compliance with local regulations regarding air quality and noise emissions should be considered during the system design phase.

About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling solutions. With a focus on innovation and quality, HeadPowder specializes in the design, manufacturing, and installation of positive pressure dilute phase powder conveying systems and related equipment. The company's headquarters is located in Shandong, China, where it leverages its expertise to develop customized solutions tailored to the unique needs of its clients. HeadPowder's commitment to excellence ensures that its products meet the highest industry standards, providing reliable and efficient material handling solutions for a wide range of applications.