

Working Principle and Features of Sintered Ash Pneumatic Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer and supplier of pneumatic conveying systems, specializing in equipment designed for handling sintered ash. Based in Shandong, China, the company has established itself as a leading provider of efficient and reliable solutions for industrial material transport, particularly in the context of sintered ash, a byproduct commonly found in steel and metallurgical processes.
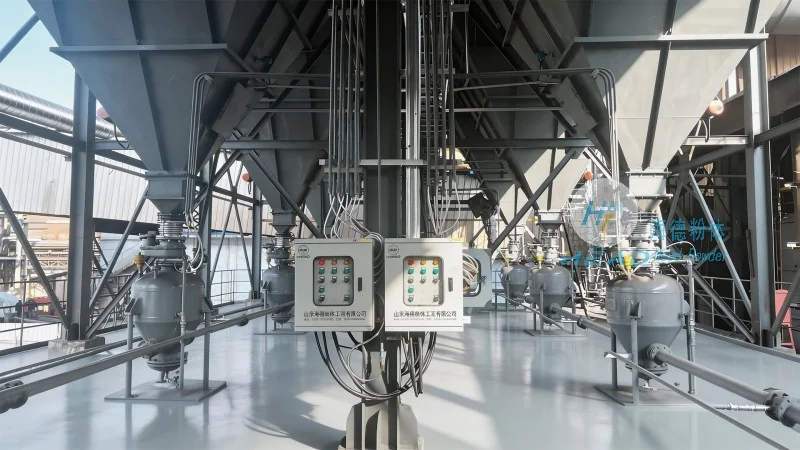
Working Principle of Sintered Ash Pneumatic Conveying Systems
The core of a sintered ash pneumatic conveying system lies in its ability to transport bulk materials like sintered ash through a pipeline using a combination of air and mechanical force. This system typically operates on the principle of pneumatic transport, which can be categorized into two main types: suction and pressure systems. In a suction system, a vacuum is created at the material inlet to draw the sintered ash into the pipeline, where it is then carried by a stream of air. Conversely, a pressure system injects air under pressure into the material at the discharge point, pushing the ash through the pipeline. Both methods rely on the interaction between the air flow and the material particles to achieve efficient transport. The system includes key components such as a hopper for material storage, a feeder to control the flow rate, a pipeline network for material transport, and a separator to separate the material from the air at the discharge end. The air flow is often generated by a blower or a fan, which provides the necessary pressure or vacuum to move the sintered ash. The design of the system is tailored to handle the specific characteristics of sintered ash, including its particle size, density, and moisture content, ensuring optimal performance and minimal material degradation during transport.

Key Features of Sintered Ash Pneumatic Conveying Equipment
HeadPowder's sintered ash pneumatic conveying systems are characterized by several distinct features that enhance their effectiveness and suitability for industrial applications. One of the primary advantages is high efficiency in material transport, as the system can move large volumes of sintered ash over long distances with minimal energy consumption compared to traditional methods like belt conveyors or trucks. This efficiency is achieved through the optimized design of the pipeline network and the air flow control mechanisms. Additionally, the system offers a high degree of flexibility in terms of layout, allowing for integration into existing industrial facilities without major structural modifications. The equipment is also designed with a focus on environmental friendliness, as it eliminates the need for open-air transport, reducing dust emissions and minimizing the impact on the surrounding environment. Another notable feature is the low maintenance requirement, thanks to the use of robust materials and components that are resistant to wear and corrosion from the sintered ash. The system's modular design facilitates easy maintenance and component replacement, reducing downtime and operational costs. Furthermore, the equipment is equipped with advanced control systems that allow for precise regulation of the material flow rate and air pressure, ensuring consistent performance and preventing overloading or blockages in the pipeline. Safety features are also integrated into the design, including pressure relief valves and material flow monitors, to protect against system failures and ensure safe operation. The overall design prioritizes durability and reliability, making it suitable for continuous and high-volume operations in industrial settings.

Application and Benefits in Industrial Settings
The sintered ash pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. are widely used in various industrial applications, particularly in the steel and metallurgical industries where sintered ash is a common byproduct. These systems are employed to transport sintered ash from storage silos or processing units to disposal sites, recycling facilities, or other processing plants. The benefits of using such a system extend beyond mere transport efficiency; they include improved safety by reducing manual handling of the material, enhanced environmental compliance by minimizing dust and emissions, and increased operational productivity by enabling continuous and uninterrupted material flow. The systems are also adaptable to different scales of operation, from small-scale installations in smaller industrial facilities to large-scale systems in major steel plants. The company's expertise in customizing the equipment to meet specific customer requirements ensures that the systems are optimized for the unique needs of each application, whether it involves handling a specific type of sintered ash or operating under particular environmental conditions. Overall, the sintered ash pneumatic conveying systems provide a comprehensive solution for the efficient and reliable transport of sintered ash, contributing to improved operational performance and sustainability in industrial processes.