

Working Principle and Features of Pulse Dust Collector Powder Conveying Machine
The pulse dust collector powder conveying machine is an advanced industrial equipment designed for efficient handling and transportation of powders in various industrial applications. It integrates dust collection and material conveying functions, making it a versatile solution for industries such as chemical, pharmaceutical, food processing, and more. This equipment is engineered to ensure high efficiency, low maintenance, and reliable performance, catering to the diverse needs of modern manufacturing processes.
Working Principle of the Pulse Dust Collector Powder Conveying Machine
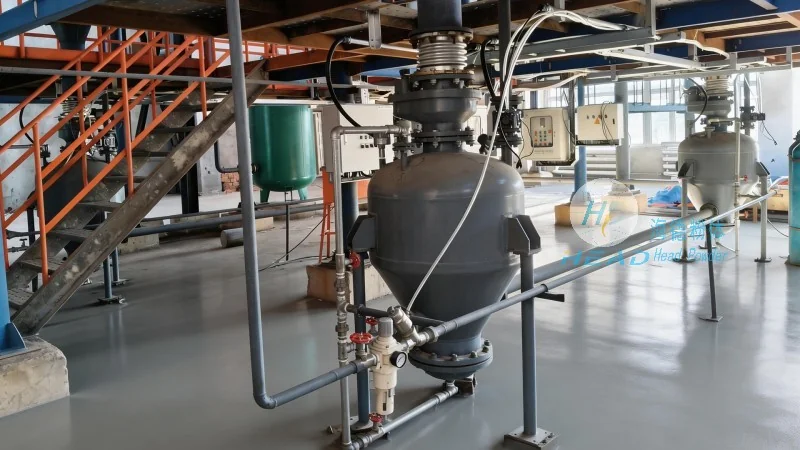
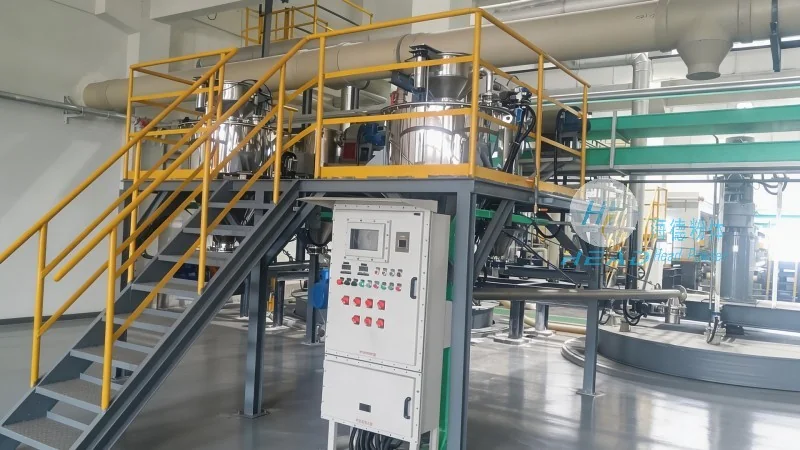
The operation of the pulse dust collector powder conveying machine is based on a combination of dust collection and pneumatic conveying technologies. The machine typically consists of a dust collector unit that captures airborne particles from the production environment, and a conveying system that transports the collected powders to designated storage or processing areas. The core mechanism involves the use of compressed air pulses to create pressure differentials, which facilitate the movement of powders through the conveying lines. The dust collector part uses filtration media to trap dust particles, while the conveying section utilizes air flow to transport the material. The system operates by periodically releasing high-pressure air pulses, which create a vacuum effect that draws the powders into the conveying pipe and moves them towards the collection tank or silo. This process ensures that the powders are transported with minimal loss and high efficiency, while the dust collector simultaneously cleans the air by trapping particulate matter.

Key Features and Advantages
Several notable features distinguish the pulse dust collector powder conveying machine from conventional conveying systems. Firstly, its integrated design combines dust collection and material handling, reducing the need for separate equipment and optimizing space utilization. The machine offers high conveying efficiency, capable of transporting powders over long distances with minimal pressure drop. The pulse control system ensures stable and consistent material flow, preventing blockages and ensuring smooth operation. Additionally, the equipment is equipped with advanced filtration systems that maintain high air quality, meeting environmental regulations and ensuring compliance with industrial standards. The machine also features low energy consumption, as the compressed air pulses are optimized to minimize power usage while maintaining performance. Maintenance is simplified due to its modular design, allowing for easy access to components for inspection and replacement. The robust construction ensures durability and long service life, making it a reliable choice for continuous industrial operations.

Company Information
HeadPowder, a leading manufacturer in the field of industrial powder handling equipment, specializes in the design, development, and production of high-quality pulse dust collector powder conveying machines. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries seeking efficient and reliable solutions for powder handling. HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, leverages advanced engineering and manufacturing capabilities to deliver products that meet international standards and customer requirements. The company's focus on research and development ensures that its equipment remains at the forefront of technological advancements, providing customers with cutting-edge solutions that enhance productivity and operational efficiency.