

Principle and Working Scene Characteristics of Cement Raw Material Powder Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the development and supply of advanced powder conveying systems for the cement industry. The company's core product, the cement raw material powder conveying system equipment, is engineered to meet the rigorous demands of material handling in cement production facilities. This system is essential for efficiently transporting bulk powders such as limestone, clay, and iron ore—key raw materials in the cement manufacturing process.
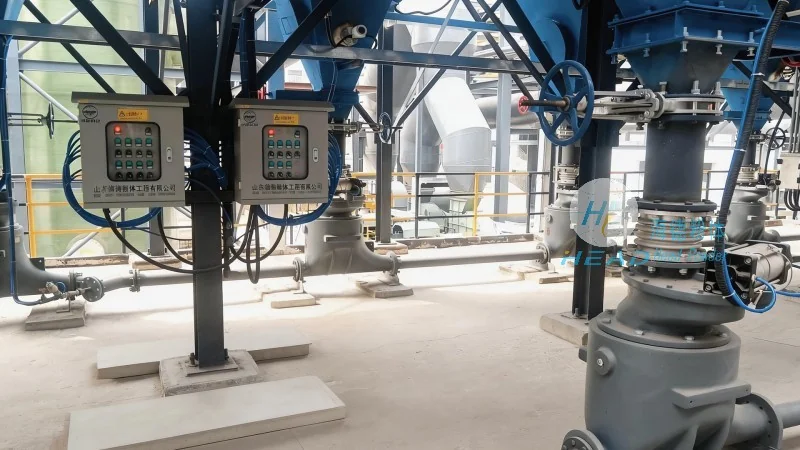
Principle of the Cement Raw Material Powder Conveying System
The cement raw material powder conveying system operates on either pneumatic or mechanical transport principles, depending on the specific design and application requirements. Pneumatic systems utilize air as the medium to move powders through pipelines, typically comprising a hopper for material storage, a feeder to regulate flow rate, a blower or compressor to generate air pressure, and a pipeline network for material delivery. Mechanical systems, conversely, rely on screw conveyors, belt conveyors, or bucket elevators to transport powders. These are often preferred for abrasive or high-capacity material handling scenarios.

Working Scene Characteristics
The working scene characteristics of the cement raw material powder conveying system are tailored to the harsh and demanding environments of cement production. These systems are engineered for high efficiency, large material volumes, and minimal downtime. Key characteristics include:

- High Capacity and Consistency: The system is capable of transporting substantial quantities of raw materials at steady speeds, ensuring smooth production flow in cement plants.
- Durability and Low Maintenance: Constructed with high-quality materials and robust components, the equipment withstands dust, moisture, and abrasive particles common in cement production, reducing maintenance needs.
- Customization and Flexibility: Shandong HeadPowder Engineering Co., Ltd. offers tailored solutions to accommodate varying production scales and material types, ensuring optimal performance for each client.
- Energy Efficiency: Modern designs incorporate energy-saving features like variable speed drives and optimized air flow, reducing operational costs while maintaining performance.
Application Scenarios
The cement raw material powder conveying system is widely used across cement production stages, including raw material storage, pre-homogenization, and feeding to the rotary kiln. In storage, the system efficiently moves limestone and other raw materials from stockpiles to silos. During pre-homogenization, it ensures uniform mixing of raw materials to enhance final cement quality. Finally, in the feeding stage, the system delivers homogenized materials to the kiln at controlled rates, optimizing combustion and energy efficiency.
Advantages in Cement Production
Implementing the cement raw material powder conveying system from Shandong HeadPowder Engineering Co., Ltd. offers significant advantages to cement manufacturers. These include improved production efficiency, reduced labor costs, and enhanced product quality. The system minimizes human intervention, reducing material loss or contamination risks. Additionally, its durability and low maintenance contribute to long-term cost savings and operational reliability.

Conclusion
Shandong HeadPowder Engineering Co., Ltd.'s cement raw material powder conveying system equipment is a critical component in modern cement production. By leveraging advanced engineering and robust design, the system ensures efficient, reliable, and cost-effective transport of raw materials. The company's commitment to customization ensures each system meets specific client needs, supporting overall productivity and success in cement manufacturing operations.