

Principle and Working Scene Characteristics of Iron Concentrate Material Handling System Equipment
Iron concentrate, a vital raw material in the steel industry, demands efficient and reliable handling systems to support seamless production processes. The iron concentrate material handling system equipment developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder) is engineered to meet the specific transportation, storage, and processing needs of iron concentrate. This system integrates advanced technology and robust engineering to optimize material flow and enhance operational efficiency in industrial settings.

Principle of the Iron Concentrate Material Handling System
The fundamental principle of the iron concentrate material handling system is to facilitate the seamless transfer of iron concentrate from one location to another within industrial facilities. The system typically combines conveyor belts, hoppers, and control mechanisms to manage material flow. Conveyor belts are engineered to handle the bulk density and abrasive nature of iron concentrate, ensuring minimal wear while maintaining high throughput. Hoppers are strategically placed to store and regulate material flow, preventing blockages and ensuring consistent feeding to downstream processing equipment. Control systems, often integrated with sensors and automation technology, monitor performance in real-time, adjusting parameters such as speed and pressure to maintain optimal operation. This integrated approach ensures efficient operation, reducing downtime and improving overall productivity.

Working Scene Characteristics of the Iron Concentrate Material Handling System
The iron concentrate material handling system is tailored to operate in diverse industrial environments, adapting to the specific requirements of each application. In mining and processing plants, the system handles large volumes of iron concentrate under harsh conditions with high dust and moisture levels. Constructed with durable materials like stainless steel and heavy-duty polymers, the equipment withstands the corrosive and abrasive properties of iron concentrate. The system's modular design allows for easy installation and integration into existing infrastructure, minimizing operational disruption. Safety features, including emergency stop mechanisms and overload protection, ensure personnel and equipment safety. The working scene characteristics also include the ability to handle varying particle sizes and moisture content, making it suitable for different stages of iron concentrate processing—from raw material handling to intermediate storage and final transfer to smelting facilities.
Key Features and Benefits of the Iron Concentrate Material Handling System
Shandong HeadPowder Engineering Co., Ltd. has incorporated several key features into the iron concentrate material handling system to enhance performance and reliability. High-capacity conveyor belts with reinforced edges prevent material spillage and ensure consistent flow. Hoppers are designed with sloped walls and discharge chutes to facilitate smooth material discharge, reducing blockage risks. Automation and control systems provide real-time monitoring and adjustment, allowing operators to optimize performance based on production needs. Maintenance-friendly components, such as easy-to-access bearings and replaceable parts, minimize downtime during maintenance. Benefits include improved operational efficiency, reduced labor costs, enhanced safety, and extended equipment lifespan. By streamlining material handling, the system contributes to cost savings and increased productivity in iron concentrate processing operations.
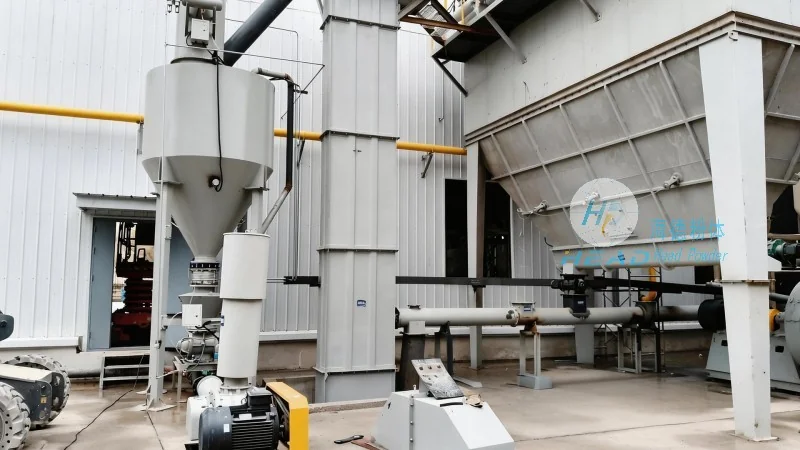
Application Scenarios and Operational Efficiency
The iron concentrate material handling system is widely used in various industrial applications, including mining, steel production, and recycling facilities. In mining operations, it transports iron concentrate from ore processing plants to storage silos or directly to smelting furnaces. The system's ability to handle large volumes and maintain consistent flow ensures uninterrupted production. In steel production facilities, it integrates into the raw material handling stage, combining iron concentrate with other materials for steel production. Efficient material flow and storage support a steady raw material supply, enabling continuous production. Additionally, the system is used in recycling plants to handle recycled iron concentrate, promoting sustainable industrial practices. Operational efficiency is further enhanced by adaptability to varying material characteristics and environmental factors. By optimizing material flow and reducing handling time, the system boosts overall productivity, making it a critical component in modern iron concentrate processing.