

Principles and Application Scenarios of Dust-Free Material Feeding with Pneumatic Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in advanced material handling solutions. This article explores the fundamental principles of dust-free material feeding using pneumatic conveying systems, alongside an analysis of key application scenarios that highlight the technology's effectiveness and versatility.

Principles of Pneumatic Conveying for Dust-Free Material Handling
Pneumatic conveying systems operate by transporting bulk materials through a closed pipeline using air or gas as the conveying medium. In the context of dust-free material feeding, these systems are designed to minimize particle generation and ensure a clean, controlled transfer process. The core principle involves creating a pressure differential within the pipeline, which propels the material from the source to the destination. Key components include the feed hopper, airlock, conveying line, and receiver, all working in tandem to maintain a dust-free environment. The system's design often incorporates features such as vacuum or pressure modes, with vacuum being preferred for material withdrawal from hoppers or silos, and pressure for material transfer to higher elevations or distant locations.
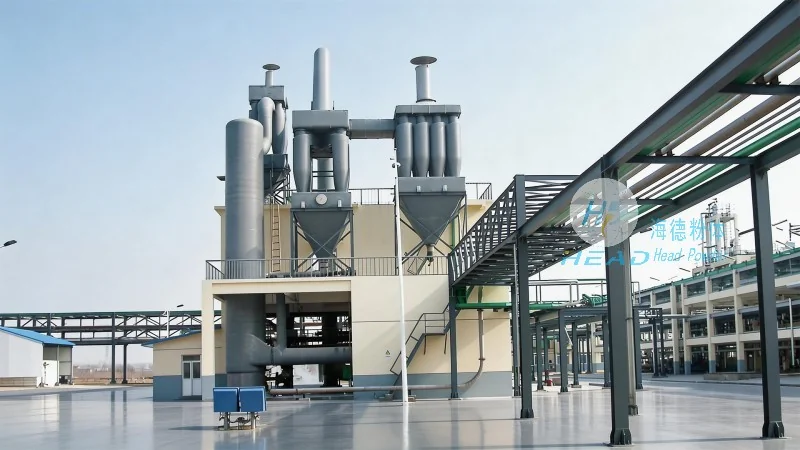
Key Application Scenarios of Dust-Free Material Feeding Systems
Dust-free material feeding via pneumatic conveying is widely utilized across various industries, including pharmaceuticals, food processing, and chemical manufacturing. In pharmaceutical applications, the technology ensures compliance with stringent regulatory standards by preventing contamination and maintaining product purity. The systems are engineered to handle sensitive powders, such as active pharmaceutical ingredients (APIs) and excipients, with minimal particle generation. In food processing, the dust-free design is crucial for maintaining hygiene and preventing cross-contamination, making it ideal for handling ingredients like flour, sugar, and spices. Chemical manufacturers benefit from the ability to transfer hazardous or reactive powders safely, reducing the risk of dust explosions and ensuring workplace safety. Additionally, the technology is employed in industrial settings where material handling efficiency and cleanliness are critical, such as in cement production, where bulk materials are transferred between storage silos and processing equipment.

Advantages of Pneumatic Conveying in Dust-Free Material Feeding
The adoption of pneumatic conveying systems for dust-free material feeding offers several advantages over traditional methods like belt conveyors or manual handling. One of the primary benefits is the elimination of dust generation, which not only improves workplace safety by reducing respiratory hazards but also enhances product quality by preventing contamination. The closed pipeline design ensures that materials remain contained throughout the transfer process, minimizing environmental impact and adhering to environmental regulations. Furthermore, pneumatic conveying systems are highly flexible, allowing for easy integration with existing production lines and the ability to handle a wide range of material types, from fine powders to granules. The technology also offers improved efficiency, as materials can be transferred at high speeds and over long distances with minimal energy consumption compared to other methods. Another advantage is the reduced need for maintenance, as the system's components are designed to withstand the rigors of continuous operation without frequent replacement.

HeadPowder's Expertise in Dust-Free Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a trusted provider of customized pneumatic conveying solutions tailored to the specific needs of various industries. The company leverages advanced engineering and manufacturing capabilities to design and install systems that meet the highest standards of efficiency, reliability, and safety. HeadPowder's team of experienced engineers works closely with clients to assess their material handling requirements, providing tailored solutions that optimize process flow and minimize operational costs. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols, ensuring that each system is built to deliver long-term performance and durability. With a focus on innovation and customer satisfaction, HeadPowder continues to be a leader in the development of dust-free material feeding technologies, helping businesses across the globe achieve cleaner, more efficient material handling processes.