

Operation Process and Working Principle of Camellia Seed Powder Pneumatic Conveying Line
Camellia seed powder, a valuable byproduct from the processing of camellia seeds, often requires efficient and reliable handling systems for transport and processing. The pneumatic conveying line developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder) addresses these needs by providing a robust solution for the movement of fine powders like camellia seed powder. This article explores the operation process and working principle of such a system, highlighting its key components and operational dynamics.

Key Components of the Pneumatic Conveying System
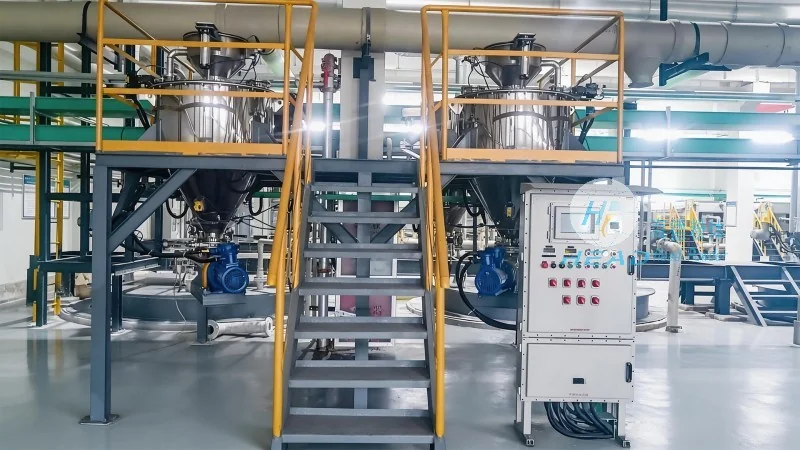
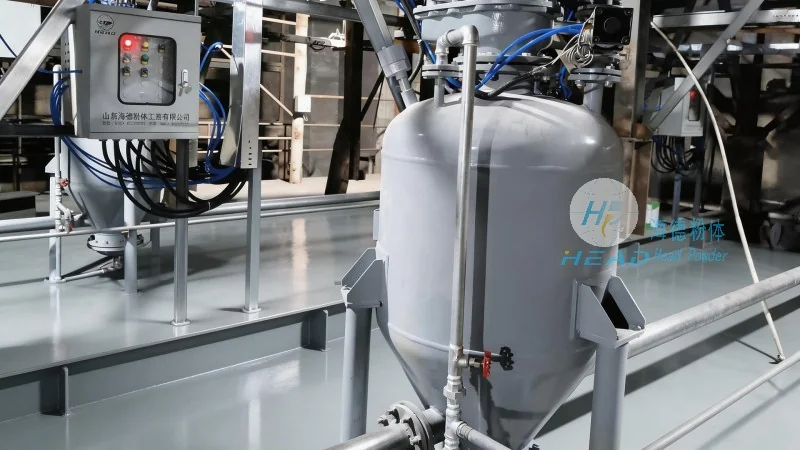
The pneumatic conveying line for camellia seed powder typically consists of several critical components that work in concert to ensure efficient material transport. These include the hopper for material storage, a rotary valve for controlled discharge, a conveying pipeline network, a blower or air compressor to generate the necessary air pressure, and a receiver or collection tank at the destination. Each component plays a vital role in maintaining the integrity of the powder and the efficiency of the conveying process.
Working Principle of the Pneumatic Conveying Process
The operation of the camellia seed powder pneumatic conveying line is based on the principle of transporting bulk materials through a pipeline using a stream of air. When the system is activated, the blower generates a high-pressure air flow that is introduced into the conveying pipeline. Simultaneously, the rotary valve in the hopper opens to allow camellia seed powder to enter the pipeline. The air stream then lifts and propels the powder particles through the pipeline to the receiver. The velocity and pressure of the air are carefully controlled to ensure that the powder is conveyed without degradation, clogging, or excessive energy consumption.

Operation Process: Step-by-Step Overview
The operation of the pneumatic conveying line follows a systematic sequence to ensure smooth and continuous material transport. The process begins with the loading of camellia seed powder into the hopper. The rotary valve then regulates the flow rate of the powder into the pipeline. The blower maintains a consistent air pressure and flow rate, which is crucial for maintaining the conveying velocity. As the powder travels through the pipeline, it reaches the receiver where it is collected. The system may also include a filter or separator to remove any entrained air or fine particles before the powder is discharged from the receiver. This step-by-step process ensures that the entire operation is efficient and reliable, minimizing downtime and maximizing throughput.
Advantages of the Pneumatic Conveying System
Implementing a pneumatic conveying line for camellia seed powder offers several advantages over traditional mechanical conveying methods. These include reduced risk of product contamination, as the material is enclosed within the pipeline, preventing exposure to external elements. Additionally, the system is capable of handling fine powders without the need for additional equipment like buckets or belts, which can cause clogging or degradation. The energy efficiency of the system, particularly with optimized air pressure and flow rates, also contributes to lower operational costs. Furthermore, the flexibility of the pipeline network allows for easy reconfiguration or expansion of the conveying system as production needs change.
Conclusion and Company Information
The pneumatic conveying line for camellia seed powder, as developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution for the efficient handling of fine powders. By understanding the operation process and working principle of this system, users can appreciate the benefits of enclosed, energy-efficient transport. With its robust design and careful engineering, the system ensures reliable performance and minimal maintenance, making it an ideal choice for industries dealing with camellia seed powder. HeadPowder, based in Shandong, China, continues to innovate in powder handling technology, providing tailored solutions that meet the specific needs of its clients.