

[H1]High-Pressure Bin Pump Pneumatic Conveying System: An Overview of Its Structure and Working Prin
High-pressure bin pumps represent a critical advancement in industrial material handling, offering efficient and reliable pneumatic conveying solutions for diverse bulk materials. This article provides a comprehensive overview of the high-pressure bin pump system, detailing its structural components and the fundamental principles that enable its operation within industrial settings.

Key Structural Components of the High-Pressure Bin Pump System
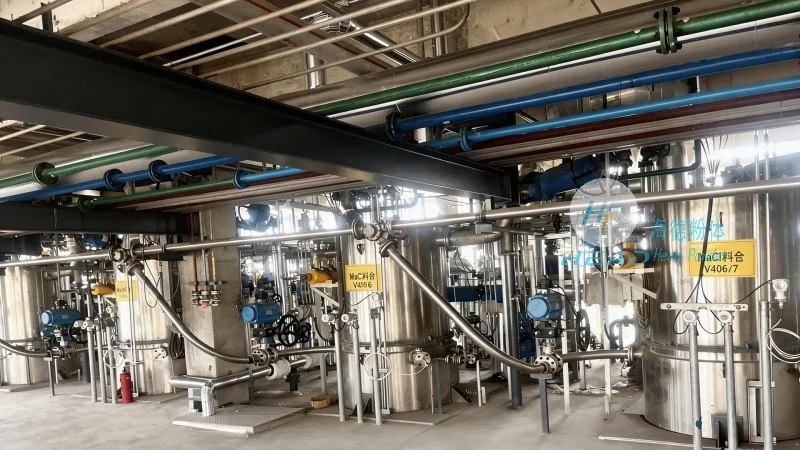
The high-pressure bin pump system comprises several integral components that work in concert to facilitate material transport. The primary elements include the bin pump (pressure vessel), inlet hopper, gasification unit, pressure control system, conveying pipeline, and discharge outlet. Each component is meticulously designed to ensure optimal performance and durability under high-pressure conditions.
The bin pump, often referred to as the pressure vessel, serves as the central storage and pressurization unit. Constructed from robust materials such as stainless steel or carbon steel, it is engineered to withstand significant internal pressures. The inlet hopper is responsible for receiving bulk materials from a primary storage silo or hopper, ensuring a continuous and unobstructed feed into the bin pump. The gasification unit, typically equipped with a high-pressure air compressor or blower, generates the necessary air pressure to create a pneumatic flow within the system.
The pressure control system regulates the pressure and flow rate within the bin pump, maintaining consistent operational parameters. The conveying pipeline transports the material-air mixture from the bin pump to the discharge point, with the discharge outlet directing the material to its final destination, such as a processing plant or storage facility. Together, these components form a cohesive system capable of handling a wide range of materials, including powders, granules, and even wet or sticky substances.
The Working Principle of High-Pressure Bin Pump Systems
The operation of the high-pressure bin pump system is based on the principle of pneumatic conveying, where materials are transported through a pipeline using a gas medium, most commonly air. The process begins with the loading of bulk material into the inlet hopper, which then flows into the bin pump. The gasification unit then injects high-pressure air into the bin pump, creating a high-pressure environment.
As the air and material mixture is pressurized, it is forced through the discharge outlet and into the conveying pipeline. The pressure differential between the bin pump and the discharge point drives the material forward through the pipeline. The high-pressure air acts as a carrier, suspending the material particles and transporting them to the destination. The control system plays a crucial role in maintaining the pressure and flow rate, ensuring consistent and efficient material transport. This system can handle various materials, from fine powders to larger granules, making it versatile for different industrial applications.

Introduction to Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of pneumatic conveying systems, specializes in the design, manufacturing, and installation of high-pressure bin pump systems. With a strong commitment to quality and innovation, HeadPowder has established itself as a trusted partner for industries requiring reliable material handling solutions. The company is headquartered in Shandong, China, and serves clients globally with its advanced technology and customer-centric approach.
HeadPowder's high-pressure bin pump systems are engineered to meet the specific needs of various industries, including chemical, food, pharmaceutical, and mining. The company's team of experienced engineers and technicians ensures that each system is tailored to the client's requirements, providing optimal performance and efficiency. With a focus on durability and reliability, HeadPowder's products are built to withstand the rigors of industrial use, delivering long-term value to its customers.
Located in Shandong, China, HeadPowder leverages its local expertise and resources to deliver high-quality products and services. The company's facilities are equipped with state-of-the-art manufacturing equipment and testing facilities, ensuring that every product meets the highest standards of quality and safety. HeadPowder's dedication to customer satisfaction and technical excellence has earned it a reputation as a leading provider of pneumatic conveying solutions in the industry.