

What is a Ton Bag Powder Conveying Machine? And What Are Its Design Principles?
Welcome to the world of bulk material handling, where efficiency and precision are paramount. In this article, we delve into the specifics of ton bag powder conveying machines, exploring their functionality and the intricate design principles that underpin their operation. As a key component in industrial processes, these machines are essential for the seamless transfer of bulk powders from storage to processing units. Let's explore what they are and how they work.
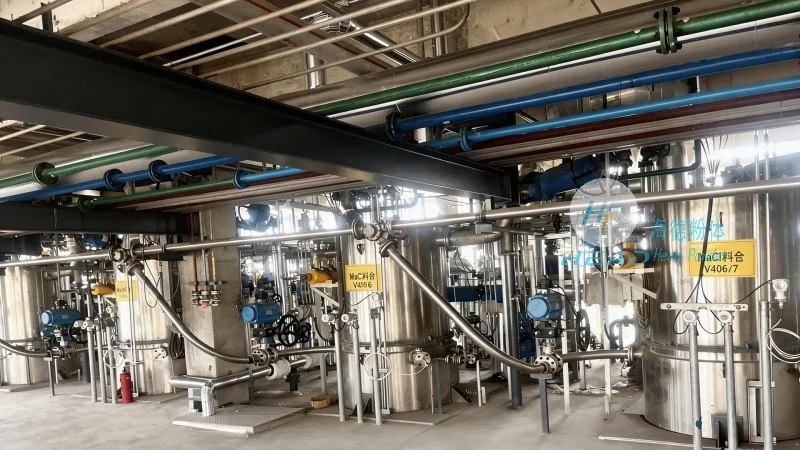
Understanding Ton Bag Powder Conveying Machines
A ton bag powder conveying machine is a specialized piece of equipment designed to handle and transport bulk powders from large ton bags into processing systems. These machines are commonly used in industries such as food processing, pharmaceuticals, chemicals, and mining, where the safe and efficient transfer of powders is critical. The primary goal of these systems is to minimize dust generation, ensure product integrity, and maintain a clean, controlled environment throughout the transfer process.

The Core Components and Functionality
At the heart of a ton bag powder conveying machine are several key components that work in tandem to achieve effective material handling. The main parts include a hopper or receiving chamber, a conveyor system (often pneumatic or mechanical), a discharge mechanism, and a dust collection system. The receiving chamber is typically designed to accommodate the ton bag, allowing for easy opening and material discharge. The conveyor system, which may be a pneumatic pipeline or a mechanical screw conveyor, transports the powder from the hopper to the processing unit. The discharge mechanism ensures that the material is released into the next stage of the process without spillage or loss. Additionally, a dust collection system is integrated to capture any airborne particles, maintaining a safe and clean working environment.

Design Principles and Key Considerations
The design of ton bag powder conveying machines is guided by several critical principles to ensure optimal performance and safety. One of the most important considerations is the need for airtight and dust-tight construction to prevent material leakage and environmental contamination. This is achieved through the use of high-quality seals, gaskets, and robust materials that can withstand the pressures and temperatures associated with bulk powder handling. Another key design principle is the optimization of material flow and pressure drop within the system. Engineers carefully calculate the dimensions of the conveyor pipes, the speed of the conveyor, and the pressure of the air or mechanical force to ensure that the powder moves smoothly and efficiently without clogging or excessive energy consumption. Furthermore, the design must account for the specific properties of the powder being handled, such as its density, flowability, and potential for static charge. For powders that are prone to static, anti-static measures are incorporated into the design to prevent buildup and ensure safe operation. The system is also designed for easy maintenance and cleaning, with features like removable components and easy access to internal parts, which helps to minimize downtime and maintain consistent performance.
Applications and Benefits in Industrial Settings
Ton bag powder conveying machines are widely used across various industrial sectors due to their versatility and efficiency. In the food industry, they are used to transfer ingredients such as flour, sugar, and spices from bulk storage to production lines, ensuring that the products remain fresh and free from contamination. In the pharmaceutical industry, these machines are crucial for handling active pharmaceutical ingredients (APIs) and other sensitive materials, where precision and sterility are paramount. In the chemical industry, they are used to transport raw materials and finished products, helping to streamline production processes and reduce waste. The benefits of using ton bag powder conveying machines include improved safety through reduced dust exposure, increased efficiency through faster material transfer, and enhanced product quality through better control over the handling process. Additionally, these systems can be integrated with other equipment, such as mixers and reactors, to create a fully automated material handling line, further enhancing operational efficiency.

Conclusion and Company Overview
In conclusion, ton bag powder conveying machines are sophisticated devices that play a vital role in modern industrial operations. Their design, which prioritizes safety, efficiency, and material integrity, makes them indispensable in industries where bulk powder handling is a daily necessity. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality, customized solutions for bulk material handling. With a focus on innovation and customer satisfaction, the company offers a range of ton bag powder conveying machines that are tailored to meet the specific needs of different industries. Whether you are in the food, pharmaceutical, chemical, or mining sector, a ton bag powder conveying machine from Shandong HeadPowder Engineering Co., Ltd. can help you achieve efficient, safe, and reliable material transfer. For more information on their products and services, please visit their official website or contact their sales team.