

What is a Potassium Sulfate Powder Conveyor? What is its Design Principle?
For industrial applications involving the handling of potassium sulfate, a specialized type of conveyor system is often employed. This equipment, commonly known as a potassium sulfate powder conveyor, is designed to efficiently transport bulk powder materials. The primary function of such a conveyor is to move potassium sulfate from one location to another within a processing facility, ensuring smooth and continuous operation in various industrial processes. Understanding the design and operational principles of this equipment is crucial for optimizing material handling efficiency and maintaining product quality.

Key Features of Potassium Sulfate Powder Conveyors
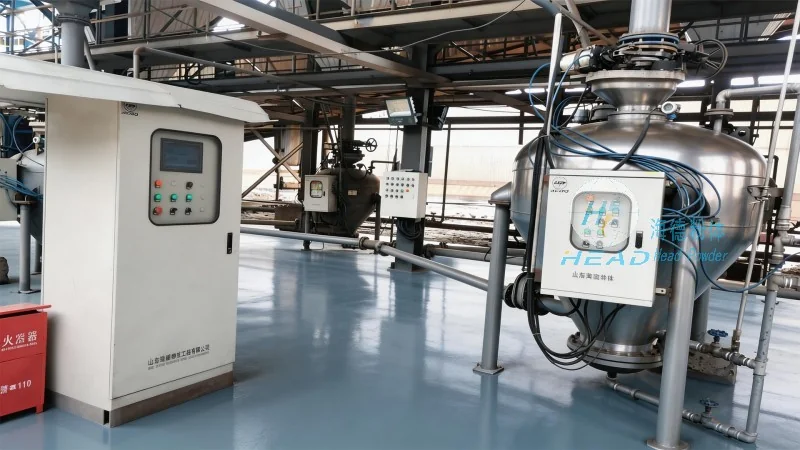
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of high-quality powder conveyors. Their potassium sulfate powder conveyors are engineered with several key features that enhance performance and reliability. These features include robust construction to withstand the abrasive nature of potassium sulfate, precise control systems for accurate material flow, and efficient sealing mechanisms to prevent dust leakage and contamination. The conveyors are also designed to minimize material degradation during transport, which is critical for maintaining the purity and quality of the potassium sulfate product. Additionally, the equipment is built to meet international safety and environmental standards, ensuring compliance in various industrial settings.

Design Principles of Potassium Sulfate Powder Conveyors
The design of a potassium sulfate powder conveyor is based on several fundamental principles that address the unique characteristics of the material being handled. First, the conveyor must be able to handle the bulk density and flow properties of potassium sulfate, which can vary depending on moisture content and particle size. The design incorporates components such as feed hoppers and discharge chutes that are optimized to control the flow rate and prevent clogging. Second, the material of construction is critical; the conveyor is typically made from corrosion-resistant materials like stainless steel or specialized alloys to resist the chemical properties of potassium sulfate and prevent degradation over time. Third, the system includes advanced control mechanisms, such as variable speed drives and level sensors, to regulate the conveyor's operation and ensure consistent material transport. These controls help maintain a stable flow rate, reducing the risk of overloading or underloading the conveyor. Fourth, the design emphasizes energy efficiency, with features like low-friction components and optimized motor sizing to minimize power consumption while maintaining performance. Finally, the conveyor is designed for easy maintenance and cleaning, with accessible components and sealed joints to facilitate regular upkeep and prevent contamination.

Applications and Benefits in Industrial Settings
Potassium sulfate powder conveyors are widely used in various industrial applications where bulk powder handling is required. These include fertilizer production, chemical processing, and food processing industries. In fertilizer production, the conveyor is used to transport potassium sulfate from storage silos to blending and packaging equipment, ensuring a continuous supply of raw material. In chemical processing, the equipment is used to move potassium sulfate between different processing stages, such as drying, grinding, and mixing. The benefits of using a specialized conveyor for potassium sulfate include improved operational efficiency, reduced labor costs, and enhanced product quality. The equipment allows for precise control over material flow, minimizing waste and optimizing production output. Additionally, the use of a conveyor reduces the risk of dust exposure and improves workplace safety by containing the material within the system. The reliability of the conveyor also contributes to reduced downtime and maintenance costs, making it a cost-effective solution for industrial operations.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd. is a reputable company based in Shandong, China, dedicated to providing high-quality powder handling solutions. Their potassium sulfate powder conveyors are designed with the latest engineering principles to meet the demands of modern industrial applications. The company's commitment to quality, reliability, and customer satisfaction has made them a trusted partner in the industry. By leveraging advanced design and manufacturing techniques, HeadPowder ensures that their conveyors are efficient, durable, and suitable for handling potassium sulfate and other similar bulk materials. The company's products are backed by a team of experienced engineers and technicians who provide technical support and maintenance services to ensure optimal performance. With a focus on innovation and customer needs, HeadPowder continues to be a leader in the powder conveyor industry, providing solutions that enhance operational efficiency and product quality for their clients.