

Working Principle and Features of an Alumina Particle Pneumatic Conveying System
The alumina particle pneumatic conveying system is a sophisticated industrial solution engineered to efficiently transport alumina particles, a critical material in various manufacturing processes. This system is specifically designed to address the unique challenges associated with handling alumina, such as its high density, abrasive nature, and tendency to generate dust. By utilizing pneumatic conveying technology, the system ensures the safe, clean, and efficient movement of alumina particles from the source to the destination, minimizing material loss and contamination. The system is widely used in applications like alumina production, processing, and distribution, where maintaining the integrity of the material is paramount for downstream operations. Its design integrates advanced engineering principles to optimize performance, reliability, and operational efficiency, making it an essential component in modern industrial facilities.
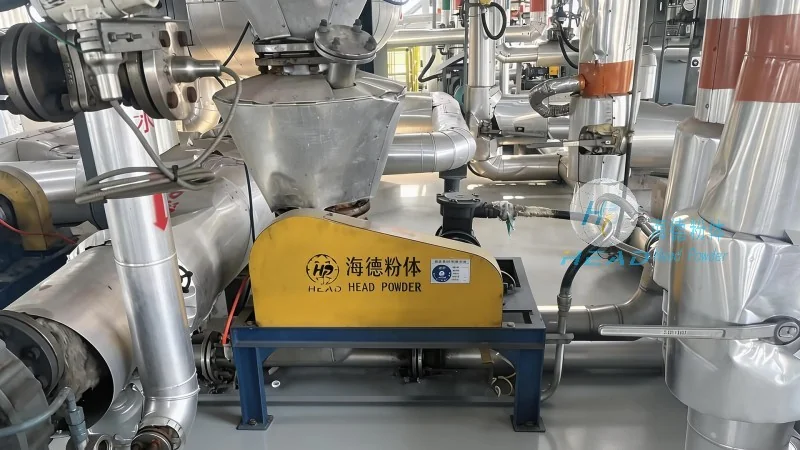

Working Principle of the Pneumatic Conveying System
The fundamental operation of the alumina particle pneumatic conveying system relies on the principle of air flow to transport solid particles. The process begins with the loading of alumina particles into a hopper or feeder, which acts as the initial storage and feeding unit. The feeder then regulates the flow of particles into the conveying line, ensuring a consistent and controlled feed rate. Compressed air is then introduced into the system, typically through a blower or compressor, creating a high-pressure air stream that propels the particles through the pipeline. The system may employ different conveying modes, including dilute phase and dense phase, each tailored to specific material and application requirements. In dilute phase conveying, the particles are suspended in the air stream, traveling at higher velocities and over longer distances. This mode is suitable for transporting particles with lower density and smaller particle sizes. In contrast, dense phase conveying involves a more concentrated flow of particles, often with lower air velocity and higher air pressure. This mode is ideal for handling abrasive or sensitive materials, as it reduces particle impact and wear on the pipeline and equipment. The system's control system monitors and adjusts the air pressure, flow rate, and particle feed, ensuring optimal performance and preventing operational issues such as clogging or blockages. The entire process is designed to maintain the quality of the alumina particles, preventing degradation or contamination during transport.

Key Features and Advantages of the System
The alumina particle pneumatic conveying system offers a range of key features and advantages that make it a preferred choice for industrial applications. One of the primary benefits is its ability to transport alumina particles over long distances with minimal material loss and contamination. The system's design minimizes the risk of particle degradation, ensuring that the material reaches its destination in the same condition as when it was loaded. This is particularly important for high-value alumina applications, where product quality is critical. Another significant advantage is the system's ability to handle abrasive materials, reducing wear and tear on components and extending the service life of the equipment. The system's components, such as the pipeline, valves, and fittings, are constructed from durable materials like stainless steel or special alloys, which resist corrosion and wear from alumina particles. The system also provides a dust-free and clean operation environment, which is essential for maintaining product quality and complying with environmental regulations. This feature is achieved through the sealed design of the system, which prevents dust emissions and ensures that the material is transported in a controlled manner. The flexibility of the system allows for easy integration into existing industrial processes, with options for varying conveying capacities and distances. This adaptability makes the system suitable for a wide range of applications, from small-scale laboratory operations to large-scale industrial production. Additionally, the system features advanced control systems that monitor and regulate the air pressure, flow rate, and particle feed, ensuring optimal performance and preventing operational issues. These controls can be adjusted based on the specific requirements of the application, providing a customized solution for each client. The system's low maintenance requirements and energy efficiency further contribute to its cost-effectiveness, making it a sustainable and economical choice for material handling.

About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a leading manufacturer and supplier of pneumatic conveying systems and related industrial equipment. With a strong commitment to innovation and quality, the company specializes in designing and manufacturing customized solutions for various powder and particle handling applications. HeadPowder's team of experienced engineers and technicians work closely with clients to understand their specific needs and develop tailored systems that meet their operational requirements. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and a research and development center. This facility is equipped with advanced machinery and technology, enabling the company to produce high-quality, reliable systems that meet international standards. HeadPowder's systems are designed to deliver consistent performance, energy efficiency, and long-term durability, ensuring that clients receive a return on their investment. The company serves a diverse range of industries, including chemical, pharmaceutical, food, mining, and manufacturing, providing comprehensive solutions for material handling challenges. HeadPowder's products are known for their robust construction, advanced features, and excellent customer support. The company's focus on customer satisfaction and technical excellence has established it as a trusted partner in the industry. With a global presence and a reputation for quality, HeadPowder continues to innovate and provide cutting-edge solutions for the ever-evolving needs of the industrial sector.