

Introduction to Lightweight Cement Pneumatic Conveying Systems: Structure and Working Principles
HeadPowder, the abbreviation for Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier of pneumatic conveying equipment. The company is headquartered in Shandong, China, and specializes in the design, development, and production of advanced pneumatic conveying systems tailored for various industrial applications. With a focus on innovation and quality, HeadPowder provides reliable solutions for material handling, particularly in the cement industry.

Lightweight Cement Pneumatic Conveying Systems
Our lightweight cement pneumatic conveying systems are engineered to efficiently transport lightweight cement and similar powders over long distances with minimal energy consumption. The systems utilize air as the primary conveying medium, ensuring a clean and dust-free operation while maintaining high material transfer efficiency. Key features include adjustable air pressure control, flexible pipeline configurations, and robust material handling capabilities, making them suitable for both new installations and retrofitting existing production lines.

System Structure and Working Principles
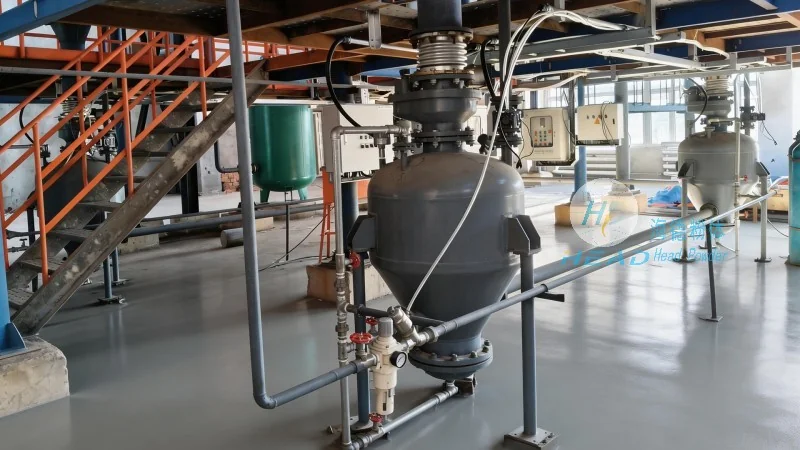
The core components of our pneumatic conveying system include a feeding hopper, a rotary valve, a conveying pipeline, a dust collector, and a discharge outlet. The process begins with the material being fed into the hopper, where it is then discharged into the pipeline through the rotary valve. Compressed air is introduced into the pipeline, creating a flow that propels the material forward. The dust collector is integrated to capture any airborne particles, ensuring environmental compliance and operational safety. The system’s design optimizes air flow and material distribution, minimizing pressure losses and maximizing conveying efficiency.
Advantages and Applications
These systems offer several advantages, including low maintenance requirements, reduced labor costs, and the ability to handle materials in a closed environment, which enhances safety and product quality. They are widely used in cement production plants, construction material processing facilities, and other industries where the efficient transport of lightweight powders is critical. The modular design allows for easy integration into existing production workflows, and the system’s scalability enables it to accommodate varying production volumes and material types.