

Bicarbonate of Soda Pneumatic Conveying System Solution
HeadPowder, a leading provider in the field, offers comprehensive solutions for the efficient and reliable transportation of bicarbonate of soda through pneumatic conveying systems. This article provides an in-depth look at the system design, operational principles, and practical applications, ensuring readers gain a thorough understanding of how such systems enhance material handling processes.

Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, operating from Shandong, China, specializes in engineering and manufacturing advanced pneumatic conveying systems tailored for various industrial needs. With a focus on quality and innovation, the company has established itself as a trusted partner for businesses requiring robust and efficient material transport solutions.
Key Components of the Pneumatic Conveying System
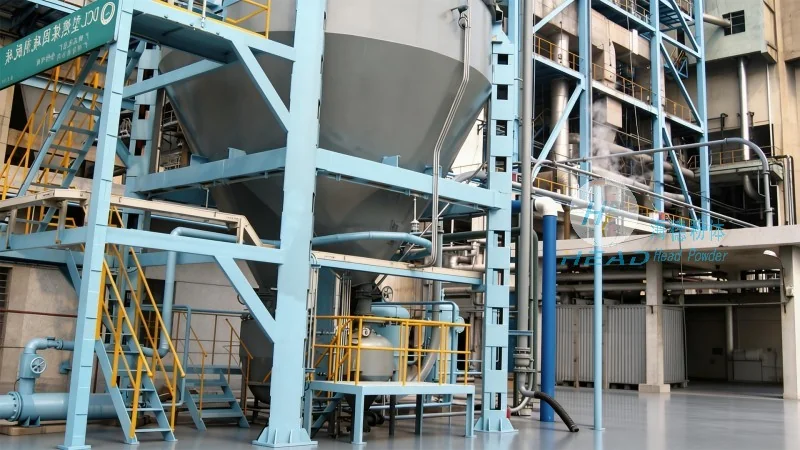
The bicarbonate of soda pneumatic conveying system typically consists of several critical components that work in tandem to ensure smooth operation. These include the material hopper, which holds the bulk bicarbonate of soda, and the air supply system, responsible for generating the necessary pressure to move the material. The conveying line, often equipped with specialized pipes and valves, facilitates the transport of the material from the source to the destination. Additionally, the system may incorporate dust collection and filtration equipment to maintain air quality and comply with environmental regulations. Each component is designed to handle the specific characteristics of bicarbonate of soda, such as its fine particle size and potential for caking, ensuring optimal performance and minimal downtime.

Operational Principles and Efficiency
The pneumatic conveying system operates on the principle of using air pressure to transport solid materials. In the case of bicarbonate of soda, the system generates a flow of air that entrains the powder particles, creating a slurry-like mixture that travels through the conveying line. This method is particularly effective for materials that are difficult to handle using traditional mechanical methods, as it minimizes material degradation and reduces the risk of blockages. The efficiency of the system is enhanced by the use of appropriate air velocities and pressure levels, which are carefully calibrated to match the properties of the material being conveyed. By optimizing these parameters, the system can achieve high throughput rates while maintaining low energy consumption, making it a cost-effective solution for industrial applications.
Applications and Industry Use Cases
Bicarbonate of soda pneumatic conveying systems find widespread application across various industries, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, the system is used to transport bicarbonate of soda for baking and other food preparation processes, ensuring consistent quality and hygiene. In pharmaceutical applications, the system helps maintain the purity of the material, as it minimizes exposure to contaminants and prevents cross-contamination. Similarly, in chemical manufacturing, the system is employed to handle bicarbonate of soda in production lines, contributing to streamlined operations and improved productivity. The versatility of the system allows it to adapt to different production scales and material requirements, making it a valuable asset for businesses seeking reliable material handling solutions.
Advantages of Choosing HeadPowder's Solutions
When selecting a pneumatic conveying system for bicarbonate of soda, businesses benefit from the expertise and experience of HeadPowder. The company's solutions offer several advantages, including enhanced material handling efficiency, reduced operational costs, and improved safety. By leveraging advanced engineering and manufacturing techniques, HeadPowder ensures that its systems are built to withstand the demands of continuous operation, minimizing maintenance requirements and maximizing uptime. Additionally, the company provides comprehensive support services, including installation, commissioning, and after-sales maintenance, ensuring that clients receive the full value of their investment. The use of high-quality materials and components further contributes to the longevity and reliability of the system, providing long-term benefits for businesses.
Conclusion and Contact Information
HeadPowder, based in Shandong, China, continues to be a leader in providing innovative and effective pneumatic conveying solutions for the transportation of bicarbonate of soda. By combining advanced technology with a customer-centric approach, the company ensures that its systems meet the specific needs of each client, delivering superior performance and reliability. For businesses seeking to enhance their material handling processes, HeadPowder offers a comprehensive range of solutions that are tailored to meet industry standards and regulatory requirements. Contact HeadPowder today to learn more about how their pneumatic conveying systems can improve your operations.