

What is a Wheat Flour Bulk Material Conveying System? What Are Its Design Principles?
Wheat flour is a fundamental component in the food and beverage industry, and efficient handling of bulk wheat flour is crucial for maintaining product quality and operational efficiency. A wheat flour bulk material conveying system is a specialized setup designed to transport wheat flour from storage silos or processing units to various destinations within a facility, such as mixing rooms, packaging lines, or storage areas. This system plays a vital role in ensuring smooth workflow and minimizing the risk of contamination or degradation during the material transfer process.
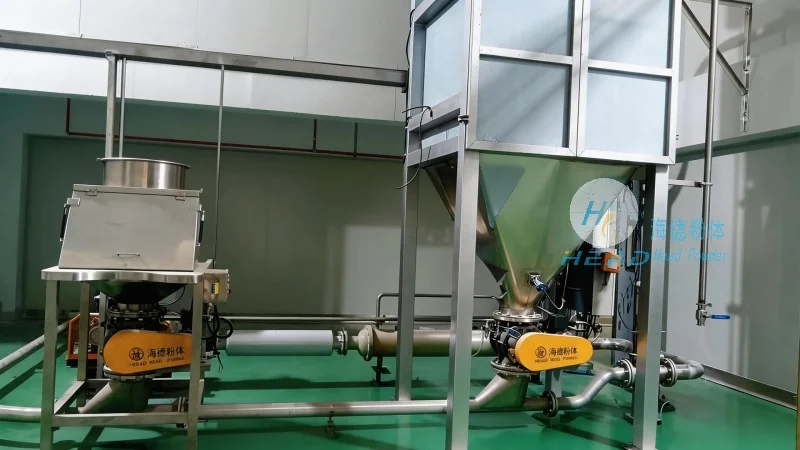
Understanding the Wheat Flour Conveying System
At the core of a wheat flour bulk conveying system is a network of components that work in tandem to move the fine, powdery material. The system typically includes silos or hoppers for storage, conveyors (such as pneumatic or mechanical systems), and control mechanisms to regulate the flow. The choice of conveying method depends on factors like the volume of flour to be moved, the distance between source and destination, and the specific requirements of the processing plant. For instance, pneumatic conveying systems use air to transport flour, while mechanical systems rely on belts or screws.
Design Principles of Wheat Flour Conveying Systems
The design of a wheat flour bulk material conveying system is guided by several key principles to ensure optimal performance and safety. First, the system must be designed to handle the unique properties of wheat flour, which includes its fine particle size, low bulk density, and tendency to create dust. This requires specialized equipment that minimizes particle breakage and prevents dust accumulation, which can lead to health hazards and equipment damage. Second, the system must be hygienic and easy to clean to comply with food safety regulations. Materials used in the construction of the conveying components, such as stainless steel, are common choices due to their resistance to corrosion and ease of sanitation.

Components and Their Functions
A typical wheat flour bulk conveying system consists of several key components, each with a specific function. The storage silo or hopper is where the wheat flour is initially stored, often equipped with a discharge valve to control the flow of material. The conveyor system, which may be pneumatic or mechanical, transports the flour from the storage area to the processing or packaging area. Pneumatic systems use air pressure to move the flour through a pipeline, while mechanical systems use screws or belts to push the material forward. The system also includes control valves and sensors to monitor and regulate the flow rate, ensuring that the flour is delivered at the correct speed and quantity. Additionally, dust collection systems are often integrated to capture any airborne flour particles, maintaining a clean and safe working environment.
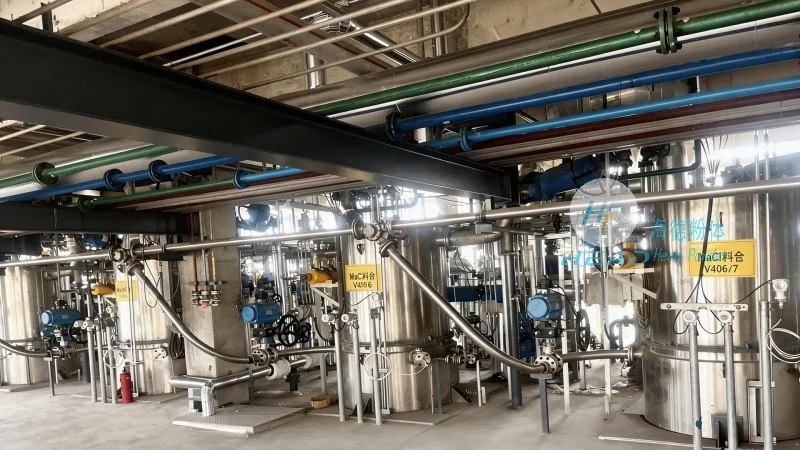
Importance of Proper Design and Maintenance
Proper design and regular maintenance are essential for the long-term efficiency and reliability of a wheat flour bulk conveying system. A well-designed system minimizes the risk of blockages, which can occur due to the fine nature of wheat flour. Regular cleaning and inspection of the conveyor components help prevent the buildup of flour residue, which can affect the system's performance and increase the risk of contamination. The use of high-quality materials and components, such as stainless steel and durable belts, ensures that the system can withstand the demands of continuous operation in a food processing environment. Additionally, the integration of advanced control systems allows for real-time monitoring of the conveying process, enabling operators to quickly identify and address any issues that may arise.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of bulk material handling solutions, including specialized wheat flour conveying systems. With a focus on innovation and customer satisfaction, HeadPowder designs and manufactures systems tailored to the unique needs of the food and beverage industry. The company's expertise lies in understanding the specific challenges of handling fine powders like wheat flour and developing solutions that ensure efficiency, safety, and compliance with industry standards. HeadPowder's systems are built with high-quality materials and advanced technology to deliver reliable performance in demanding environments. The company serves clients across China and beyond, helping them optimize their material handling processes and improve overall operational efficiency.