

Working Principle and Features of Bulk Bag Unloading Pneumatic Conveying Systems
Bulk bag unloading pneumatic conveying systems represent a sophisticated solution for efficient material handling in industrial settings. These systems are engineered to automate the process of transferring bulk materials from flexible containers, commonly known as ton bags, into processing equipment or storage facilities. By integrating pneumatic conveying technology with specialized components, the systems ensure seamless operation, minimize manual labor, and enhance overall operational safety.

System Overview and Application
Bulk bag unloading pneumatic conveying systems are widely utilized across various industries, including chemical processing, food and beverage, pharmaceuticals, and mining. The primary function is to handle large quantities of bulk materials, such as powders, granules, and fine particulates, which are typically stored in ton bags due to their cost-effectiveness and ease of transport. The system's design allows for the safe and controlled transfer of these materials, preventing dust generation and contamination during the unloading process.
Working Principle of the Pneumatic Conveying Process
The operation of a bulk bag unloading pneumatic conveying system is based on the principles of pneumatic transport, which can be categorized as either vacuum or positive pressure systems. In a vacuum system, a vacuum pump creates a negative pressure that draws material from the bulk bag through the discharge valve and into the conveying line. The material is then carried to the receiving point by the moving air stream. Conversely, a positive pressure system employs a blower to generate positive pressure, pushing material from the bulk bag into the conveying line. Both methods ensure that the material remains enclosed within the system, minimizing exposure to external contaminants and maintaining product integrity.
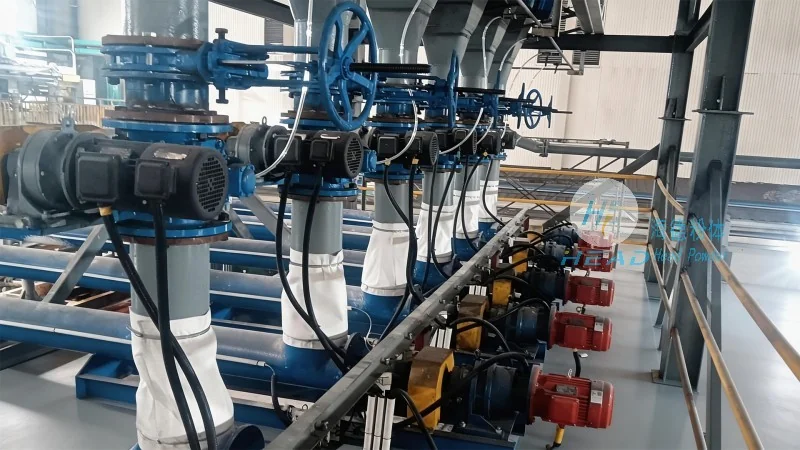
Key components in the system include the bulk bag itself, which is constructed from durable fabric and designed to hold substantial quantities of material. The discharge valve, often a bottom discharge type, enables controlled material release into the conveying line. The pneumatic conveying unit typically comprises a hopper, a filter, and a vacuum pump or blower. The hopper serves as a collection point for the material, while the filter removes any airborne particles to maintain air quality. The vacuum pump or blower provides the necessary air flow to transport the material through the system.
Key Features and Advantages
One of the most significant advantages of bulk bag unloading pneumatic conveying systems is their high operational efficiency. By automating the unloading process, these systems reduce the time required to empty ton bags, thereby increasing production throughput and reducing labor costs. The pneumatic conveying method also minimizes material degradation and segregation, as the material is transported in a closed system, preserving its physical and chemical properties.

Another notable feature is the system's adaptability to diverse material types and processing requirements. The design allows for customization, such as adjusting the conveying velocity or the size of the conveying line, to accommodate different bulk densities and flow characteristics. This flexibility ensures that the system can be optimized for specific applications, whether in pharmaceutical manufacturing, where precise dosing is critical, or in chemical processing, where handling corrosive or abrasive materials is required.
Reliability is a critical feature of these systems. Advanced control systems and durable components ensure consistent performance over extended periods. Regular maintenance, including filter cleaning and component inspection, is recommended to maintain optimal operation. The use of high-quality materials, such as stainless steel for the conveying line and hopper, enhances longevity and resistance to corrosion, especially when handling harsh or abrasive materials.
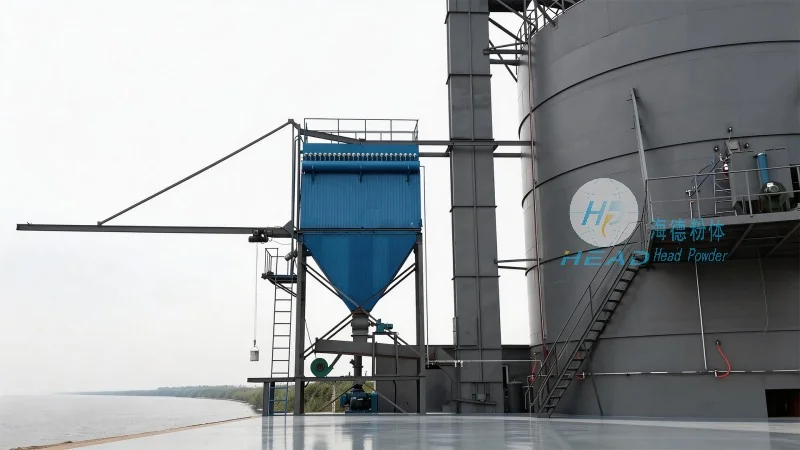
Company Background: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a leading manufacturer of bulk bag unloading pneumatic conveying systems. With decades of experience in the material handling industry, the company specializes in providing customized solutions tailored to the unique needs of its clients. The company's commitment to quality and innovation has established it as a trusted partner in the industry, delivering reliable and efficient systems that meet international standards.
HeadPowder Engineering Co., Ltd. leverages advanced engineering and manufacturing capabilities to design and produce systems that combine performance, durability, and cost-effectiveness. The company's products are widely used in various sectors, including chemical processing, food and beverage, and pharmaceutical manufacturing, where precise and safe material handling is essential. By adhering to rigorous quality control processes, HeadPowder ensures that each system meets the highest standards of performance and safety, providing long-term value to its customers.