

Principle and Working Scene Characteristics of Boron Nitride Material Handling Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced material handling solutions, including sophisticated systems for transporting boron nitride (BN) materials. This article delves into the fundamental principles behind these systems and explores the key characteristics of their operational environments.
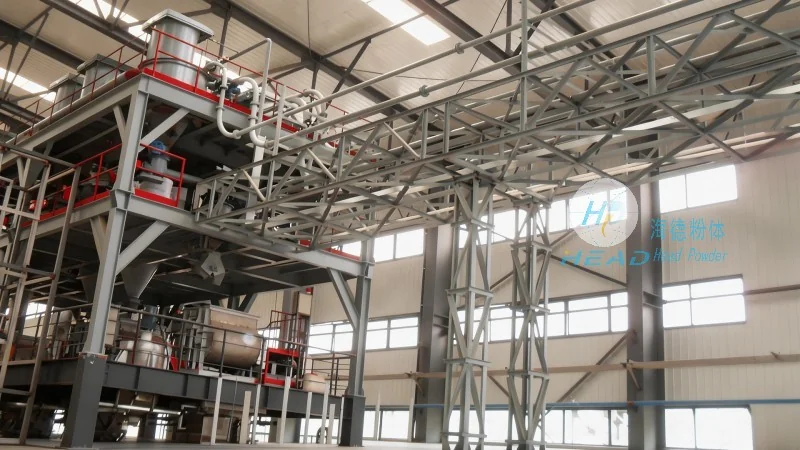
Introduction to Boron Nitride Material Handling Systems
Boron nitride, known for its exceptional thermal stability, chemical inertness, and lubricating properties, is widely used in high-tech industries such as semiconductor manufacturing, aerospace, and advanced ceramics. The efficient and reliable transportation of BN materials is critical to maintaining product quality and operational efficiency in these sectors. HeadPowder's material handling systems are engineered to meet the stringent demands of handling this unique material, ensuring safe and effective movement from storage to processing units.

The Core Principles of BN Material Handling
The operation of boron nitride material handling systems is grounded in several key principles that ensure optimal performance and material integrity. Firstly, the systems are designed to minimize friction and wear, which is crucial given BN's delicate nature and the high temperatures often encountered during processing. This is achieved through specialized components like low-friction bearings, smooth-surfaced conveyors, and precision-engineered transfer mechanisms. Secondly, the systems prioritize contamination control, as even minute impurities can compromise the purity of BN, which is essential for applications like semiconductor wafer manufacturing. Advanced filtration and sealed systems are integral to maintaining a clean environment. Thirdly, energy efficiency is a critical design consideration, with systems incorporating variable speed drives and optimized flow paths to reduce operational costs while minimizing environmental impact.
Key Working Scene Characteristics
The operational environments where these material handling systems are deployed exhibit distinct characteristics that influence system design and performance. In semiconductor fabs, for instance, the systems operate in ultra-clean rooms with strict particle and contamination limits. The design must include features like HEPA filtration, sealed enclosures, and non-porous materials to prevent particulate release. In contrast, in aerospace or high-temperature processing facilities, the systems may need to handle BN at elevated temperatures, requiring heat-resistant components and thermal management solutions. The systems are also adapted to different scales, from small-scale laboratory setups to large-scale industrial production lines, with modular designs allowing for flexibility in system configuration. Additionally, the systems are integrated with automation and control systems to enable precise material tracking and real-time monitoring, enhancing overall process control and safety.

Applications and Industry Impact
Boron nitride material handling systems from HeadPowder play a vital role in enabling the efficient production of high-value BN-based products. By ensuring the reliable and contamination-free transport of BN materials, these systems contribute to improved product yield, reduced downtime, and enhanced safety in various industrial applications. The systems are particularly valuable in sectors where material purity and process consistency are non-negotiable, such as advanced electronics manufacturing and aerospace component fabrication. As industries continue to demand higher performance from BN materials, the role of sophisticated material handling systems becomes increasingly critical, and HeadPowder's solutions are positioned to meet these evolving needs.