

Principle and Working Scene Characteristics of Coal Ash Material Handling Equipment
For industrial operations involving coal ash, efficient material handling is crucial. The coal ash material handling equipment developed by Shandong HeadPowder Engineering Co., Ltd. is designed to meet the demands of various industrial applications, ensuring reliable and efficient transport of coal ash materials. This article explores the underlying principles of this equipment and highlights its key working scene characteristics.

Company Overview
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and supply of advanced material handling solutions. With a strong focus on innovation and customer needs, the company provides tailored equipment for diverse industrial sectors, including power plants, cement factories, and waste management facilities. The company's expertise lies in optimizing material transport processes, enhancing operational efficiency, and ensuring compliance with industry standards.
The Principle of Coal Ash Material Handling Equipment
The coal ash material handling equipment operates based on mechanical principles that facilitate the movement of bulk materials like coal ash. The core components typically include conveyor systems, feeding mechanisms, and control units. The equipment is engineered to handle the specific physical properties of coal ash, such as its density, moisture content, and particle size distribution. By integrating advanced engineering techniques, the system ensures consistent and controlled material flow, minimizing downtime and maximizing throughput. The design emphasizes durability and low maintenance, making it suitable for continuous industrial operations.

Working Scene Characteristics
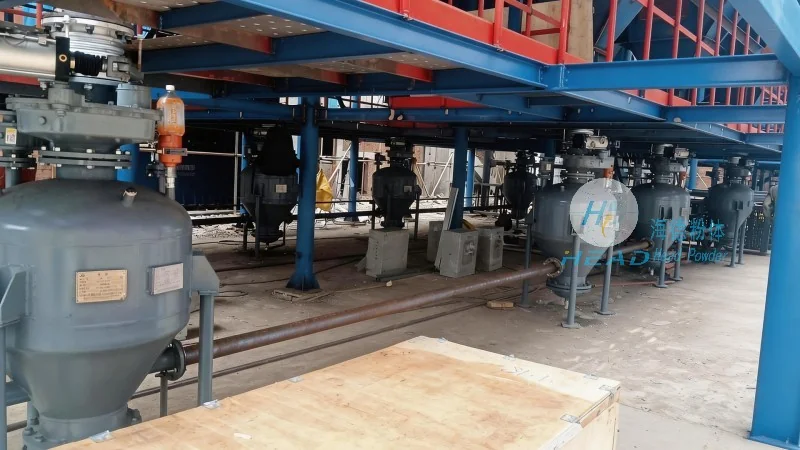
The working scene characteristics of coal ash material handling equipment are tailored to the specific requirements of industrial environments. In power plants, for instance, the equipment is used to transport coal ash from combustion processes to storage or disposal sites. The system must handle high volumes of material while maintaining safety standards and environmental regulations. In cement factories, the equipment assists in the transport of coal ash as a raw material for cement production, contributing to the overall production efficiency. The equipment's adaptability allows it to operate in various working conditions, including indoor and outdoor settings, with minimal operational adjustments. The working scene characteristics also include considerations for space constraints, as industrial facilities often have limited room for material handling equipment. The design incorporates compact structures and flexible configurations to fit into existing layouts without compromising performance.

Key Features and Advantages
Shandong HeadPowder Engineering Co., Ltd.'s coal ash material handling equipment offers several advantages that enhance operational performance. The equipment is equipped with advanced control systems that allow for real-time monitoring and adjustment of material flow. This feature ensures optimal operation under varying load conditions and helps prevent equipment overload. The use of high-quality materials in construction ensures durability and resistance to corrosion, which is critical for handling coal ash that may contain acidic components. The equipment also features energy-efficient designs, reducing operational costs and environmental impact. Additionally, the company provides customized solutions to meet the unique needs of each client, ensuring that the equipment is perfectly suited to the specific working environment and material characteristics.
Application Scenarios
The coal ash material handling equipment is widely used in various industrial applications. In power generation, the equipment is essential for the efficient transport of coal ash from boilers to storage facilities, where it can be used as a fuel or disposed of safely. In the cement industry, coal ash is often used as a supplementary cementitious material, and the handling equipment ensures that it is transported to the production line without loss or contamination. Waste management facilities also utilize this equipment to handle coal ash generated from municipal solid waste incineration, contributing to the recycling and proper disposal of waste materials. The equipment's versatility makes it suitable for a range of applications, from small-scale operations to large-scale industrial plants.
Conclusion
Coal ash material handling equipment from Shandong HeadPowder Engineering Co., Ltd. represents a reliable solution for industrial material transport needs. By understanding the underlying principles and working scene characteristics, industries can select the most appropriate equipment to enhance their operational efficiency and meet regulatory requirements. The company's commitment to quality and innovation ensures that its equipment continues to meet the evolving demands of the industrial sector, providing long-term value and performance.