

[Nitrile Rubber Pneumatic Conveying Equipment: An Overview of Its Structure and Working Principles]
For industries dealing with nitrile rubber, efficient material handling is crucial. The nitrile rubber pneumatic conveying equipment offered by Shandong HeadPowder Engineering Co., Ltd. is a specialized solution designed to meet the demands of modern material transport. This equipment is engineered to handle nitrile rubber with precision, ensuring minimal material degradation and optimal performance in various industrial applications.

Key Features of Nitrile Rubber Pneumatic Conveying Systems
The nitrile rubber pneumatic conveying equipment from HeadPowder is built with durability and efficiency in mind. These systems are equipped with high-quality components that can withstand the unique properties of nitrile rubber, such as its elasticity and resistance to oils and chemicals. The design incorporates advanced materials and engineering techniques to ensure long-term reliability and low maintenance costs. Each component, from the hopper to the discharge valve, is carefully selected to maintain the integrity of the nitrile rubber during transport.
Working Principle of Pneumatic Conveying for Nitrile Rubber
The operation of nitrile rubber pneumatic conveying equipment relies on the principle of air movement to transport materials. The system typically consists of a hopper where the nitrile rubber is stored, a blower or air compressor that generates the necessary air pressure, and a pipeline network that directs the material to its destination. As air is introduced into the hopper, it creates a low-pressure zone that draws the nitrile rubber particles into the pipeline. The air then carries the rubber through the system, depositing it at the discharge point. This process is continuous and can be adjusted to handle varying volumes and particle sizes of nitrile rubber.
Structural Components and Their Functions
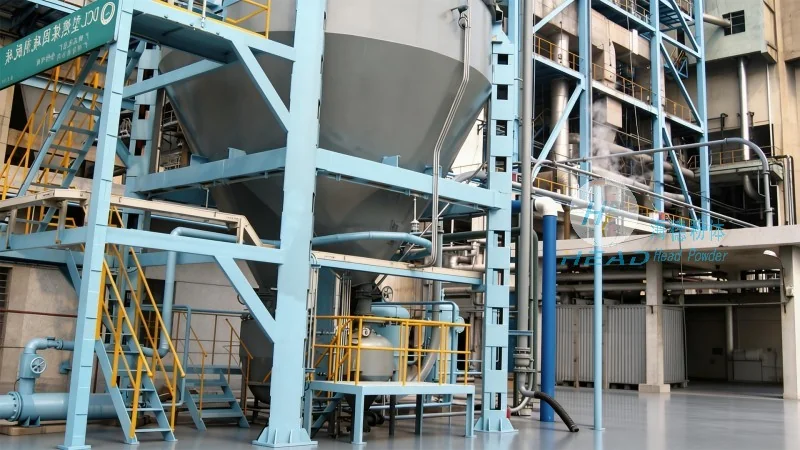
The nitrile rubber pneumatic conveying equipment includes several key structural components, each playing a vital role in the overall operation. The hopper is the primary storage unit, designed with a sloped bottom to facilitate material flow. It is often lined with wear-resistant materials to prevent damage from the abrasive nature of nitrile rubber. The blower or air compressor provides the necessary air pressure, with options available for both positive and negative pressure systems depending on the application. The pipeline system is made of corrosion-resistant materials, such as stainless steel or special plastics, to ensure compatibility with nitrile rubber and prevent contamination. The discharge valve at the end of the pipeline controls the release of the material, allowing for precise control over the discharge rate.
Benefits of Using Nitrile Rubber Pneumatic Conveying Equipment
Implementing nitrile rubber pneumatic conveying equipment offers numerous advantages for industrial operations. Firstly, it eliminates the need for manual handling, reducing the risk of workplace injuries and improving safety standards. Secondly, the equipment minimizes material loss and contamination, ensuring that the nitrile rubber remains in pristine condition throughout the transport process. Thirdly, the automated system increases operational efficiency, allowing for higher throughput and reduced downtime. Additionally, the equipment is designed to be energy-efficient, helping to lower operational costs and reduce the environmental impact of material handling.

Applications in Industrial Settings
The nitrile rubber pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is widely used in various industrial sectors. In the automotive industry, it is used to transport nitrile rubber components for seals and gaskets. In the chemical industry, it helps in the handling of nitrile rubber used in protective gloves and other products. The equipment is also utilized in the manufacturing of rubber products, where consistent material flow is essential for quality control. Regardless of the application, the equipment ensures that nitrile rubber is handled with care, maintaining its properties and extending its shelf life.
Customization and Technical Support
HeadPowder understands that each industrial application has unique requirements. Therefore, the nitrile rubber pneumatic conveying equipment is customizable to meet specific needs. Customers can choose from different hopper sizes, pipeline configurations, and air pressure systems to suit their production processes. The company also provides comprehensive technical support, including installation guidance, maintenance services, and troubleshooting assistance. This ensures that clients can maximize the performance of their equipment and achieve optimal results in their operations.